With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications involving the transport of dry pebbles, various pneumatic conveying structures are employed to ensure efficient and reliable material handling. These systems are designed to handle different particle sizes, flow rates, and operational conditions, catering to the specific needs of mining, construction, and other industries. Understanding the main types of dry pebble pneumatic conveying structures is crucial for selecting the most suitable system for a given application.
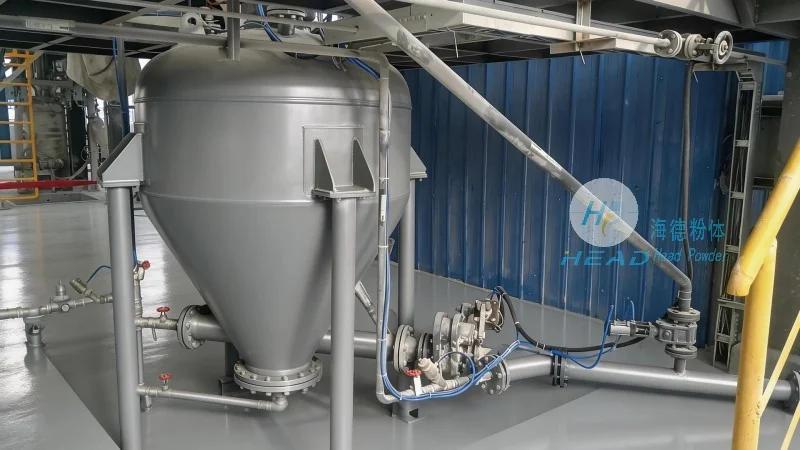
Dry pebble pneumatic conveying systems utilize air or gas to transport solid materials, such as pebbles, over long distances without the need for mechanical components like belts or buckets. These systems are widely used in the mining and construction sectors due to their ability to handle abrasive materials and operate in harsh environments. The efficiency and reliability of these systems depend largely on the design and configuration of the conveying structure, which must be tailored to the characteristics of the pebbles being transported.
All dry pebble pneumatic conveying systems consist of several core components, including a material feed hopper, a conveying line (usually a pipe), a blower or compressor to generate airflow, and a discharge outlet. The material feed hopper is responsible for storing and feeding the pebbles into the system, while the conveying line transports the material from the feed point to the discharge point. The blower or compressor provides the necessary pressure and airflow to move the material through the system, and the discharge outlet collects the material at the end of the conveying line. Each component plays a critical role in the overall performance of the system, and their design must be optimized for the specific application.
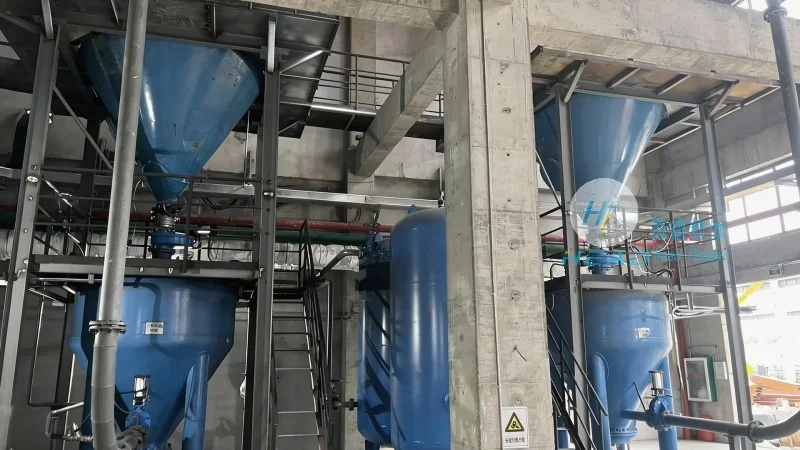
There are several main types of dry pebble pneumatic conveying structures, each with its own advantages and applications. The most common types include the positive pressure system, the negative pressure system, the mixed pressure system, and the dilute phase system. Each type is characterized by the pressure differential used to move the material and the particle size range it can handle.
The positive pressure system is the most widely used type of dry pebble pneumatic conveying structure. In this system, air is forced under pressure into the conveying line, carrying the pebbles from the feed hopper to the discharge outlet. The pressure in the system is maintained above atmospheric pressure, which helps to prevent dust and other contaminants from entering the system. This system is suitable for transporting pebbles over long distances and at high flow rates, and it is commonly used in mining and construction applications. The positive pressure system is also known for its ability to handle abrasive materials and operate in harsh environments.
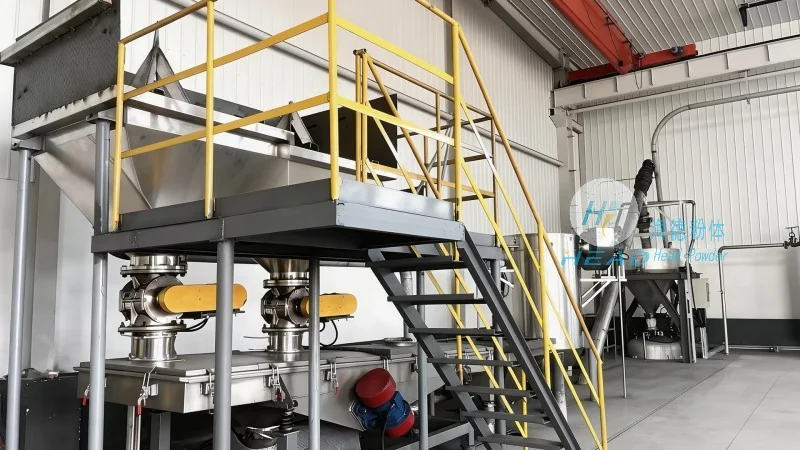
The negative pressure system is a less common type of dry pebble pneumatic conveying structure, but it is still used in some applications. In this system, air is drawn out of the conveying line, creating a vacuum that pulls the pebbles from the feed hopper to the discharge outlet. The pressure in the system is maintained below atmospheric pressure, which helps to prevent dust and other contaminants from entering the system. This system is suitable for transporting pebbles over short distances and at low flow rates, and it is commonly used in laboratory or pilot plant applications. The negative pressure system is also known for its ability to handle fine particles and operate in clean environments.
The mixed pressure system is a combination of the positive and negative pressure systems, and it is used in applications where both high and low flow rates are required. In this system, the conveying line is divided into two sections, with a positive pressure section at the feed end and a negative pressure section at the discharge end. The positive pressure section is used to transport the pebbles from the feed hopper to the middle of the line, while the negative pressure section is used to transport the pebbles from the middle of the line to the discharge outlet. This system is suitable for transporting pebbles over long distances and at varying flow rates, and it is commonly used in large-scale industrial applications.
The dilute phase system is a type of pneumatic conveying system that uses a low concentration of material in the conveying line. In this system, the pebbles are mixed with a large amount of air, which helps to reduce the pressure drop and increase the flow rate. The dilute phase system is suitable for transporting pebbles over long distances and at high flow rates, and it is commonly used in mining and construction applications. The dilute phase system is also known for its ability to handle abrasive materials and operate in harsh environments.
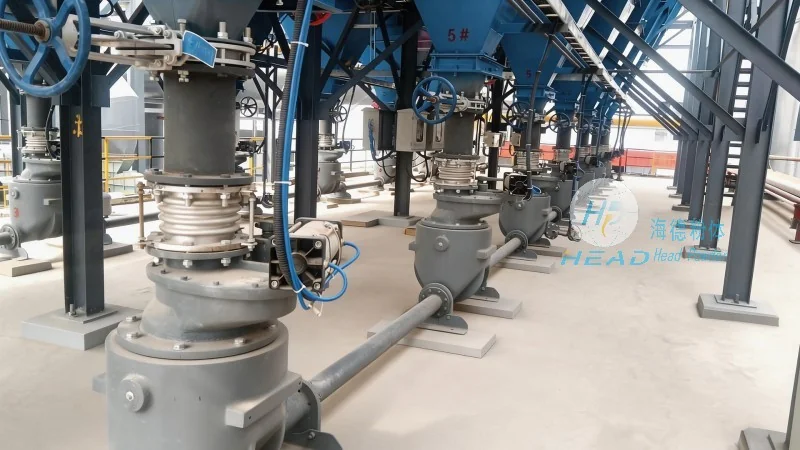
The selection of the appropriate dry pebble pneumatic conveying structure depends on several factors, including the particle size of the pebbles, the flow rate required, the distance to be covered, and the operating environment. The positive pressure system is generally preferred for long-distance and high-flow applications, while the negative pressure system is preferred for short-distance and low-flow applications. The mixed pressure system is suitable for applications where both high and low flow rates are required, and the dilute phase system is suitable for applications where high flow rates and long distances are required. The choice of system should be based on a thorough analysis of the specific application requirements and the characteristics of the pebbles being transported.
Dry pebble pneumatic conveying structures are essential for efficient material handling in the mining and construction industries. The main types of these structures, including the positive pressure, negative pressure, mixed pressure, and dilute phase systems, each offer unique advantages and are suitable for different applications. The selection of the appropriate system depends on the specific requirements of the application, including the particle size, flow rate, distance, and operating environment. By understanding the characteristics of each system and the factors that influence their performance, industrial operators can select the most suitable dry pebble pneumatic conveying structure for their needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top