With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Sulfate potash is a vital mineral resource widely used in agriculture as a fertilizer, playing a crucial role in enhancing soil fertility and crop yields. The efficient handling and transportation of this bulk powder material are essential for industrial operations, and pneumatic conveying systems have emerged as a reliable solution to address these challenges. This article explores the principles and applications of sulfate potash pneumatic conveying, highlighting how air flow can be utilized to move these fine particles with high efficiency and minimal loss.
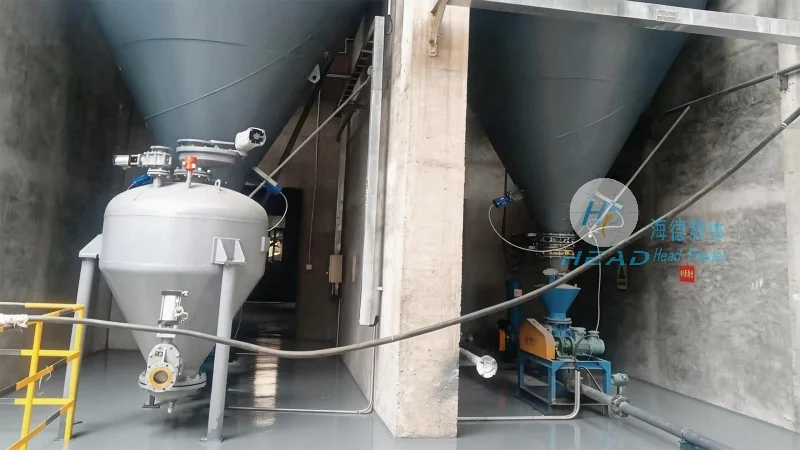
Traditional methods of transporting sulfate potash, such as belt conveyors or bucket elevators, often face limitations when dealing with fine powders. These systems may suffer from material degradation, dust emissions, and operational inefficiencies. In contrast, pneumatic conveying offers several advantages that make it an ideal choice for handling sulfate potash. First, it provides a closed system, reducing dust pollution and ensuring environmental compliance. Second, it allows for gentle material handling, minimizing product degradation and preserving the quality of the fertilizer. Third, pneumatic conveying systems can be designed for both dilute and dense phase operations, offering flexibility in handling different flow rates and particle sizes. For sulfate potash, which often consists of fine particles, dense phase conveying is particularly effective as it reduces the risk of blockages and ensures consistent flow.
Pneumatic conveying systems operate by using air to transport bulk materials through a pipeline. The process typically involves a blower or compressor that generates the necessary air pressure to move the material. In the case of sulfate potash, the system can be configured as either a positive or negative pressure system. Positive pressure systems push the air and material through the pipeline, while negative pressure systems draw the material into the system using a vacuum. The choice between these systems depends on factors such as the distance to be covered, the volume of material to be transported, and the need to minimize dust emissions. For sulfate potash, a positive pressure system is often preferred as it provides better control over the flow and reduces the risk of material buildup in the pipeline.
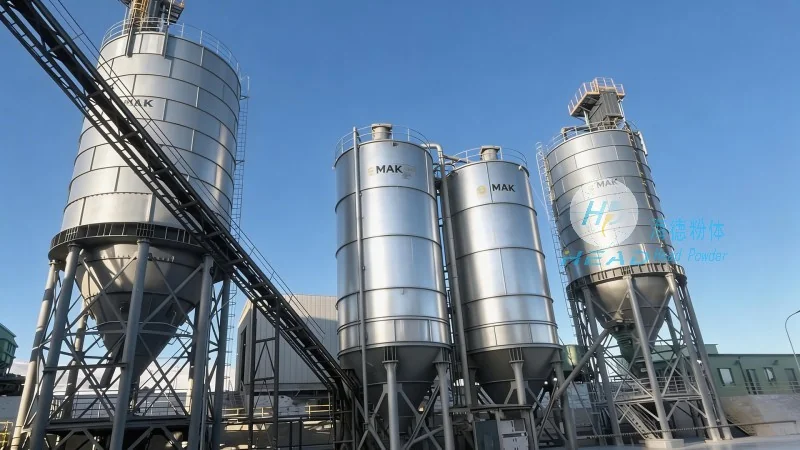
A typical pneumatic conveying system for sulfate potash includes several key components that work together to ensure efficient operation. These components include a material feeder, which is responsible for feeding the powder into the system at a controlled rate. The feeder can be a rotary valve, a screw feeder, or a vibratory feeder, depending on the specific requirements of the application. Next, the system includes a blower or compressor, which provides the air pressure needed to move the material. The blower is usually located at the inlet of the system to ensure that the air and material are mixed properly. The pipeline itself is made of materials that are resistant to corrosion and abrasion, such as stainless steel or plastic, to withstand the harsh conditions of sulfate potash. At the discharge end, a receiver or silo is used to collect the material, and a dust collector may be included to capture any particles that escape the system. The system also includes control valves and sensors to monitor the flow rate and pressure, ensuring that the operation is stable and efficient.
Sulfate potash pneumatic conveying systems are used in a variety of applications across the agricultural and industrial sectors. In fertilizer production, these systems are used to transport the raw material from storage silos to processing facilities, ensuring a continuous and efficient supply of material. In the manufacturing of fertilizer blends, pneumatic conveying is used to mix different components, such as sulfate potash, nitrogen, and phosphorus, into a uniform blend. The systems are also used in the distribution of fertilizer to farms, where they can be used to load trucks or spreaders with the material. Additionally, pneumatic conveying is used in research and development facilities to transport small quantities of sulfate potash for testing and analysis.
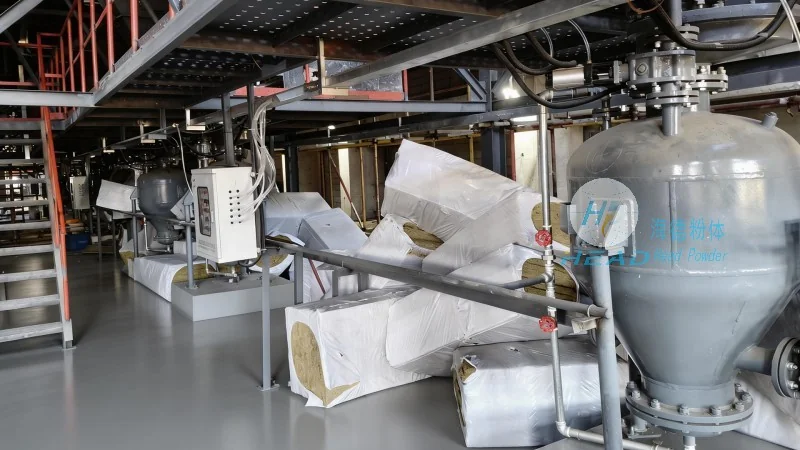
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of pneumatic conveying systems for sulfate potash and other bulk materials. With years of experience in the industry, HeadPowder has developed a range of customized solutions that meet the specific needs of its clients. The company's expertise lies in designing and manufacturing high-quality pneumatic conveying systems that are efficient, reliable, and cost-effective. HeadPowder's systems are designed to handle the unique challenges of sulfate potash, such as its fine particle size and high moisture content. The company uses advanced technology and materials to ensure that its systems are durable and long-lasting, providing years of trouble-free operation. HeadPowder's commitment to quality and customer satisfaction has made it a trusted partner for many companies in the agricultural and industrial sectors.
HeadPowder understands that each client's needs are unique, and therefore, the company offers customized pneumatic conveying solutions tailored to specific applications. The company works closely with its clients to understand their requirements and develop a system that meets their needs. This includes considering factors such as the distance to be covered, the volume of material to be transported, the required flow rate, and the need for environmental compliance. HeadPowder also invests in research and development to stay at the forefront of technological advancements in pneumatic conveying. The company continuously improves its systems to enhance efficiency, reduce energy consumption, and minimize maintenance costs. By combining its expertise with innovative technology, HeadPowder provides its clients with the best possible solutions for their sulfate potash conveying needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top