With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Sulfuric magnesium, a versatile chemical compound widely used in agriculture, food processing, and industrial manufacturing, presents unique handling challenges due to its physical properties. As a fine powder, it often suffers from issues such as poor flowability, electrostatic buildup, and dust generation during transfer. Traditional mechanical conveying methods, such as screw conveyors or belt conveyors, may not always provide the required efficiency or cleanliness for high-value chemical materials. To address these complexities, industries are increasingly turning to advanced pneumatic conveying technologies. This technology ensures a sealed transfer process, minimizing product loss and contamination while maximizing throughput. For businesses seeking a reliable method to manage bulk powder logistics, understanding the capabilities of a specialized provider is essential.
When selecting a partner for chemical material handling, it is crucial to choose a provider with deep technical expertise and a proven track record. The selection process involves evaluating the manufacturer's ability to design systems that integrate seamlessly into existing production lines. A professional approach considers the specific characteristics of the material, the distance of transfer, and the environmental conditions of the facility. By prioritizing these factors, companies can ensure a smooth transition from raw material storage to final processing or packaging stages.
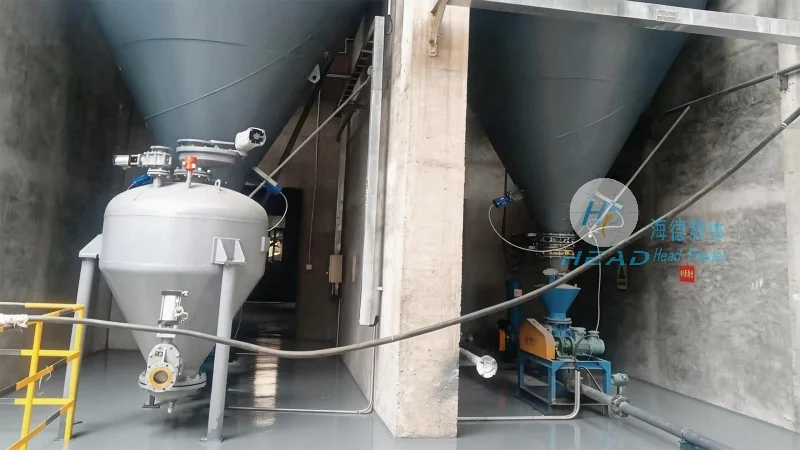
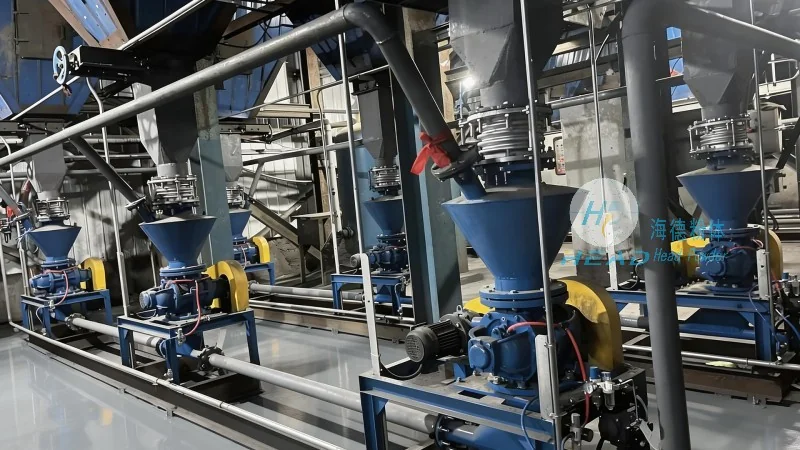
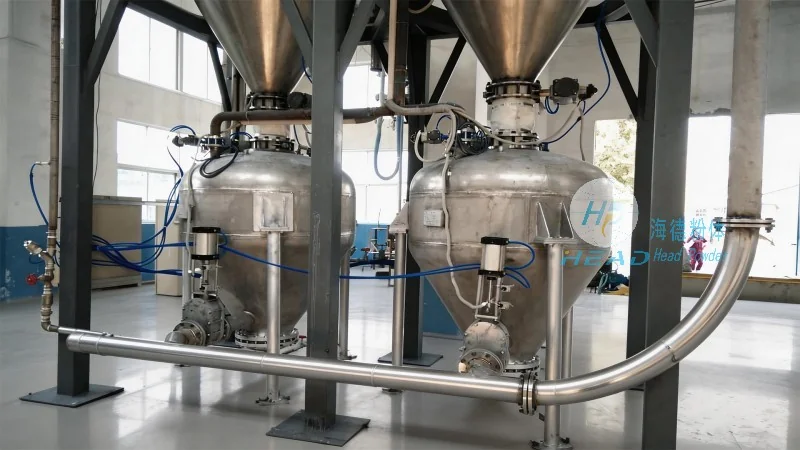
Headpowder stands out as a premier provider in the field, recognized as a dedicated Sulfuric Magnesium Pneumatic Conveying Manufacturer. Our engineering team possesses extensive knowledge regarding the rheology and flow dynamics of chemical powders. We understand that sulfuric magnesium is not just a commodity but a critical input for many production processes, and its integrity must be preserved during transit. As a manufacturer, we focus on the fabrication of high-quality components, including airlocks, pumps, and piping systems, all designed to withstand the corrosive and abrasive nature of industrial chemicals.
Our manufacturing facility is equipped with state-of-the-art machinery that allows for precise fabrication and rigorous quality control testing. Every piece of equipment leaving our factory undergoes a series of stress tests to ensure durability and performance consistency. By controlling the manufacturing process from start to finish, we guarantee that our clients receive equipment that meets the highest industry standards. This commitment to quality makes us a preferred partner for companies looking to upgrade their material handling infrastructure.
Every industrial facility has unique spatial constraints and operational requirements. A "one-size-fits-all" approach rarely works in chemical engineering. Therefore, we specialize in providing a customized Sulfuric Magnesium Pneumatic Conveying Solution tailored to the specific needs of our clients. Our process begins with a comprehensive site survey and material analysis. We evaluate the layout of the plant, the volume of material to be moved, and the destination points to design a system that optimizes energy efficiency and operational safety.
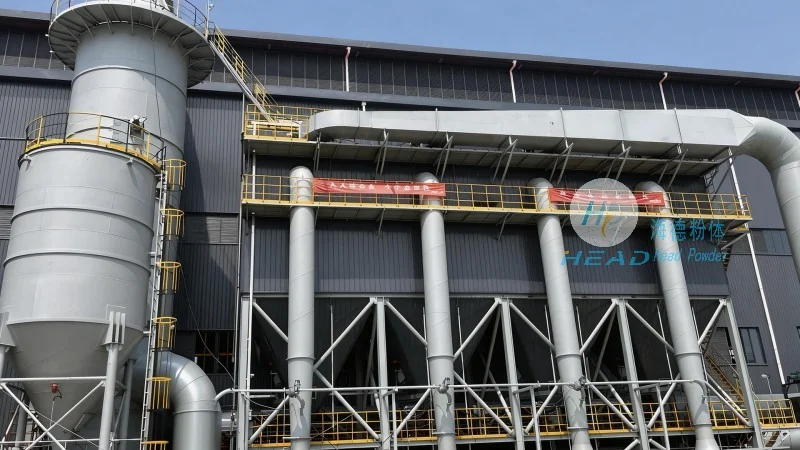
Our customization capabilities extend to various system configurations, whether the requirement is a vacuum-based system for suction of material from multiple hoppers or a pressure-based system for pushing material through long distances. We can also design systems that incorporate dust collection units and explosion-proof features to meet stringent safety regulations. By collaborating closely with the client during the design phase, we ensure that the final solution is not only technically superior but also economically viable, reducing long-term operational costs.
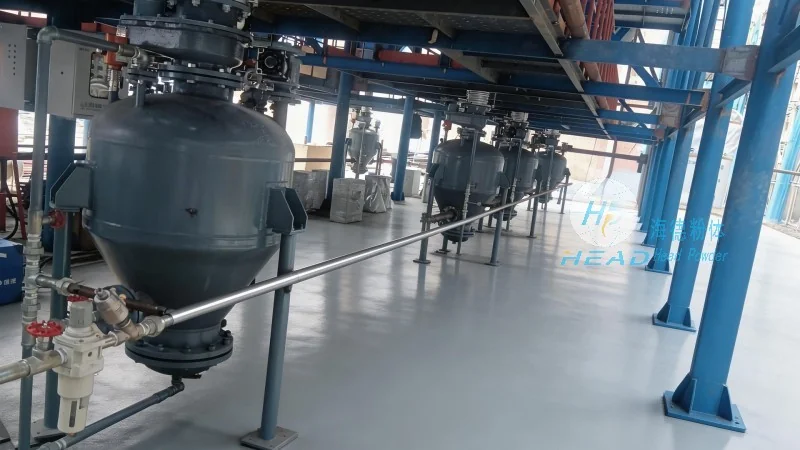
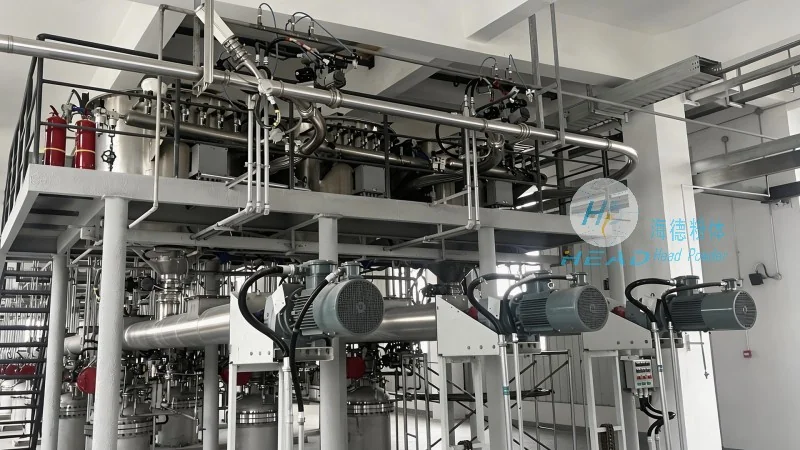
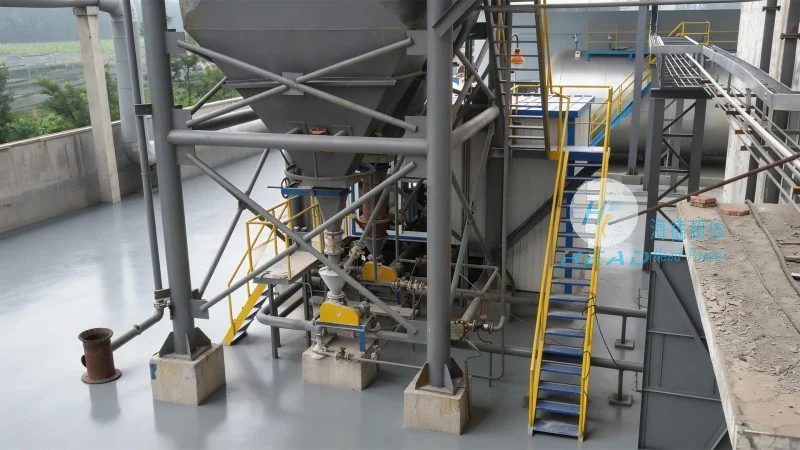
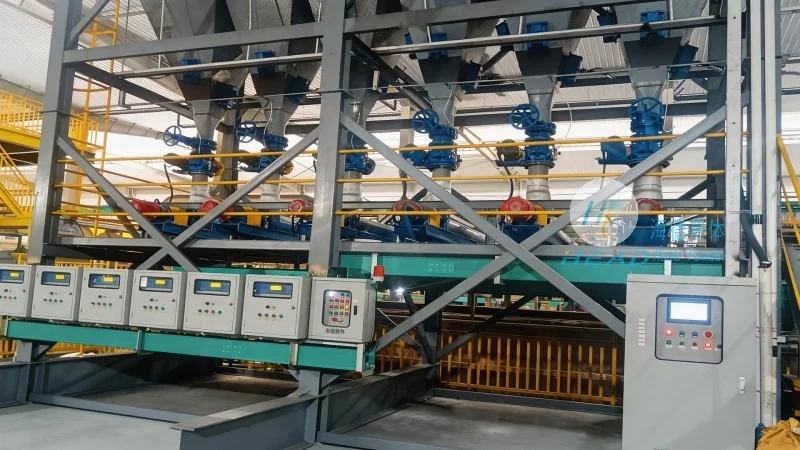
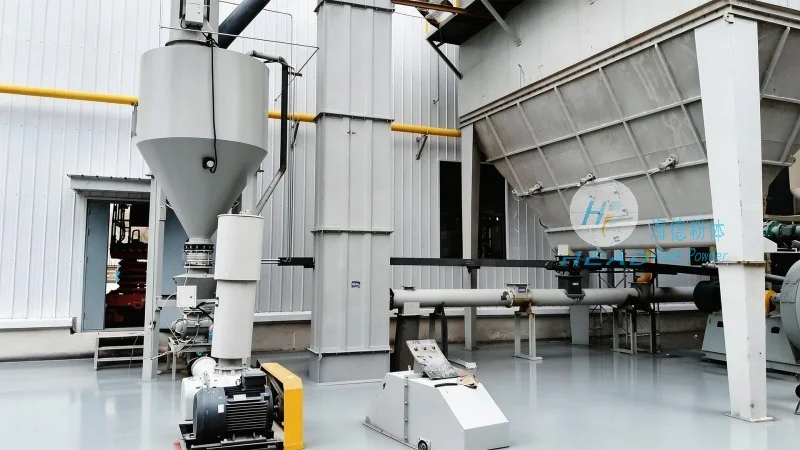
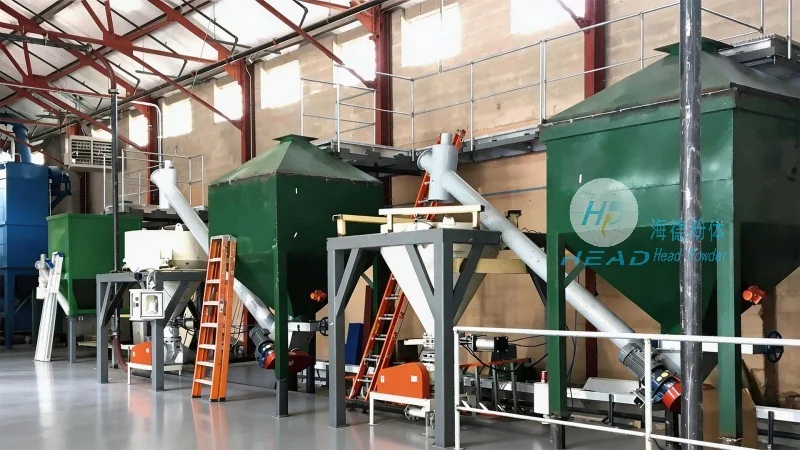
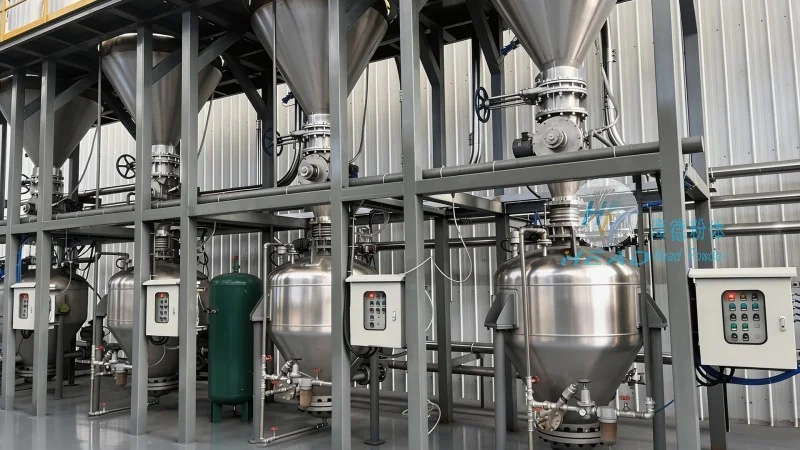
A complete Sulfuric Magnesium Conveying System encompasses more than just the conveying pipe; it is an integrated ecosystem of mechanical and electrical components working in harmony. Headpowder designs and delivers turnkey systems that cover the entire material handling workflow. This includes the design of receiving hoppers, surge bins, and discharge points, ensuring a continuous and uninterrupted flow of material.
The core of our system is the pneumatic conveying mechanism, which utilizes air pressure or vacuum to transport the powder through a closed pipeline network. This closed-loop system is instrumental in preventing environmental pollution, as it eliminates dust emissions and contains the material within the pipeline. Furthermore, our systems are designed for easy maintenance, with accessible components that allow for quick cleaning and servicing. This reliability minimizes downtime, ensuring that production schedules remain unaffected. Whether for short-distance transfers within a factory or long-distance vertical or horizontal transport, our systems deliver consistent performance.
The technology employed in our systems offers numerous technical advantages that set us apart from competitors. One of the primary benefits is the ability to handle difficult-flowing materials. Sulfuric magnesium can sometimes clump or bridge in hoppers; our systems utilize specialized feeding mechanisms to ensure a steady, consistent feed rate into the conveying line. Additionally, we address the issue of electrostatic discharge, which is common with fine powders, by incorporating grounding and anti-static materials into our designs.
Energy efficiency is another cornerstone of our engineering philosophy. We utilize variable frequency drives and optimized air-to-material ratios to reduce power consumption without compromising conveying speed. The materials used for the piping and components are selected based on the chemical compatibility of sulfuric magnesium, ensuring that the system does not degrade over time due to corrosion or wear. These technical nuances demonstrate our commitment to providing a robust and efficient solution for complex material handling tasks.
The versatility of our systems allows them to be deployed across a wide range of scenarios. In the agricultural sector, sulfuric magnesium is used as a soil amendment, and our conveyors facilitate the efficient loading of fertilizers into storage silos or packaging lines. In the food and pharmaceutical industries, where hygiene is paramount, our closed systems prevent cross-contamination, meeting the strict purity standards required for these sectors. For industrial applications, such as the production of fire retardants or detergents, our systems provide the necessary volume and consistency to support large-scale manufacturing.
Shandong Headpowder Engineering Co., Ltd. is the entity behind these advanced solutions. Headquartered in Shandong, China, our company has established itself as a leader in the engineering and manufacturing of pneumatic conveying equipment. We are committed to innovation and customer satisfaction, continuously refining our technologies to meet the evolving demands of the global market. Our team of engineers and technicians is dedicated to providing exceptional service, from the initial consultation to after-sales support.
For those interested in optimizing their material handling processes or seeking a reliable partner for sulfuric magnesium transport, we encourage you to reach out. Our team is ready to discuss your specific requirements and provide expert guidance. You may contact our project manager, Mr. Zhang, for detailed consultations. We look forward to collaborating with you to achieve operational excellence.
Contact: Mr. Zhang (Manager)
WeChat: 15662777102

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top