With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Ammonium bicarbonate, a widely used chemical compound in industrial applications, necessitates specialized handling and transportation methods due to its distinct physical properties. The systems engineered for this purpose are designed to ensure safe, efficient, and reliable movement of the powder, addressing challenges such as dust generation, material flow control, and equipment durability. This overview will explore the key components and operational principles of ammonium bicarbonate powder handling systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in this field.
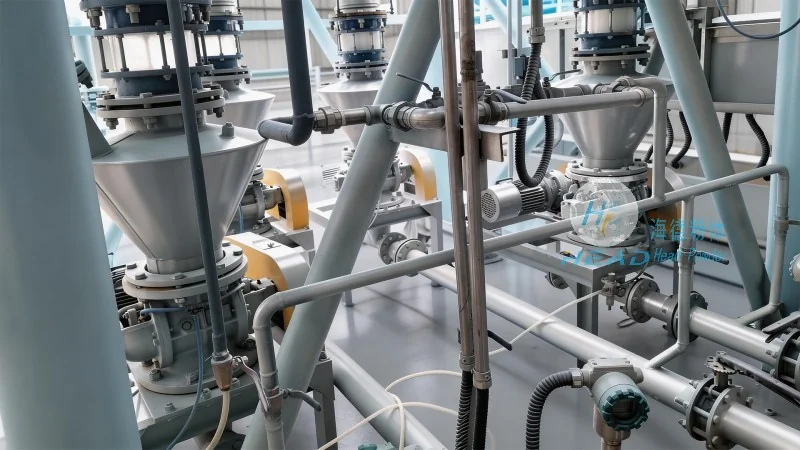
HeadPowder, the professional brand behind advanced powder handling solutions, is dedicated to providing tailored systems for diverse industrial needs. As a leading manufacturer and supplier, HeadPowder Engineering Co., Ltd. specializes in the design, development, and implementation of equipment for handling ammonium bicarbonate and other fine powders. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the chemical processing industry. HeadPowder operates from its headquarters in Shandong, China, where it leverages local expertise and resources to deliver high-performance solutions that meet the stringent requirements of modern industrial applications.
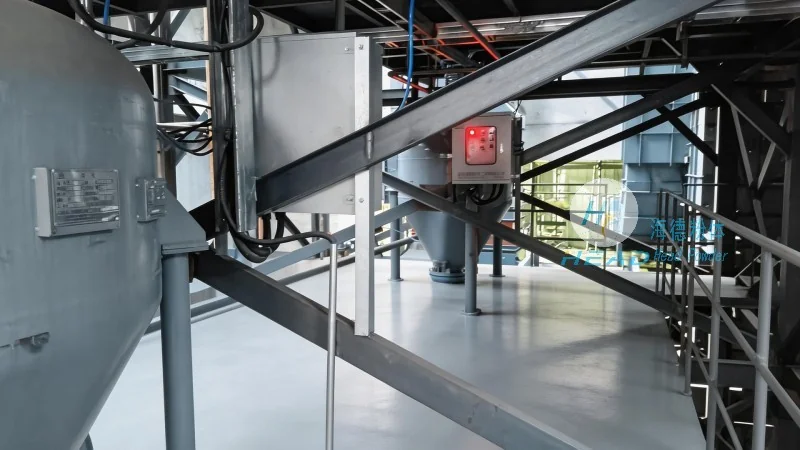
The efficient handling of ammonium bicarbonate powder relies on a combination of specialized equipment and engineering principles. Key components typically include feeders, conveyors, storage silos, and dust control systems. Feeders, such as rotary or vibratory types, are used to regulate the flow of the powder from storage to processing equipment, ensuring consistent and controlled material delivery. Conveyors, including pneumatic or mechanical systems, facilitate the transport of the powder over longer distances or to different processing stages. Storage silos are designed with anti-static and aeration features to maintain the quality and prevent caking or agglomeration of the material. Dust control systems, including filters and ventilation, are essential to mitigate the health and safety risks associated with fine powder handling, ensuring compliance with environmental and occupational health regulations.
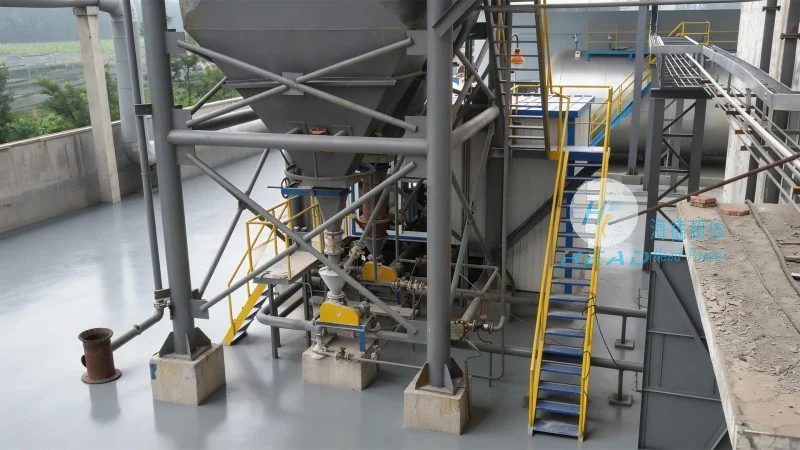
The structural design of ammonium bicarbonate powder handling systems is critical to their performance and longevity. Engineers at HeadPowder consider factors such as material compatibility, corrosion resistance, and operational efficiency when designing these systems. The equipment is constructed from materials that are resistant to the chemical properties of ammonium bicarbonate, preventing degradation and ensuring the integrity of the system over time. Additionally, the design incorporates features to minimize the risk of blockages, such as smooth internal surfaces and appropriate angles for material flow. The integration of aeration and vibration systems helps maintain the flowability of the powder, reducing the likelihood of clogging and ensuring continuous operation. These design principles are tailored to the specific characteristics of ammonium bicarbonate, which is known for its hygroscopic nature and tendency to absorb moisture from the air, making proper moisture control a key aspect of system design.
Operational efficiency and safety are paramount in the handling of ammonium bicarbonate powder. HeadPowder systems are engineered to optimize material throughput while minimizing downtime and maintenance requirements. The use of advanced control systems allows for precise monitoring and adjustment of the powder flow, ensuring that the system operates within optimal parameters. Safety measures are integrated throughout the design, including explosion-proof components, dust extraction systems, and emergency shutdown protocols. These measures help protect personnel and equipment from the hazards associated with fine powder handling, such as dust explosions and respiratory health risks. Regular maintenance and inspection procedures are also part of the operational plan, ensuring that the system remains in good working condition and meets all regulatory standards. By prioritizing both efficiency and safety, HeadPowder systems provide reliable performance for industrial applications that require the consistent and safe handling of ammonium bicarbonate.
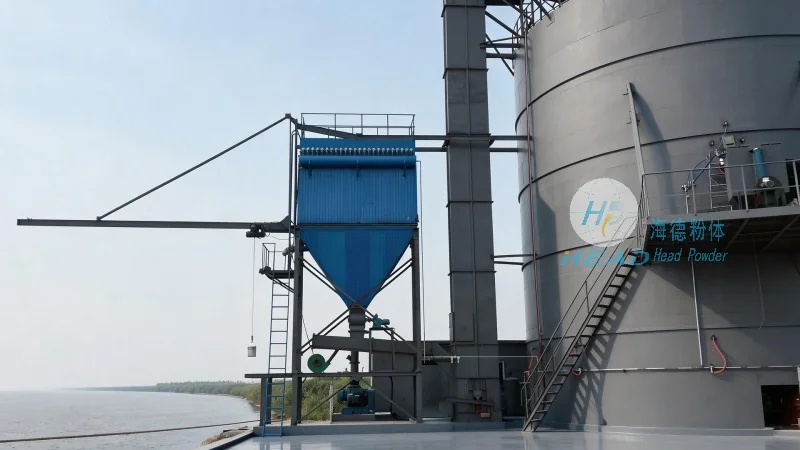
Ammonium bicarbonate powder handling systems, as exemplified by the solutions offered by Shandong HeadPowder Engineering Co., Ltd., represent a critical component of modern industrial processes. These systems are designed to address the unique challenges of handling fine, hygroscopic powders, ensuring safe and efficient material movement from storage to processing. The expertise of HeadPowder in engineering and manufacturing tailored solutions has made it a trusted provider in the chemical processing industry. Whether used in food production, pharmaceutical manufacturing, or other applications requiring ammonium bicarbonate, these systems contribute to the overall productivity and safety of industrial operations. HeadPowder's commitment to quality, innovation, and customer satisfaction continues to drive the development of advanced powder handling technologies that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top