With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Camellia seed material handling systems are critical components in the processing and management of oil tea seeds, which are widely used in the production of edible oil and other value-added products. These systems are designed to efficiently transport, store, and process camellia seeds from the initial collection stage to the final processing stage. The effectiveness of such systems directly impacts production efficiency, product quality, and operational costs in oil tea processing facilities.
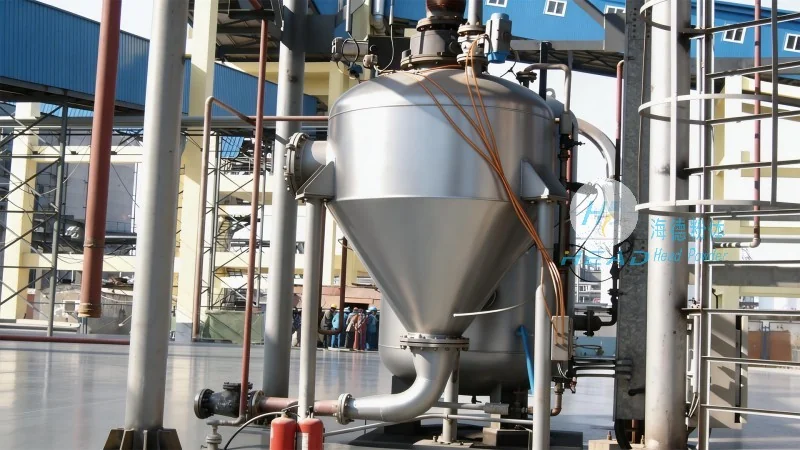
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling solutions. With a strong focus on innovation and customer-centric solutions, HeadPowder has established itself as a trusted partner in the agricultural processing industry. The company’s headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality systems tailored to the unique needs of its clients.
The core principle of camellia seed material handling systems is to ensure the seamless and efficient movement of seeds through various stages of processing. These systems typically incorporate a combination of conveyor belts, elevators, and storage units, each designed to handle the specific characteristics of camellia seeds. The conveyor systems are engineered to handle the seeds’ size, shape, and moisture content, minimizing damage and loss during transport. Elevators are used to lift seeds to higher levels for processing or storage, while storage units provide controlled environments to maintain seed quality. The integration of these components ensures a continuous flow of materials, reducing downtime and increasing overall productivity.
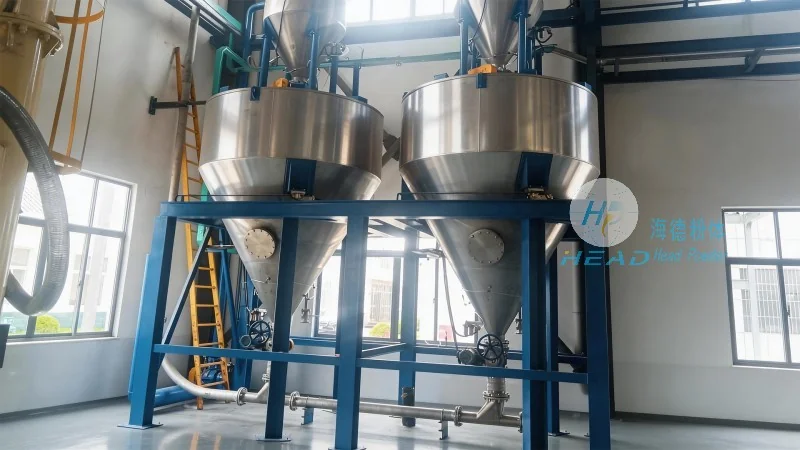
Camellia seed material handling systems consist of several key components, each playing a vital role in the overall operation. The primary components include: conveyor belts, which are responsible for transporting seeds horizontally or at slight inclines; bucket elevators, which lift seeds vertically; storage silos or bins, which store seeds before processing; and feeding mechanisms, which regulate the flow of seeds into processing equipment. Each component is carefully selected and designed to match the specific requirements of the processing facility, ensuring optimal performance and durability.
The operational scenarios for camellia seed material handling systems vary based on the scale and type of processing facility. For small-scale processing plants, the systems may include basic conveyor belts and small storage bins, designed to handle lower volumes of seeds. In contrast, large-scale industrial facilities may employ more complex systems, incorporating multiple conveyor lines, large storage silos, and automated feeding mechanisms. These systems are commonly used in scenarios such as: seed collection from farms, initial cleaning and sorting, storage before processing, and transportation to oil extraction units. The versatility of these systems allows them to adapt to different operational needs, from manual to fully automated processing environments.
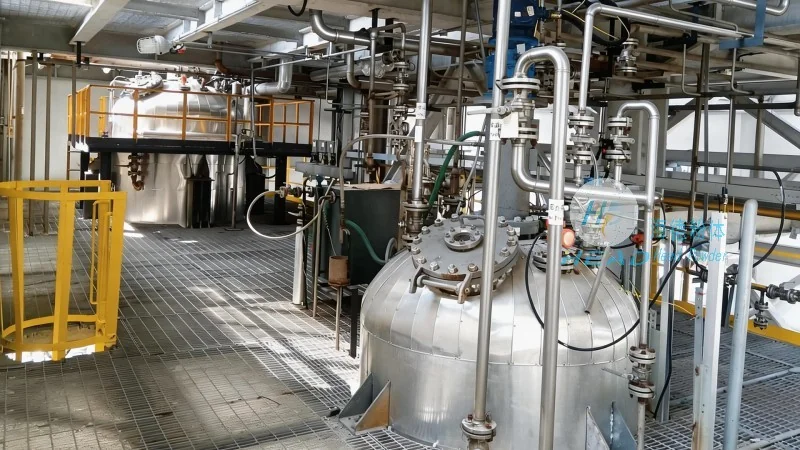
Implementing advanced camellia seed material handling systems offers several significant advantages. Firstly, these systems enhance production efficiency by reducing manual labor and minimizing material handling time. The automated flow of seeds ensures consistent processing speeds, leading to higher output volumes. Secondly, the systems improve product quality by minimizing seed damage and contamination during transport. This is particularly important for oil tea seeds, as damage can affect the final oil yield and quality. Thirdly, the systems reduce operational costs by optimizing energy usage and minimizing waste. By streamlining the material handling process, facilities can achieve better cost control and profitability. Additionally, the use of durable materials and advanced engineering in these systems ensures long-term reliability and low maintenance requirements, providing a solid return on investment for businesses.
HeadPowder specializes in providing customized camellia seed material handling systems that integrate seamlessly with existing processing equipment. The company works closely with clients to understand their specific processing requirements, including seed characteristics, production volumes, and facility layout. Based on this information, HeadPowder designs and manufactures systems that are tailored to meet these needs. The integration of material handling systems with processing equipment, such as oil extractors and separators, ensures a smooth and continuous production line. This customization not only improves operational efficiency but also enhances the overall performance of the processing facility. HeadPowder’s expertise in engineering and material handling allows it to deliver solutions that are both effective and cost-efficient, helping clients achieve their production goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top