With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Wheat starch processing is a critical step in the food and industrial sectors, where efficient material handling is essential for maintaining production efficiency and product quality. The wheat starch material handling system, as designed by Shandong HeadPowder Engineering Co., Ltd. (commonly known as HeadPowder), integrates advanced engineering principles to ensure seamless transportation of starch materials from processing stages to storage or further processing units. This system is engineered to handle the unique characteristics of wheat starch, such as its granular structure and moisture content, while optimizing operational performance and minimizing downtime.
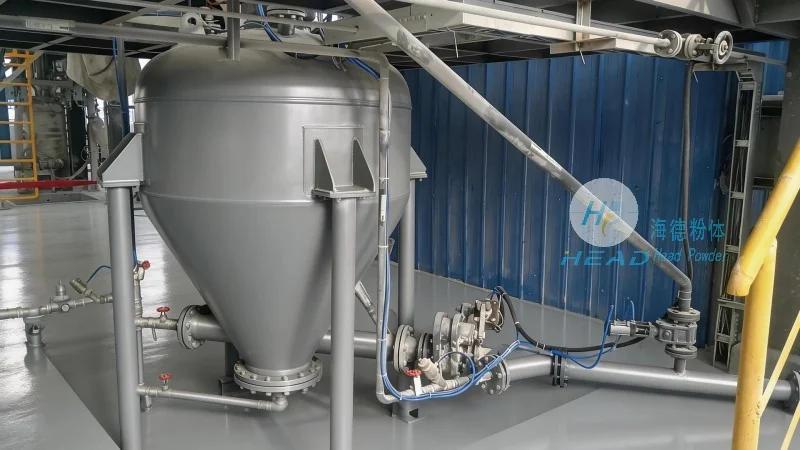
The fundamental principle of the wheat starch material handling system revolves around the use of specialized equipment tailored to the physical properties of starch. Key components include conveyor belts, screw conveyors, and pneumatic transport systems, each selected based on the specific flow characteristics of wheat starch. The system employs a modular design that allows for flexibility in adapting to different production scales and processing requirements. For instance, screw conveyors are ideal for vertical or inclined transport due to their ability to handle bulk materials with minimal segregation, while pneumatic systems offer high-speed, dust-free transport for sensitive starch products. The integration of these components ensures a continuous and controlled flow of material, reducing the risk of clogging or material degradation during transport.
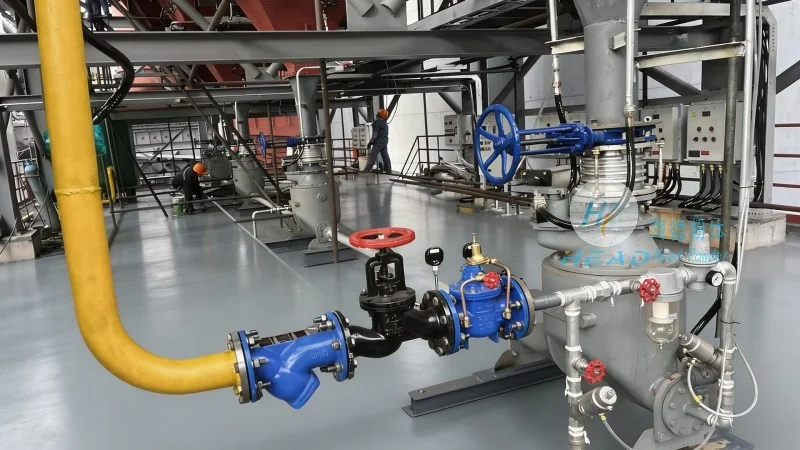
The operational characteristics of the wheat starch material handling system are tailored to diverse industrial applications, including food processing, pharmaceutical manufacturing, and chemical production. In food processing facilities, the system is commonly used to transport starch from grinding and sieving stages to mixing or packaging areas, ensuring a hygienic and efficient workflow. The system's design prioritizes cleanability and compliance with food safety standards, making it suitable for environments where contamination control is paramount. In pharmaceutical applications, the system may be adapted to handle starch as an excipient, with additional features like dust extraction and particle size control to meet stringent regulatory requirements. Industrial chemical plants also utilize this system for transporting starch-based raw materials to reactors or storage tanks, leveraging the system's durability and ability to handle abrasive materials.
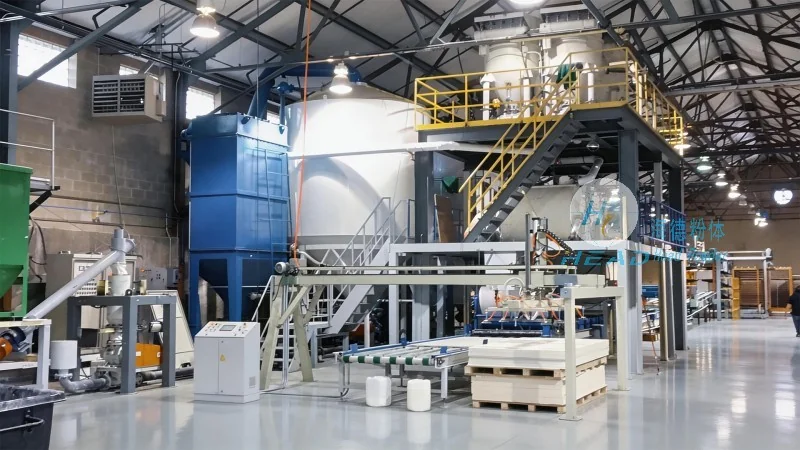
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, has extensive experience in designing and manufacturing systems for the starch industry. With a focus on innovation and customer-centric solutions, HeadPowder combines decades of industry knowledge with advanced engineering capabilities to deliver customized material handling systems. The company's team of engineers and technicians specializes in understanding the unique challenges of starch processing, such as handling fine powders and managing moisture variations, and develops tailored solutions to address these challenges. HeadPowder's commitment to quality is reflected in its adherence to international standards and rigorous testing protocols, ensuring that each system meets the highest performance and safety requirements.
The wheat starch material handling system offers several advantages that enhance operational efficiency and product quality. One key benefit is the reduction in labor costs and manual handling, as automated systems handle the bulk of material transport, minimizing the risk of human error and workplace injuries. The system also improves production throughput by maintaining a consistent flow of materials, which is crucial for meeting high-demand production schedules. Additionally, the system's modular design allows for easy expansion or modification as production needs evolve, providing long-term value to the customer. The use of high-quality materials and advanced manufacturing techniques ensures the system's durability and low maintenance requirements, further contributing to cost savings over its operational life.
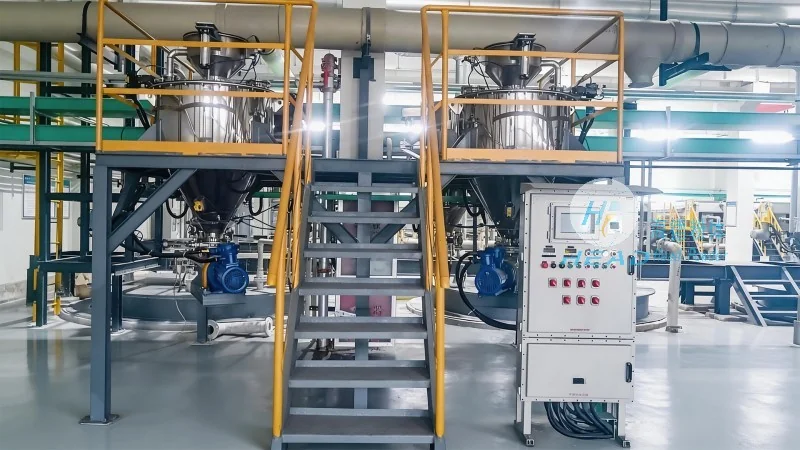
For businesses in the wheat starch industry seeking reliable and efficient material handling solutions, Shandong HeadPowder Engineering Co., Ltd. offers a comprehensive range of systems designed to meet their specific needs. With a focus on innovation, quality, and customer satisfaction, HeadPowder is committed to delivering solutions that enhance productivity and ensure product quality. Based in Shandong, China, HeadPowder leverages its local expertise and global standards to provide systems that are both effective and cost-efficient. For more information or to discuss customized material handling solutions, please contact HeadPowder at their headquarters in Shandong, China.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top