

Principle and Working Scene Characteristics of Quartz Sand Powder Pneumatic Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems for various industrial applications. The company's expertise lies in delivering efficient and reliable solutions for transporting fine powders like quartz sand, ensuring optimal performance and minimal operational disruptions.
Principle of Quartz Sand Powder Pneumatic Conveying Systems
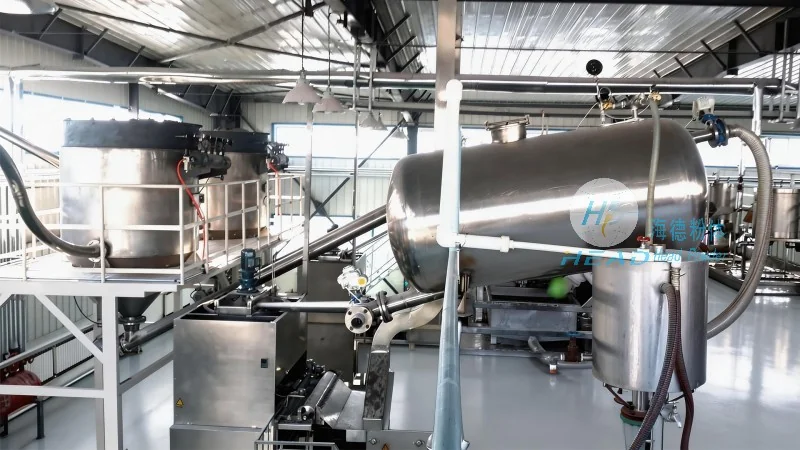
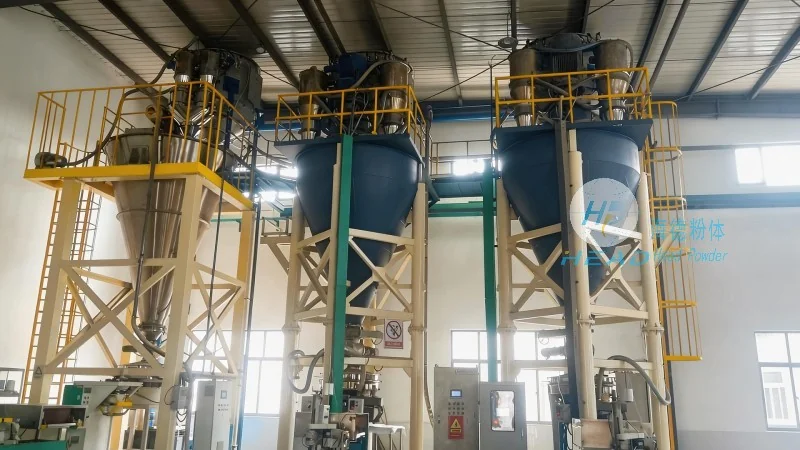
A pneumatic conveying system for quartz sand powder operates on the fundamental principle of using compressed air or other gases to transport bulk materials through a pipeline network. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a conveying line with appropriate ductwork, and a receiver to collect the material at the destination. The process involves creating a pressure differential between the inlet and outlet of the conveying line, which propels the quartz sand particles along the pipeline. This method eliminates the need for mechanical components such as belts or screws, reducing maintenance requirements and enhancing system reliability. The air velocity and pressure are carefully controlled to ensure the material is transported without degradation, clogging, or excessive energy consumption. The system can be designed as either a positive pressure system (where air is blown into the line) or a negative pressure system (where air is drawn out), depending on the specific application requirements and material characteristics.
Working Scene Characteristics of Quartz Sand Powder Pneumatic Conveying Systems
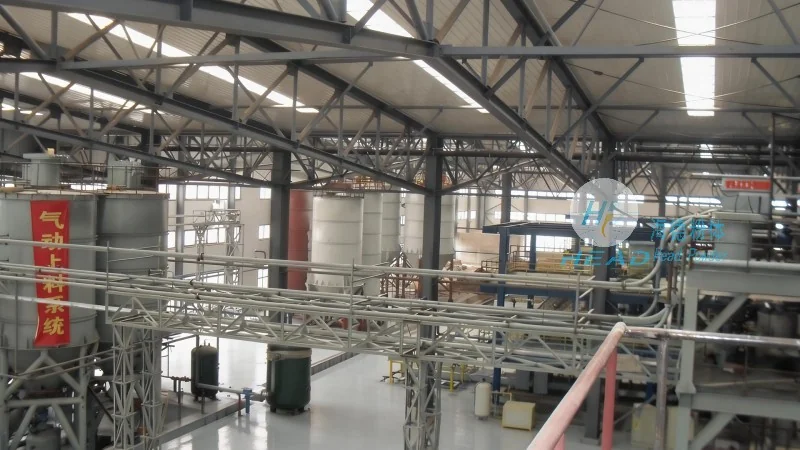
The working scene characteristics of quartz sand powder pneumatic conveying systems are tailored to meet the unique demands of industrial environments. These systems are commonly used in mining, construction, and manufacturing sectors where the efficient handling of fine powders is critical. The key characteristics include high transport efficiency, minimal material degradation, and the ability to handle large volumes of quartz sand over long distances. The systems are designed to operate in both indoor and outdoor settings, with considerations for dust control and environmental compliance. For example, in a mining operation, the system may be used to transport quartz sand from a storage silo to a processing plant, ensuring a continuous and uninterrupted supply of raw material. In a construction site, the system can be employed to move quartz sand from a stockpile to a mixing facility, improving workflow and reducing manual handling risks. The adaptability of these systems allows them to integrate seamlessly with existing production lines, enhancing overall operational productivity. Additionally, the systems are engineered to handle varying particle sizes and moisture content, making them suitable for diverse applications across different industries.
Application and Operational Advantages
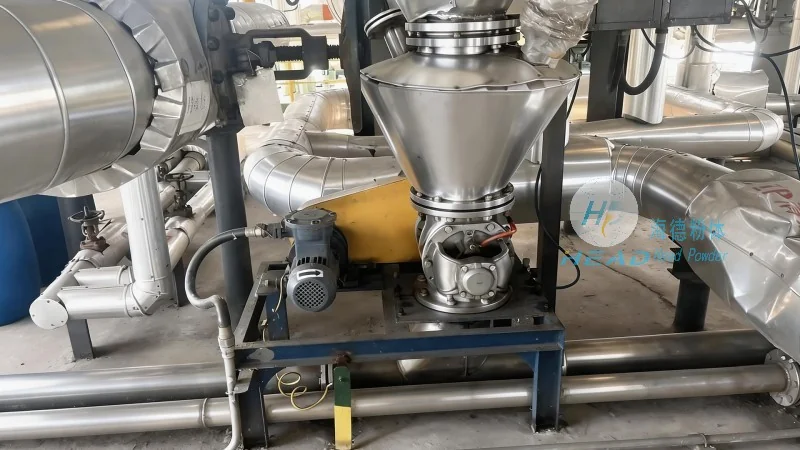
The application of quartz sand powder pneumatic conveying systems offers several operational advantages that enhance industrial productivity and efficiency. By eliminating the need for traditional bulk handling methods, such as bucket elevators or belt conveyors, these systems reduce the risk of material contamination and improve product quality. The enclosed pipeline design minimizes dust emissions, contributing to a safer working environment and compliance with environmental regulations. Furthermore, the systems are capable of transporting materials over significant distances without the need for intermediate storage or transfer points, streamlining the supply chain. In terms of maintenance, the absence of moving parts in the conveying line reduces wear and tear, leading to lower operational costs and longer system lifespans. The flexibility of the system design allows for easy integration with existing infrastructure, making it a cost-effective solution for upgrading or expanding industrial operations. Overall, the quartz sand powder pneumatic conveying systems from HeadPowder provide a reliable, efficient, and sustainable method for handling fine powders in various industrial settings.