With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
White gray material pneumatic conveying equipment operates on the principle of using compressed air or inert gases to transport bulk materials through a pipeline system. This method, known as pneumatic conveying, is particularly effective for handling fine powders like white gray materials, which are often characterized by low density, high dustiness, and potential for caking. The core mechanism involves creating a pressure differential within the pipeline to move the material from the source to the destination. There are two primary types of pneumatic conveying systems: suction (or vacuum) systems and pressure systems. Suction systems use a vacuum at the material source to draw the material into the pipeline, while pressure systems use compressed air to push the material from a storage silo or hopper. For white gray materials, suction systems are commonly employed due to their ability to handle materials from various points and their suitability for long-distance or complex route applications. The process typically begins with the material being fed into a hopper or silo, where it is then drawn into the conveying line by a vacuum created by a rotary airlock or a venturi device. The air and material mixture travels through the pipeline, with the material being separated from the air at the discharge point using a cyclone separator or a filter. This separation ensures that the material is delivered to the target location without contamination or loss of product quality.
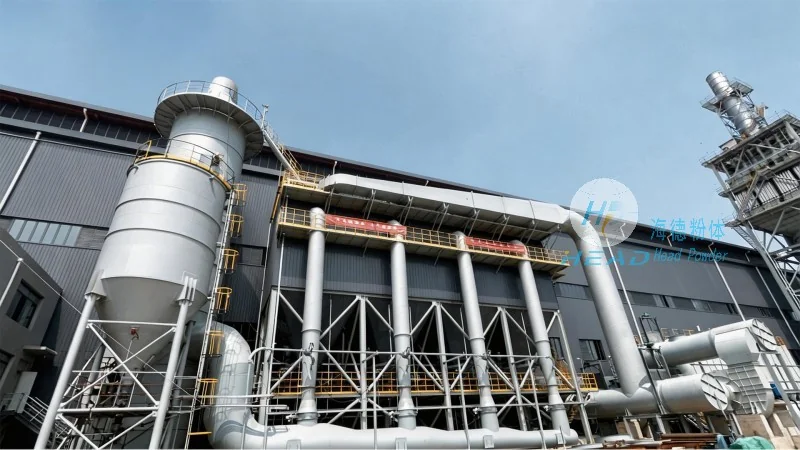
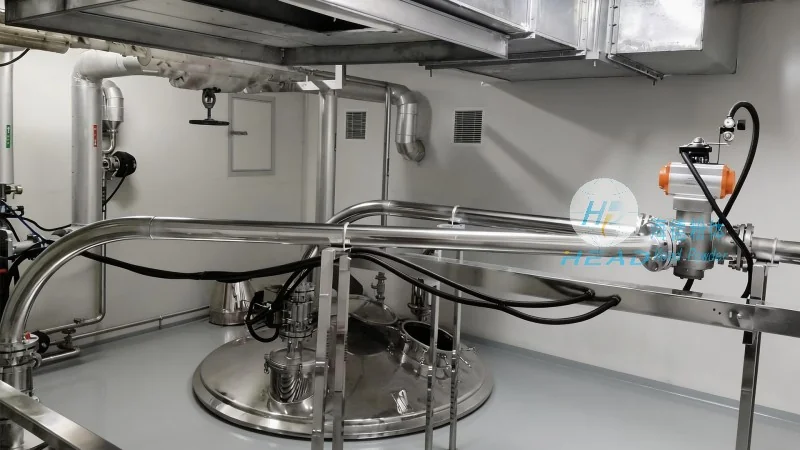
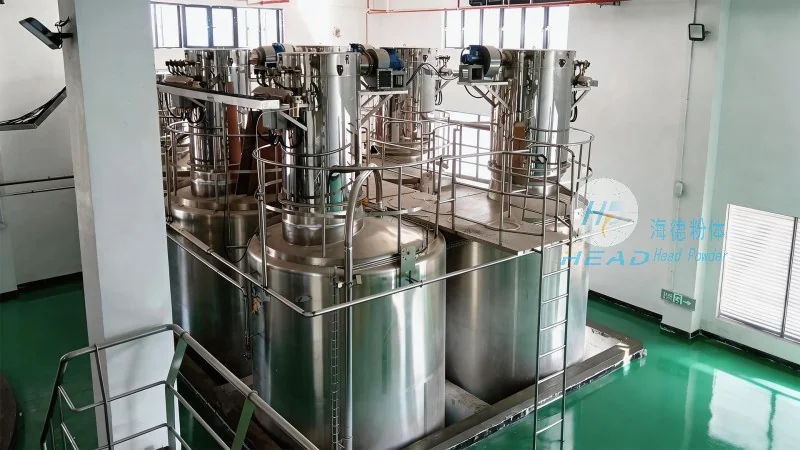
White gray material pneumatic conveying equipment offers several advantages that make it an ideal choice for industrial applications. One of the most significant features is its high efficiency in material transport. Unlike traditional mechanical conveyors, which rely on moving parts like belts or chains, pneumatic systems can transport materials over long distances with minimal energy consumption. This efficiency is particularly beneficial for white gray materials, which are often transported over several hundred meters or more. Another key feature is environmental friendliness. Pneumatic conveying eliminates the need for open chutes or hoppers, reducing dust emissions and minimizing the risk of material contamination. This is crucial for white gray materials, which are often used in food, pharmaceutical, or chemical industries where product purity is paramount. Additionally, the system's flexibility in layout is a major advantage. Pneumatic conveying lines can be easily reconfigured or extended to accommodate changes in production processes or facility expansions. This adaptability reduces the need for costly infrastructure modifications. From a maintenance perspective, pneumatic conveying systems generally have lower maintenance requirements compared to mechanical systems. The absence of moving parts like belts or gears reduces wear and tear, leading to lower operational costs over the system's lifespan. Furthermore, the system's ability to handle abrasive materials without significant wear is another beneficial feature. White gray materials, while fine, can be abrasive, and the smooth interior of the conveying pipeline helps to minimize wear and extend the equipment's service life. The safety aspect of pneumatic conveying is also noteworthy. Unlike mechanical systems that may pose risks from moving parts or entanglement hazards, pneumatic systems operate with enclosed pipelines, reducing the risk of material exposure and improving workplace safety. Overall, these features make white gray material pneumatic conveying equipment a reliable and efficient solution for various industrial applications.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored to the needs of white gray material handling. The company leverages decades of experience in material handling technology to develop customized solutions that address the unique challenges of transporting fine powders. HeadPowder's engineers work closely with clients to understand their specific material characteristics, production volumes, and operational requirements, ensuring that the final system is optimized for performance and efficiency. The company's product line includes a range of components such as rotary airlocks, venturi meters, cyclone separators, and control systems, all designed to work seamlessly together. By integrating these components, HeadPowder provides comprehensive solutions that cover the entire material handling process from source to destination. The company's commitment to quality is evident in its adherence to international standards and rigorous testing protocols. Each system is thoroughly tested before delivery to ensure it meets the client's specifications and operational demands. HeadPowder's expertise in white gray material handling has enabled the company to serve a diverse range of industries, including construction, food processing, and chemical manufacturing. The company's systems are known for their reliability, durability, and ability to handle high volumes of material with minimal downtime. In addition to standard systems, HeadPowder also offers customized solutions for complex applications, such as multi-point material collection or integration with existing production lines. This flexibility allows clients to adapt the system to their specific needs without compromising on performance. The company's focus on customer satisfaction and technical support ensures that clients receive not only a high-quality product but also ongoing assistance to maximize the system's performance. With a strong presence in the domestic market and growing international recognition, Shandong HeadPowder Engineering Co., Ltd. continues to be a leader in the development of advanced pneumatic conveying solutions for white gray materials.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top