With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with bulk materials, efficient and reliable material handling solutions are crucial for maintaining operational efficiency and product quality. Among the various technologies available, bulk bag material pneumatic conveying systems offer a versatile and effective method for transporting powders and granules. This article explores the working principle and key features of such systems, providing insights into how they operate and the advantages they bring to material handling processes.
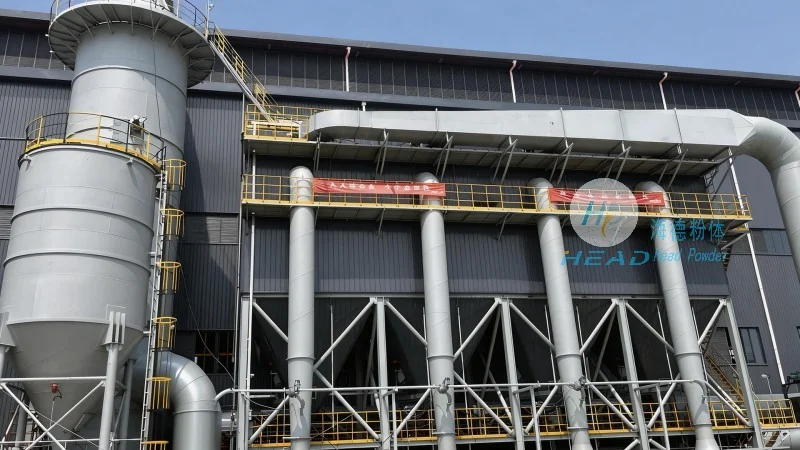
Bulk bag material pneumatic conveying systems are designed to transport bulk materials from a storage container, typically a bulk bag or tote, to a processing or storage location. These systems utilize air pressure or vacuum to move materials through a pipeline network, eliminating the need for mechanical components like belts or screws that may cause contamination or material degradation. The technology is widely used in industries such as pharmaceuticals, food processing, chemicals, and mining, where maintaining product purity and preventing cross-contamination is essential.
The core of a bulk bag material pneumatic conveying system lies in its ability to create a flow of material using air. The process typically begins with the bulk bag being placed on a discharge spout or a hopper equipped with a valve. As air is introduced into the system, it creates a low-pressure zone that draws the material from the bag into the conveying line. The material is then carried through the pipeline by the moving air stream, which can be either positive pressure (where air is forced into the system) or negative pressure (where air is extracted from the system). The system includes components such as a feeder, a filter, and a receiver, which work together to ensure efficient and clean material transfer.
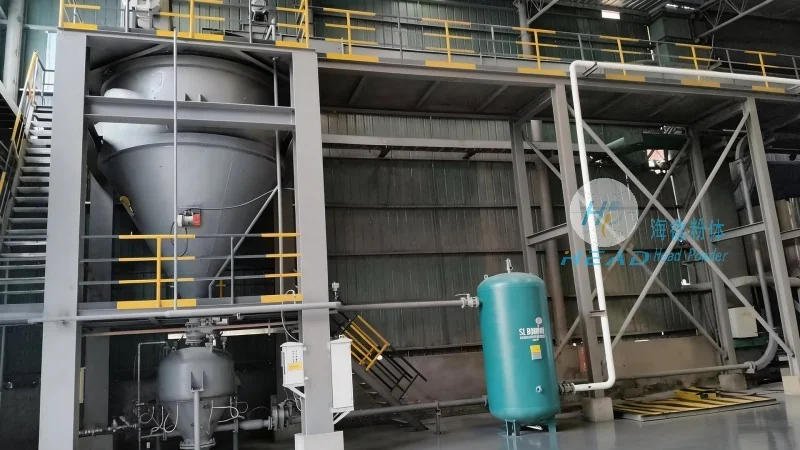
Bulk bag material pneumatic conveying systems offer several advantages that make them a preferred choice for many industries. Firstly, they provide a hygienic and clean method of material transfer, as the system is enclosed and prevents contact with external contaminants. This is particularly important in industries like food and pharmaceuticals where product purity is non-negotiable. Secondly, these systems are flexible and can handle a wide range of materials, from fine powders to coarse granules, without the need for adjustments to the conveying equipment. Thirdly, they are energy-efficient compared to traditional mechanical conveying methods, as they use less power to move materials over short to medium distances. Additionally, the systems are easy to install and maintain, with minimal moving parts that reduce the risk of breakdowns and maintenance costs.
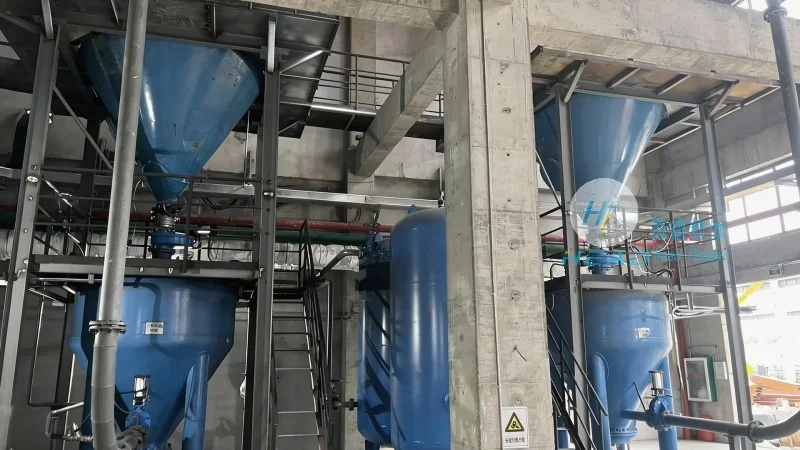
Bulk bag material pneumatic conveying systems are applied in various industries where bulk materials need to be transported efficiently and safely. In the pharmaceutical industry, they are used to transfer active pharmaceutical ingredients (APIs) and excipients with high precision and minimal risk of contamination. In the food industry, they handle ingredients like flour, sugar, and spices, ensuring that the products remain fresh and free from spoilage. The chemical industry uses these systems to transport powders and granules, such as catalysts and reagents, while maintaining the integrity of the materials. In mining and mineral processing, they are employed to move raw materials from storage to processing plants, improving the overall efficiency of the operation.
Bulk bag material pneumatic conveying systems represent a sophisticated solution for material handling, combining efficiency, hygiene, and flexibility. By understanding their working principle and key features, industries can make informed decisions about implementing these systems to enhance their operational capabilities. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality pneumatic conveying systems tailored to the specific needs of various industries. With a focus on innovation and customer satisfaction, HeadPowder offers reliable solutions that meet the stringent requirements of modern material handling applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top