With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Efficient and reliable material handling is a critical aspect of modern fertilizer production, especially when dealing with bulk materials like potash. The potash fertilizer material pneumatic conveying equipment is a specialized system designed to transport these materials with precision and minimal loss. This equipment plays a vital role in the overall workflow of fertilizer manufacturing plants, ensuring smooth and continuous operation from storage to processing and packaging.
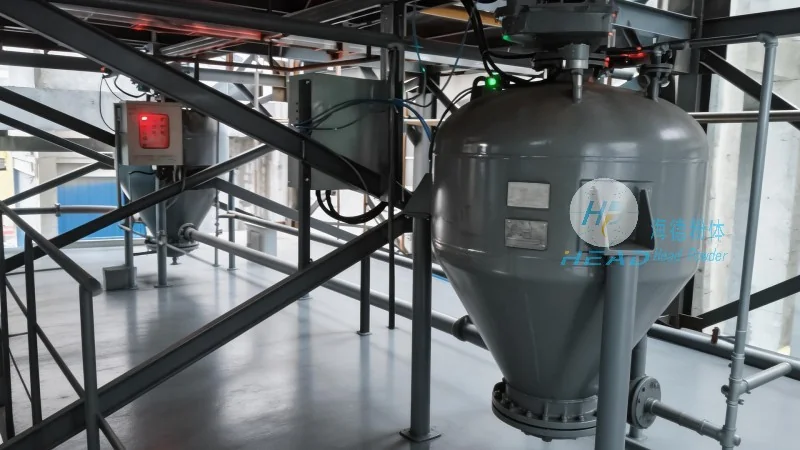
The core of the potash fertilizer material pneumatic conveying system lies in its ability to use air as the conveying medium. This system typically operates under either positive pressure or negative pressure, depending on the specific requirements of the material and the plant layout. In positive pressure systems, a blower or fan generates high-pressure air that propels the potash fertilizer particles through a network of pipes. The air flow carries the material from the source, such as a storage silo or a hopper, to the destination, like a processing unit or a packaging line. The velocity of the air is carefully controlled to ensure that the potash particles are suspended and transported without causing excessive wear on the equipment or the pipes. Negative pressure systems, on the other hand, use a vacuum to draw the material from the source and move it through the system. This approach is often preferred for applications where dust control is a priority, as the sealed system prevents the release of fine particles into the environment.
For potash fertilizer, which is often in the form of granules or fine powder, the design of the pneumatic conveying equipment must account for the material's characteristics. The equipment includes components such as feeders, cyclones, and filters to manage the flow and separation of the material. The feeders, typically screw or rotary types, ensure a consistent and controlled feed rate of the potash into the conveying line. Cyclones are used to separate the material from the air stream, allowing the potash to be deposited at the desired location while the air is either recirculated or discharged. Filters are essential to maintain air quality and prevent the buildup of dust in the system, which is crucial for both operational efficiency and compliance with environmental regulations.
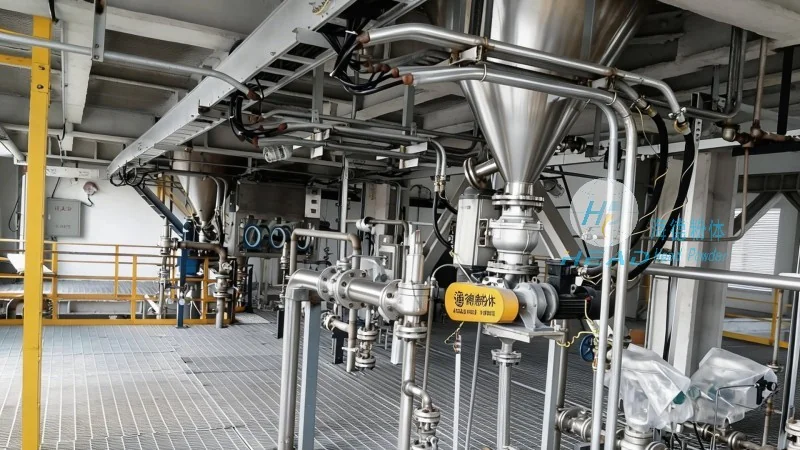
Several distinct features make the potash fertilizer material pneumatic conveying equipment an optimal choice for industrial applications. One of the primary advantages is its ability to handle a wide range of material sizes and densities, from fine powders to larger granules. This versatility allows the system to be adapted to different stages of the fertilizer production process, from raw material intake to final product packaging. The equipment also offers high efficiency in terms of material transport, with minimal material loss and reduced downtime compared to traditional methods like belt conveyors or bucket elevators.
Another significant feature is the system's flexibility in terms of layout and integration. Pneumatic conveying systems can be easily customized to fit the specific space constraints and operational needs of a fertilizer plant. They can be installed in various configurations, including horizontal, vertical, or a combination of both, to accommodate the plant's layout. This adaptability makes the equipment suitable for both new installations and retrofitting existing facilities. Additionally, the equipment is designed with durability and low maintenance in mind, using high-quality materials and components that can withstand the abrasive nature of potash fertilizer particles over extended periods of operation.
The environmental benefits of pneumatic conveying are also a key feature. By operating in a closed system, the equipment minimizes dust emissions and prevents the contamination of the surrounding environment. This is particularly important for potash fertilizer, which can be a source of fine dust that may affect air quality and worker health. The closed system design also helps in maintaining product purity, as the material is not exposed to external contaminants during transport. Furthermore, the energy efficiency of modern pneumatic conveying systems contributes to lower operational costs and reduced environmental impact, making it a sustainable choice for fertilizer manufacturers.
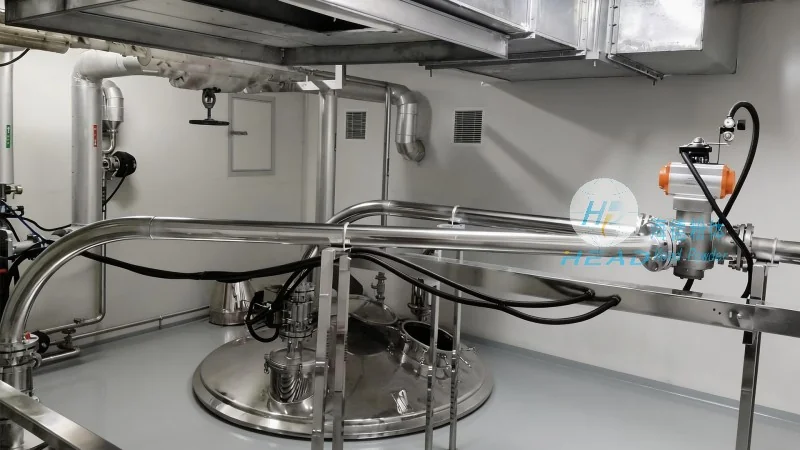
As a leading manufacturer of specialized material handling equipment, Shandong HeadPowder Engineering Co., Ltd. (headpowder) has established itself as a trusted partner in the fertilizer industry. With a strong commitment to innovation and quality, the company designs and manufactures a wide range of pneumatic conveying systems tailored to the unique needs of potash fertilizer production. HeadPowder's expertise lies in understanding the specific challenges of handling bulk materials like potash, and developing solutions that enhance operational efficiency, reduce costs, and ensure compliance with industry standards and regulations.
HeadPowder is headquartered in Shandong, China, where the company leverages its local resources and expertise to provide comprehensive support to clients worldwide. The company's team of engineers and technicians work closely with clients to understand their production requirements and design customized solutions that meet their specific needs. From initial consultation and system design to installation and after-sales service, HeadPowder ensures that every aspect of the project is handled with precision and professionalism. The company's dedication to quality and customer satisfaction has earned it a reputation as a reliable and innovative supplier in the global fertilizer equipment market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top