With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Shandong HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a prominent provider of engineering solutions for the fertilizer industry. This article explores the working principle and key characteristics of a specialized material handling system designed for transporting potassium carbonate fertilizer, a vital nutrient in modern agricultural applications. By examining the technical operations and benefits of this system, stakeholders in the fertilizer sector can gain insights into optimizing their material handling processes and enhancing overall operational efficiency.
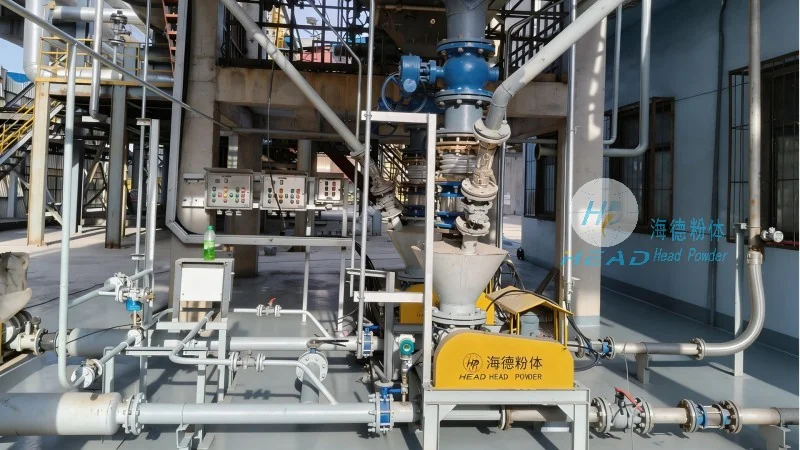
The system functions through a coordinated sequence of mechanical and automated processes to ensure the efficient and safe transport of potassium carbonate fertilizer. Its core components include hoppers, conveyor belts, and control units that work together to move the material from storage to processing or packaging stages. The process begins with the loading of raw potassium carbonate into the hopper, where it is then transferred to the conveyor system. The conveyor belts, constructed with materials resistant to the fertilizer's properties, transport the material through multiple stages, including sorting, blending, and quality inspection. Advanced sensors and control panels monitor the flow rate, ensuring consistent and precise delivery. Safety features such as overload protection and emergency stop mechanisms are integrated to prevent accidents and maintain operational reliability.
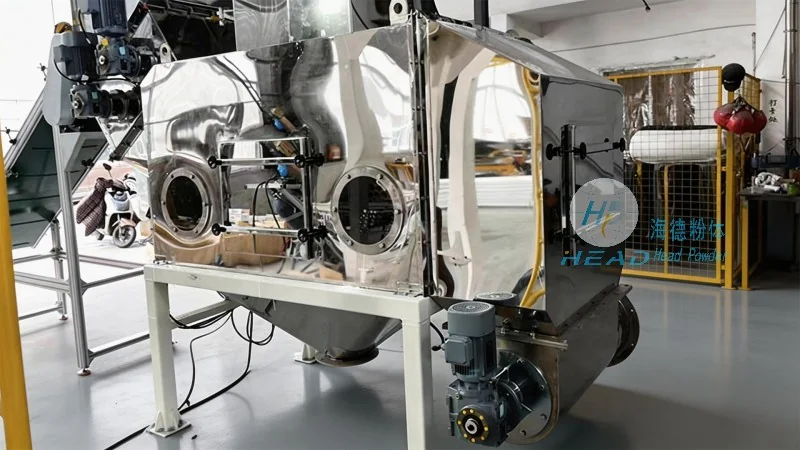
The material handling system for potassium carbonate fertilizer offers several notable advantages that improve operational performance and product quality. Firstly, the system is engineered to handle the granular nature and potential dust generation of potassium carbonate. Dust suppression systems and sealed conveyor components minimize environmental impact and ensure compliance with safety regulations. Secondly, the automated control system enables real-time monitoring and adjustment of material flow, reducing downtime and boosting productivity. The modular design allows for easy scalability, enabling companies to expand capacity as demand grows without significant additional investment. Additionally, the system incorporates energy-efficient components like variable frequency drives for conveyor motors, which lower operational costs and reduce the facility's carbon footprint. The robust construction, using corrosion-resistant and wear-resistant materials, ensures long-term reliability and minimal maintenance requirements.
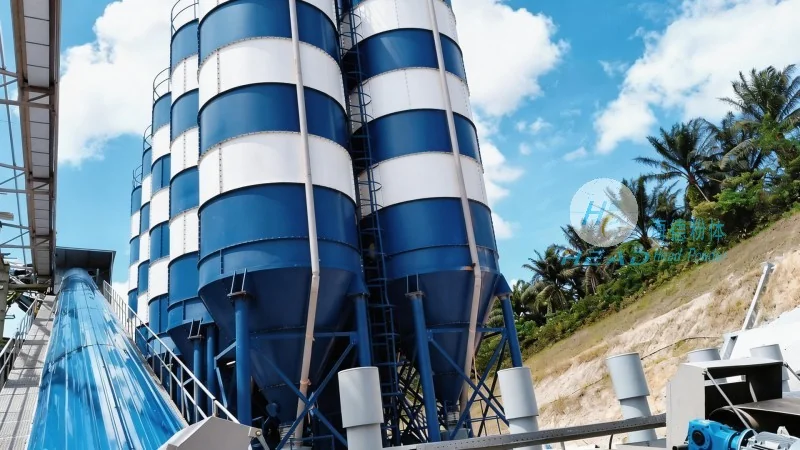
For businesses in the fertilizer industry, implementing a specialized material handling system for potassium carbonate fertilizer can lead to substantial improvements in operational efficiency, product quality, and safety. The system's ability to manage the material's unique characteristics while maintaining high performance standards makes it an essential component for modern fertilizer production facilities. By partnering with Shandong HeadPowder Engineering Co., Ltd., companies can deploy a reliable and efficient system tailored to their specific needs, contributing to enhanced productivity and competitiveness in the market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top