

Working Principle and Features of Pneumatic Conveying Systems for Food Additives
For companies in the food industry, the efficient and safe handling of food additives is a critical concern. Pneumatic conveying systems offer a solution that addresses these needs by providing a hygienic, flexible, and reliable method for transporting bulk materials. This article explores the working principle and key features of such systems, highlighting their importance in modern food processing operations.
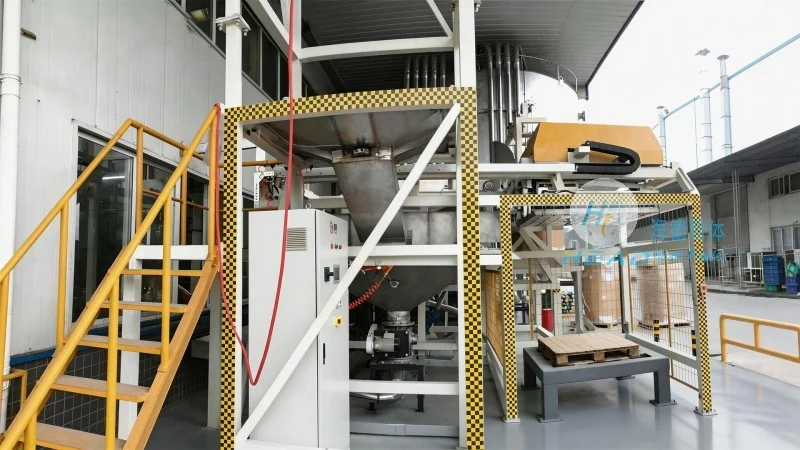
Working Principle of Pneumatic Conveying Systems
The core of a pneumatic conveying system is the use of air or gas to transport solid materials through a pipeline. The process typically involves a few key components: a material feed hopper, a conveyor line (often a flexible tube or rigid pipe), a blower or compressor to generate the air flow, and a discharge point where the material is released. The system operates by creating a pressure differential that propels the material particles forward. There are two main types of pneumatic conveying: dilute phase and dense phase, each with distinct operating characteristics.
In dilute phase systems, the material is carried in a low concentration of particles suspended in the air stream, similar to a cloud. This method is suitable for materials that are free-flowing and non-abrasive, such as powdered food additives. The air velocity is high enough to keep the particles airborne, ensuring smooth transport. Conversely, dense phase systems operate at lower air velocities, where the material is carried in a higher concentration, often forming a plug or slug of material within the air stream. This approach is ideal for handling more abrasive or sensitive materials, as it reduces particle impact and friction, minimizing product degradation.
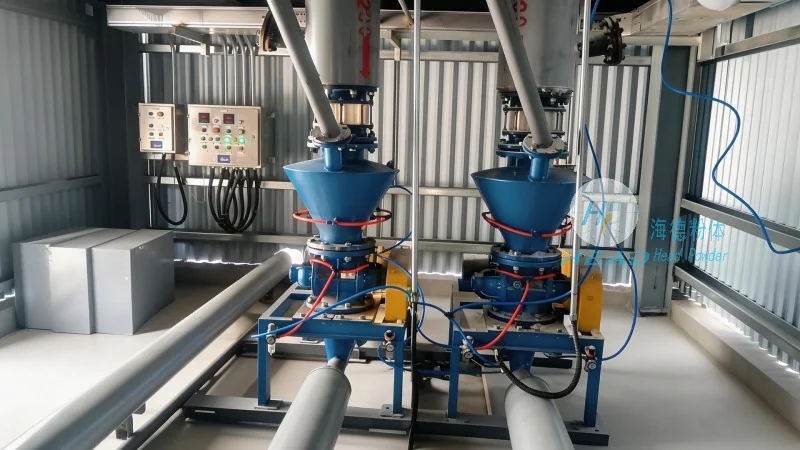
Key Features of Pneumatic Conveying Systems
Several features make pneumatic conveying systems particularly advantageous for food additive applications. Firstly, they provide excellent hygienic performance. The enclosed pipeline design prevents contamination from external sources and minimizes dust exposure, which is crucial for maintaining product quality and compliance with food safety regulations. Secondly, these systems offer high flexibility in terms of layout and material handling. They can be easily integrated into existing production lines and adapted to different processing requirements, allowing for changes in production volume or material types without significant modifications.
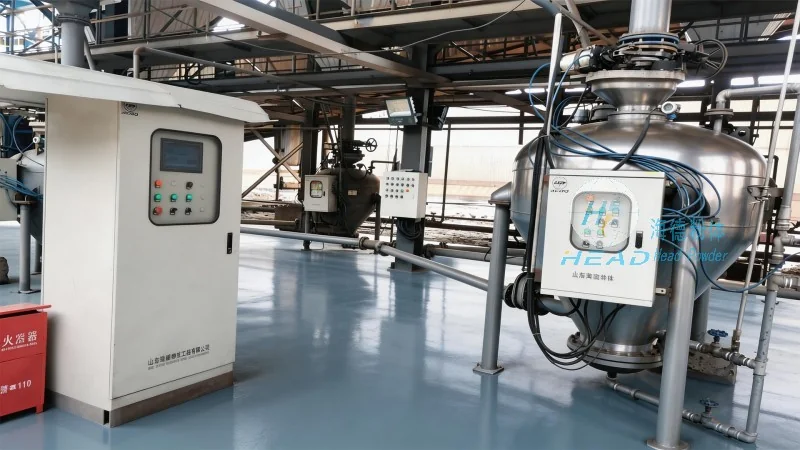
Another important feature is the ability to handle a wide range of particle sizes and densities. From fine powders to larger granules, pneumatic conveying systems can transport various food additives efficiently. This versatility is essential for manufacturers dealing with diverse product portfolios. Additionally, the systems are energy-efficient compared to traditional mechanical conveyors, as they use air pressure rather than mechanical components to move materials. This reduces operational costs and environmental impact, making them a sustainable choice for food processing facilities.
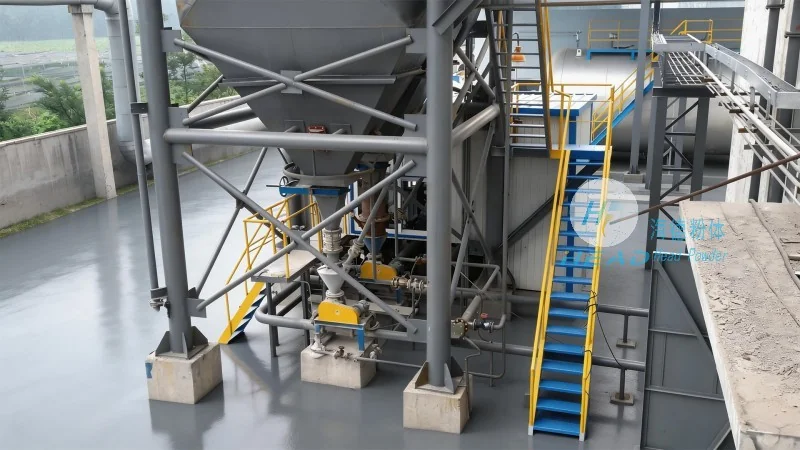
Applications in Food Additive Processing
Pneumatic conveying systems are widely used in the processing of food additives, including flavorings, colorings, preservatives, and vitamins. For example, in the production of powdered flavorings, these systems ensure that the delicate particles are transported without clumping or degradation. Similarly, when handling sensitive colorants, the gentle transport method preserves their color intensity and prevents oxidation. The ability to maintain consistent product quality throughout the conveying process is a significant advantage for food manufacturers, as it directly impacts the final product's taste, appearance, and safety.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized engineering solutions for the food and pharmaceutical industries. With a focus on innovation and quality, the company designs and manufactures advanced pneumatic conveying systems tailored to the unique needs of food additive processing. HeadPowder's expertise lies in creating hygienic, efficient, and reliable equipment that meets the stringent standards of the food industry. The company's commitment to customer satisfaction and product excellence has established it as a trusted partner for businesses seeking to optimize their material handling processes.