With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
High-pressure bin pump pneumatic conveying systems represent a sophisticated technology used in bulk material handling, offering efficient and reliable solutions for transporting powders and granules over long distances. This article delves into the working principle and key features of such systems, providing a comprehensive understanding for industry professionals and potential clients.
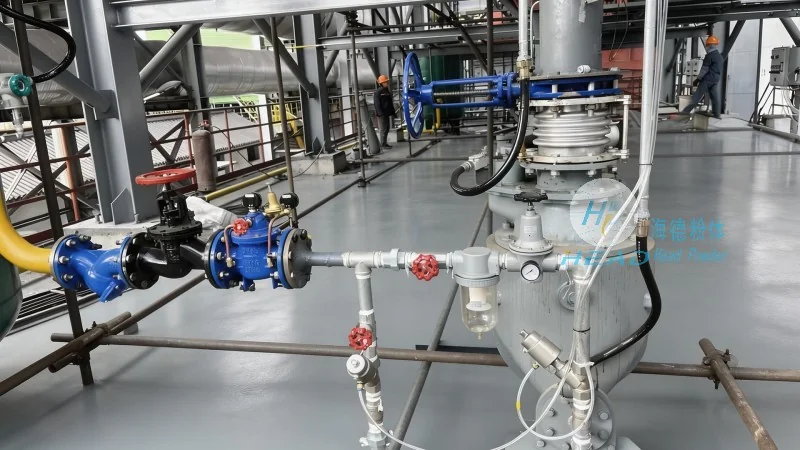
The core of a high-pressure bin pump system lies in its ability to generate high-pressure air or gas to move material through a pipeline. The system typically consists of a hopper, a bin pump, a control unit, and a series of pipelines. The process begins when material is fed into the hopper from a storage silo or other source. The bin pump, often a positive displacement type, draws the material from the hopper and mixes it with the pressurized air or gas. This mixture is then forced through the pipeline to the discharge point, where the material is separated from the air and deposited into the receiving container or process equipment.
A critical component is the bin pump itself, which operates by creating a vacuum or pressure differential to draw material into its chamber. As the pump rotates or moves, the material is trapped and expelled in a controlled manner, ensuring consistent flow rates. The control unit manages the pressure, flow rate, and other parameters to optimize the conveying process, adapting to variations in material type, density, and pipeline length.

High-pressure bin pump systems offer several distinct advantages that make them ideal for various industrial applications. One of the primary features is their ability to handle a wide range of materials, including fine powders, granules, and even abrasive or corrosive substances. The system's design minimizes material degradation and contamination, as the material is enclosed within the pipeline and pump, preventing exposure to external elements.
Efficiency is another significant feature. By operating at high pressures, these systems can transport materials over long distances with minimal energy consumption compared to other conveying methods. The positive displacement nature of the bin pump ensures a consistent and reliable flow, reducing downtime and maintenance requirements. Additionally, the system can be easily integrated with existing infrastructure, allowing for seamless incorporation into production lines.
Reliability is a key characteristic of high-pressure bin pump systems, particularly when operated by reputable manufacturers like Shandong HeadPowder Engineering Co., Ltd. The robust construction and advanced control systems minimize the risk of system failures, ensuring continuous operation. Regular maintenance, including checks on pump seals, air filters, and pipeline integrity, is essential to maintain optimal performance. Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, specializes in the design, manufacturing, and installation of such systems, providing comprehensive support and after-sales services to ensure long-term reliability.
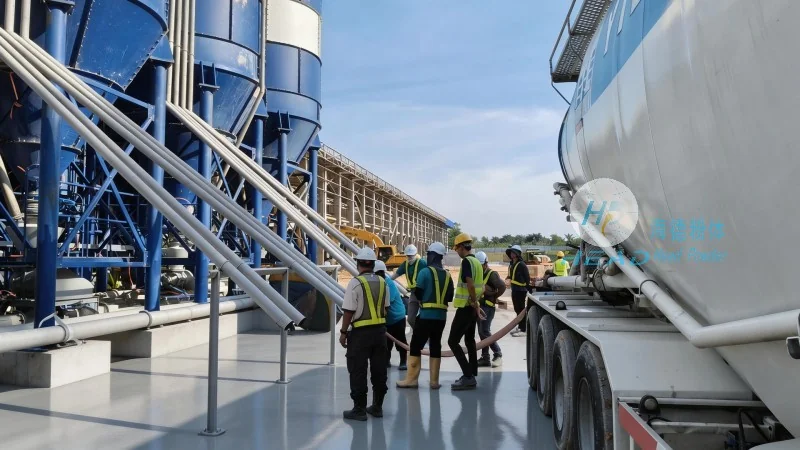
High-pressure bin pump pneumatic conveying systems are widely used in industries such as food processing, pharmaceuticals, chemicals, and mining. Their ability to handle sensitive materials with precision makes them indispensable in sectors where product quality and safety are paramount. The systems contribute to increased productivity by enabling automated material handling, reducing labor costs, and improving overall operational efficiency.
In conclusion, high-pressure bin pump pneumatic conveying systems combine advanced engineering with practical application, offering a reliable and efficient solution for bulk material transport. With features like wide material compatibility, high efficiency, and robust design, these systems are a preferred choice for industries seeking to optimize their material handling processes. Shandong HeadPowder Engineering Co., Ltd. continues to lead in the development and implementation of such technologies, serving clients with expertise and quality in the bulk material handling sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top