

What is a Phosphate Rock Powder Material Handling System Equipment? What Are Its Design Principles?
Phosphate rock powder, a critical raw material in the fertilizer and chemical industries, requires efficient and reliable material handling systems to ensure smooth production processes. The design of such systems is crucial for optimizing performance, minimizing operational costs, and enhancing safety. This article explores the components and design principles of phosphate rock powder material handling systems, with a focus on the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in this field.
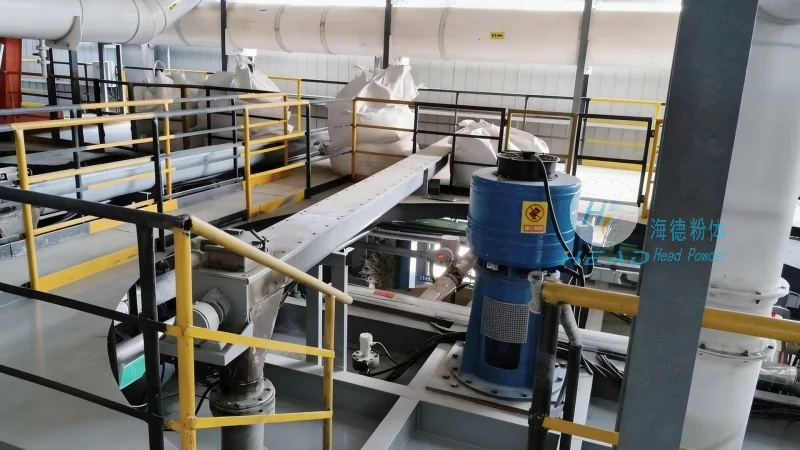
HeadPowder, the professional brand under Shandong HeadPowder Engineering Co., Ltd., specializes in the development and manufacturing of advanced material handling solutions tailored for the phosphate rock industry. With a strong presence in China, the company leverages years of experience to deliver systems that meet the unique challenges of processing and transporting phosphate rock powder.
Key Design Principles for Phosphate Rock Powder Material Handling Systems
The design of a phosphate rock powder material handling system involves several critical principles that ensure efficiency, durability, and safety. First, the system must address the inherent properties of phosphate rock powder, such as its fine particle size, which can lead to dust generation and caking. To mitigate these issues, the design incorporates features like sealed conveying lines and anti-static measures. Second, the system is engineered for high throughput and low maintenance, using robust components that can withstand the abrasive nature of the material. Third, safety is a top priority, with integrated controls and emergency stop mechanisms to prevent accidents during operation. These principles collectively contribute to a system that is both effective and reliable.
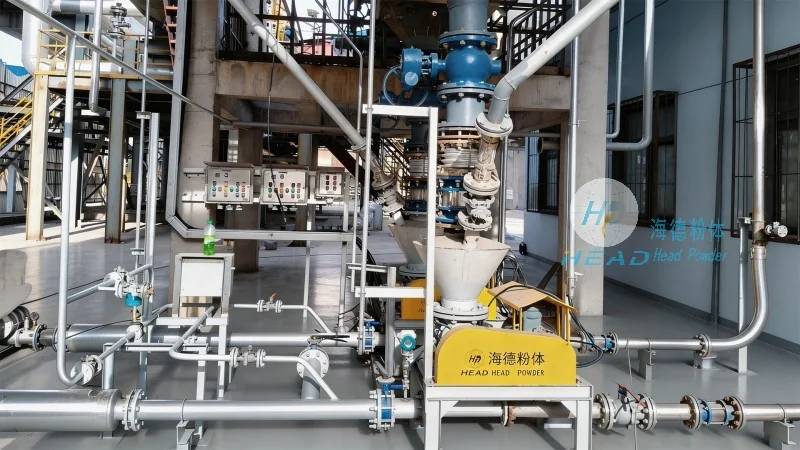
Components of a Phosphate Rock Powder Material Handling System
A typical phosphate rock powder material handling system consists of several key components, each playing a vital role in the overall operation. The primary components include feeders, conveyors, storage silos, and processing equipment. Feeders, such as rotary or vibratory types, ensure a consistent and controlled flow of powder from the source to the conveyor. Conveyors, often using pneumatic or mechanical methods, transport the powder to the storage or processing areas. Storage silos are designed to hold large quantities of powder, with features like aeration to prevent caking and maintain material quality. Processing equipment, such as crushers or classifiers, may be integrated into the system to prepare the powder for further use. Each component is selected based on the specific requirements of the application, ensuring optimal performance and longevity.
Advantages of Using a Phosphate Rock Powder Material Handling System
Implementing a specialized material handling system for phosphate rock powder offers numerous advantages for industrial operations. One of the most significant benefits is the reduction in operational costs. By minimizing material loss and optimizing energy consumption, the system helps lower overall production expenses. Additionally, the system enhances production efficiency by ensuring a steady supply of powder to processing units, reducing downtime and increasing output. Another key advantage is improved safety. The sealed and controlled environment of the system prevents dust exposure and reduces the risk of accidents, creating a safer working environment for personnel. Furthermore, the system’s durability and low maintenance requirements contribute to long-term cost savings and reliable operation.
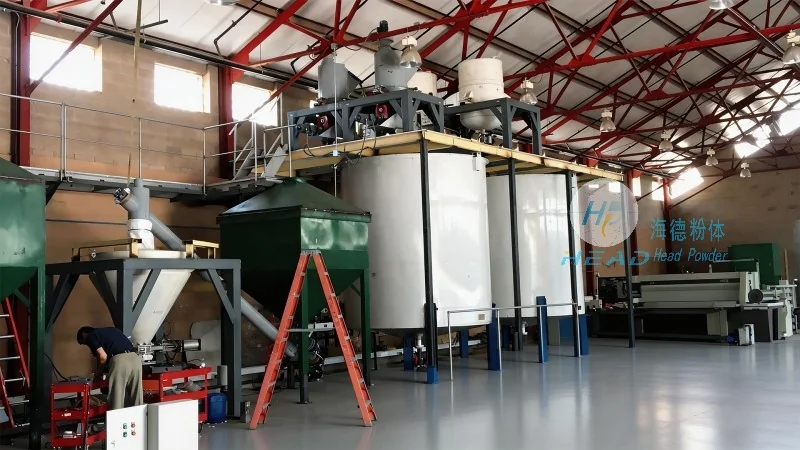
Applications in the Phosphate Rock Industry
Phosphate rock powder material handling systems are widely used in various applications within the phosphate rock industry. In fertilizer production, the system efficiently transports raw phosphate rock to processing plants, where it is converted into phosphoric acid and other fertilizers. In chemical manufacturing, the system delivers phosphate rock powder to facilities that produce phosphates for industrial uses, such as detergents and food additives. Additionally, the system is utilized in mining operations to transport phosphate ore from the mine to processing sites. In each of these applications, the system’s design ensures that the material is handled safely and efficiently, meeting the specific needs of the industry.
HeadPowder’s Commitment to Quality and Innovation
Shandong HeadPowder Engineering Co., Ltd. is committed to providing high-quality, reliable material handling systems for the phosphate rock industry. The company’s team of engineers and technicians works closely with clients to understand their specific requirements and develop customized solutions. By leveraging advanced technology and rigorous quality control, HeadPowder ensures that its systems meet or exceed industry standards. The company also offers comprehensive after-sales support, including maintenance services and technical assistance, to ensure the long-term performance of the equipment. With a focus on customer satisfaction and innovation, HeadPowder continues to be a trusted partner for businesses in the phosphate rock industry.