With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Metering bin pump pneumatic conveying systems represent a sophisticated and efficient method for transporting bulk materials over long distances or through complex layouts. At the core of this technology is the integration of a metering bin, a pump, and a pneumatic conveying pipeline, all working in tandem to ensure precise material handling and reliable operation. This system is widely used in various industries, including chemical, food processing, and pharmaceuticals, where the need for accurate dosing and contamination-free transport is paramount. HeadPowder, a leading manufacturer based in Shandong, China, specializes in designing and manufacturing these systems to meet the diverse needs of industrial clients. The company's expertise in material handling technology ensures that each system is tailored to the specific requirements of the application, providing optimal performance and reliability.
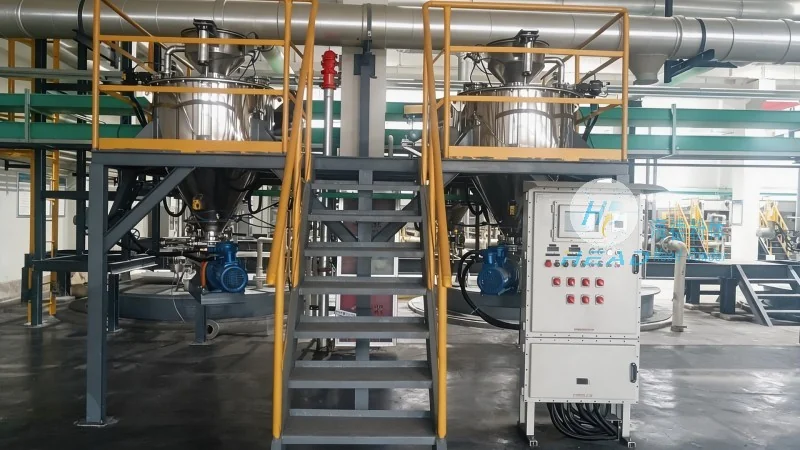
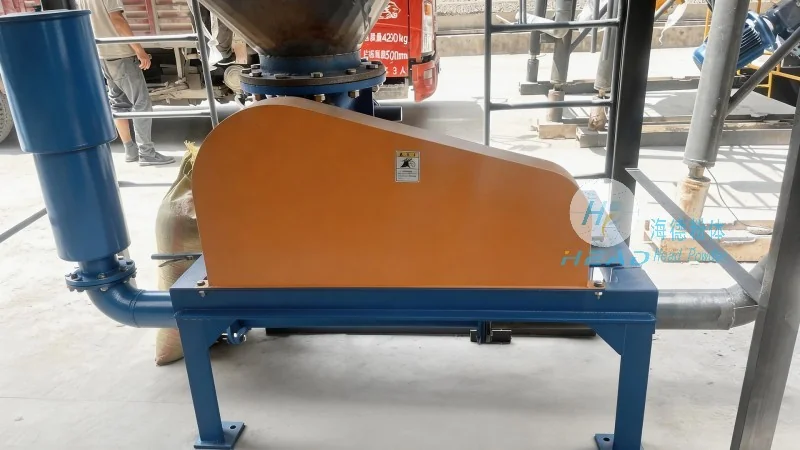
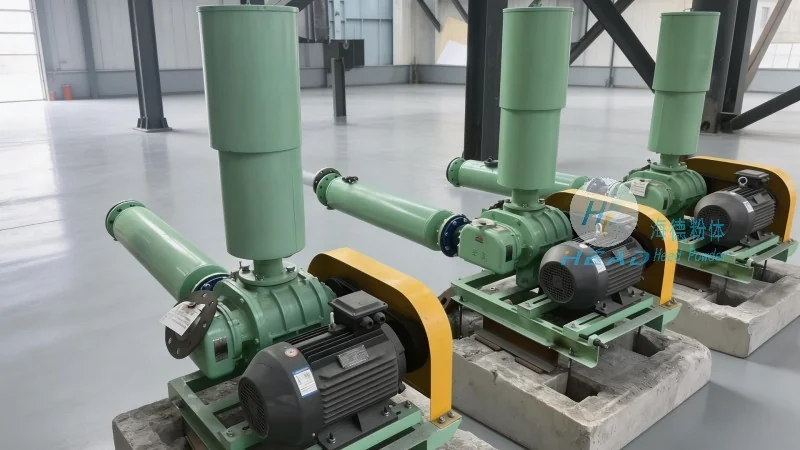
The effectiveness of a metering bin pump system relies on several critical components, each playing a specific role in the overall operation. The metering bin serves as the storage and feeding unit, providing a controlled volume of material to the pump. It often includes features such as level sensors and flow control mechanisms to maintain consistent material feed rates. The pump, typically a positive displacement type, generates the necessary pressure to move the material through the conveying pipeline. This pump is designed to handle the specific characteristics of the bulk material, such as particle size, density, and moisture content. The pneumatic conveying pipeline, usually made of stainless steel or other corrosion-resistant materials, transports the material from the source to the destination. It may include bends, valves, and filters to ensure smooth and efficient material flow. Additionally, the system may incorporate a control panel that monitors and regulates the operation of all components, ensuring optimal performance and safety. The control panel typically includes sensors for pressure, flow, and level, as well as indicators for system status and alarms for any issues that may arise.
The design principles of metering bin pump pneumatic conveying systems are centered on achieving precision, efficiency, and reliability. One of the primary design goals is to maintain a consistent material flow rate, which is crucial for applications requiring accurate dosing, such as in chemical manufacturing or food processing. This is achieved through the integration of the metering bin, which provides a controlled feed, and the pump, which delivers the material at a steady pressure. The system is also designed to handle a wide range of bulk materials, from fine powders to coarse granules, by adjusting the pump speed and the bin's feeding mechanism. Another key design principle is the prevention of material degradation or contamination. This is achieved through the use of corrosion-resistant materials for the pipeline and components, as well as the incorporation of filters and cleaning mechanisms to remove dust or debris. The system is also designed for easy maintenance and operation, with accessible components and clear control interfaces. Finally, the design prioritizes energy efficiency, using the pump and conveying system in a way that minimizes power consumption while maintaining performance. Engineers often consider factors such as material properties, transport distance, and required flow rate when designing the system to ensure it meets the specific needs of the application.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top