With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Coal slurry, a vital component in the coal processing industry, relies on precise technical parameters and optimized conveying system processes to ensure efficient transportation and utilization. This article delves into the key aspects of coal slurry technical specifications and the operational workflow of conveying systems, providing insights into how these elements contribute to industrial efficiency and reliability.
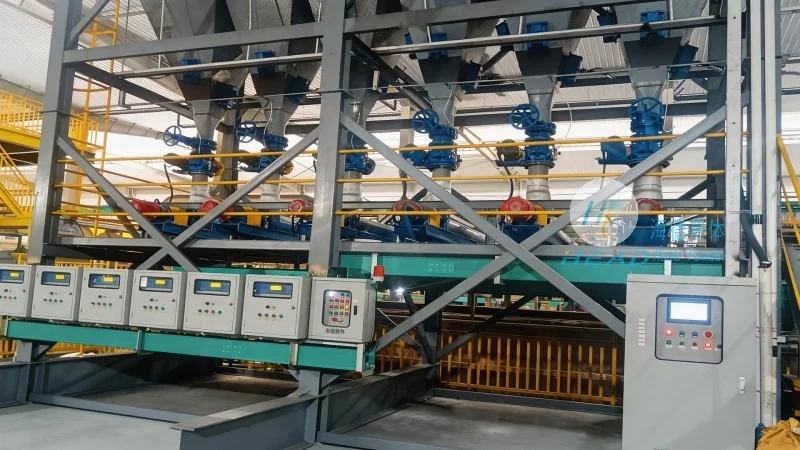
HeadPowder, a prominent engineering firm headquartered in Shandong, China, specializes in delivering comprehensive solutions for coal slurry handling and conveying systems. With a strong commitment to technical innovation and industrial excellence, HeadPowder has built a reputation as a trusted partner in the coal processing sector, offering tailored engineering services and equipment that meet the unique needs of clients worldwide.
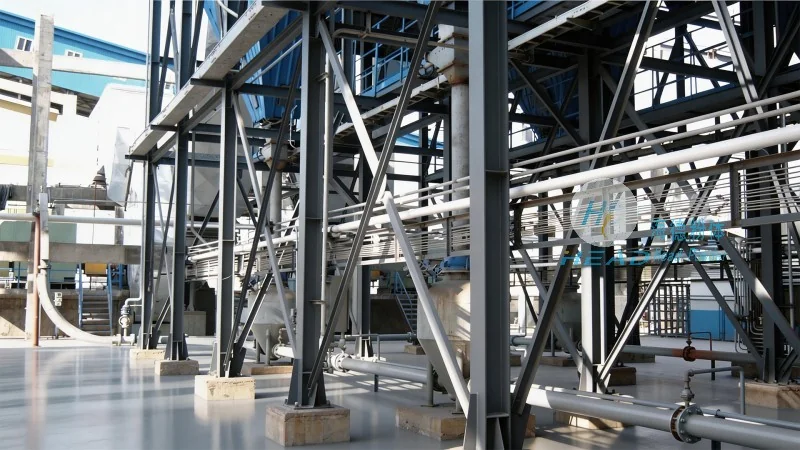
The technical parameters of coal slurry are fundamental to the performance and stability of conveying systems. These parameters encompass slurry concentration, viscosity, density, and particle size distribution, each playing a critical role in system operation. Slurry concentration, typically expressed as a percentage of solid content, directly influences flow rates and pipeline capacity. Higher concentrations may increase flow efficiency but also raise the risk of blockages if not properly managed. Viscosity, affected by temperature and particle size, impacts pump selection and system head requirements. For example, higher viscosity may necessitate more powerful pumps to maintain adequate flow, while lower viscosity allows for more energy-efficient operation. Density variations, resulting from changes in coal and water ratios, affect system pressure and energy consumption. Particle size distribution is crucial for determining the suitability of pipeline materials and pump types, as larger particles can cause increased wear and tear on equipment. Proper characterization of these parameters enables engineers to design systems that are optimized for specific applications, ensuring reliable and cost-effective operation.
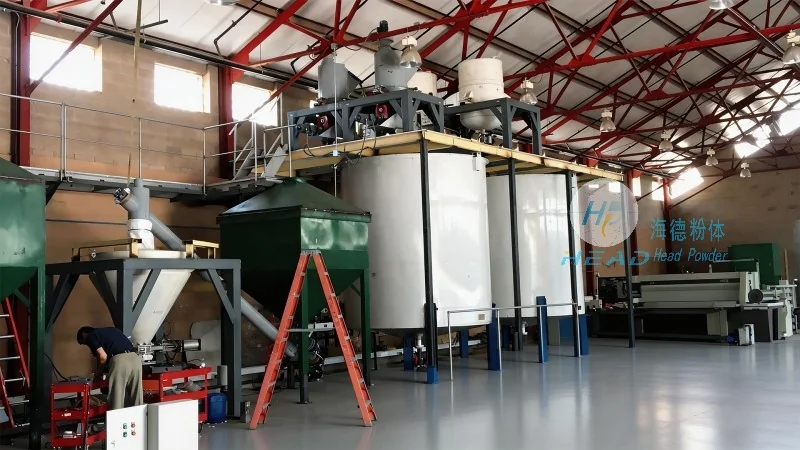
The coal slurry conveying system operates through a systematic process that begins with slurry preparation at the source. This involves mixing raw coal with water to achieve the desired slurry concentration, followed by screening and filtration to remove oversized particles and impurities. The prepared slurry is then pumped through a network of pipelines, which may include vertical and horizontal sections, using high-pressure pumps specifically designed for slurry transport. The system incorporates essential components such as valves, regulators, and monitoring devices to control flow rates, pressure, and temperature. Real-time monitoring of slurry parameters—including flow rate, pressure, and viscosity—is critical for maintaining system stability and detecting potential issues before they escalate. Regular maintenance and inspection of pipelines, pumps, and other components are also vital to ensure long-term reliability and minimize downtime. The process concludes with the delivery of slurry to the intended destination, such as a processing plant or storage facility, where it is further processed or utilized.
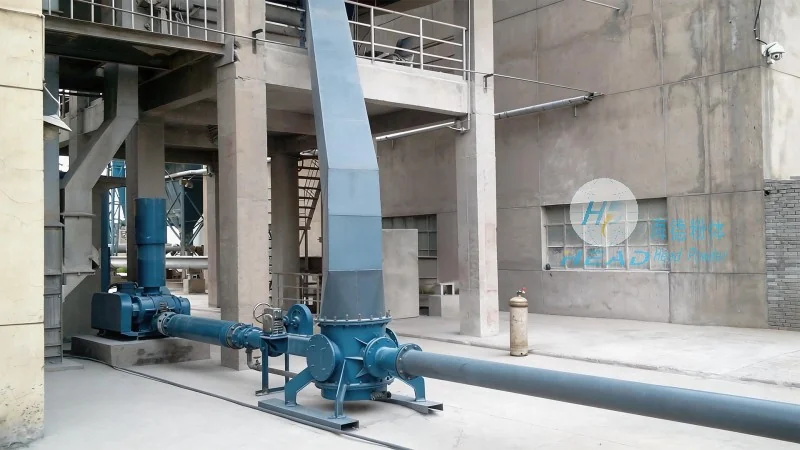
Implementing advanced coal slurry technical parameters and conveying system processes offers significant advantages for industrial operations. Efficient slurry transport reduces transportation costs compared to traditional methods like truck or rail transport, as it allows for the movement of large volumes of material over long distances with lower energy consumption. Optimized system designs minimize operational risks, including pipeline blockages and equipment failure, which can lead to substantial downtime and financial losses. Precise control of slurry parameters ensures consistent product quality, which is essential for downstream processing applications. The integration of monitoring and control technologies enables proactive maintenance, extending the lifespan of equipment and reducing maintenance costs. Overall, the adoption of advanced coal slurry conveying systems enhances operational efficiency, improves safety, and supports sustainable industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top