With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industries dealing with phosphate rock powder, the efficiency and safety of material transport are critical. Pneumatic conveying systems offer a robust method to move these fine powders, but challenges such as dust leakage can compromise both operational integrity and worker safety. This article explores effective strategies to prevent dust leakage in pneumatic conveying systems specifically when handling phosphate rock powder, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. (headpowder), a leading provider of specialized engineering solutions.
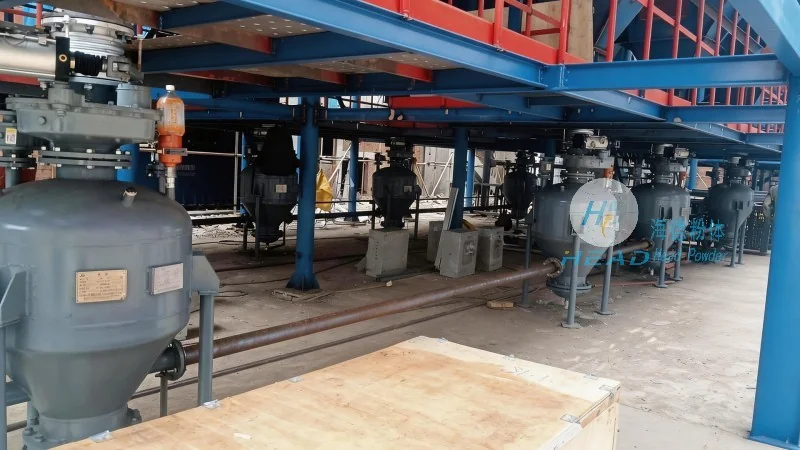
Phosphate rock powder is characterized by its fine particle size and high dust generation potential during handling. When using pneumatic conveying, the system must maintain a sealed environment to prevent air and powder from escaping, which can lead to environmental contamination and health hazards. Traditional systems may struggle with maintaining tight seals, especially under varying pressure and temperature conditions. headpowder recognizes these challenges and has developed advanced solutions tailored to the unique properties of phosphate rock powder.
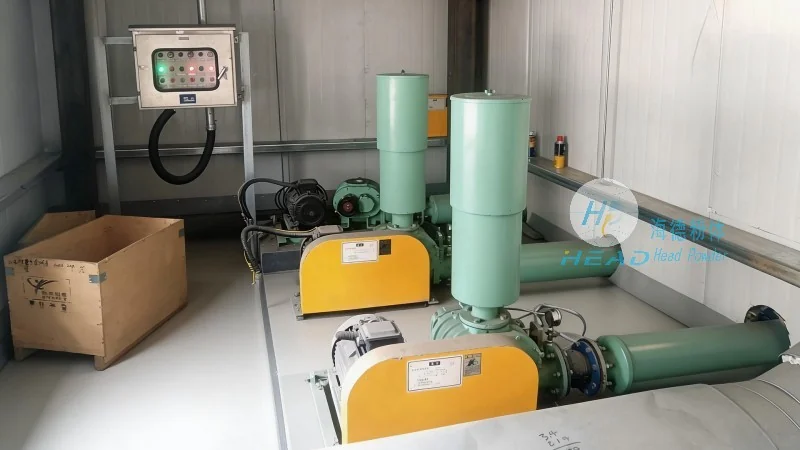
headpowder employs several key technologies to ensure effective dust control in pneumatic conveying systems. One of the primary methods is the use of high-quality, airtight components such as seals, valves, and hoppers. These components are designed to withstand the abrasive nature of phosphate rock powder, ensuring long-term performance without compromising sealing efficiency. Additionally, the company utilizes advanced material handling equipment, including rotary valves and pressure vessels, which are engineered to maintain consistent pressure and minimize air leakage points.
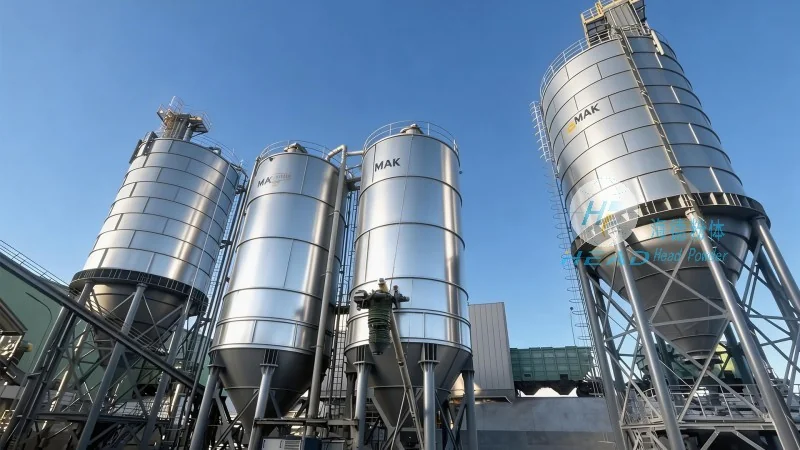
Proper seal design is crucial for preventing dust leakage. headpowder’s engineers design seals that are compatible with the chemical and physical properties of phosphate rock powder, ensuring they remain effective over time. Regular maintenance is also a critical aspect of preventing leakage. The company recommends routine inspections and replacements of seals, as well as the use of lubricants and protective coatings to extend the lifespan of sealing components. By implementing these strategies, facilities can significantly reduce the risk of dust leakage and maintain a safe working environment.
headpowder offers customized pneumatic conveying systems that are tailored to the specific needs of phosphate rock powder handling operations. The company works closely with clients to assess their unique requirements, including material flow rates, distance, and environmental regulations. By integrating advanced control systems and monitoring tools, headpowder ensures that the conveying system operates at optimal efficiency while maintaining strict dust control standards. This customized approach not only enhances performance but also helps clients comply with local and international safety regulations.
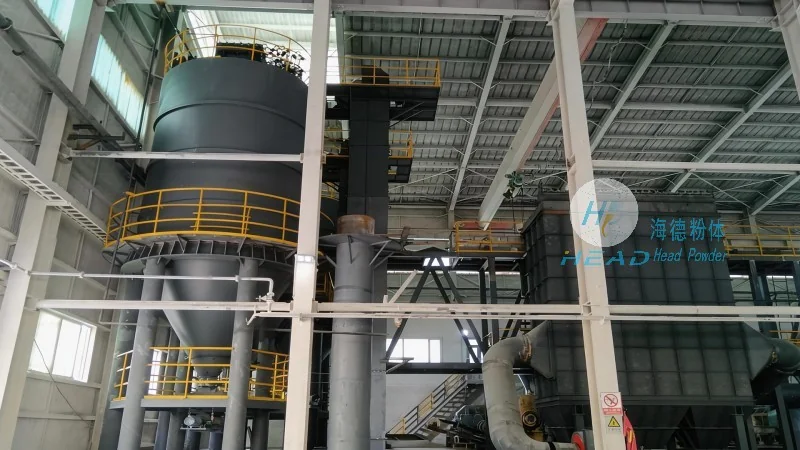
Partnering with headpowder provides numerous benefits for industries handling phosphate rock powder. The company’s expertise in pneumatic conveying technology ensures that systems are designed to minimize dust leakage, reducing operational costs associated with cleanup and environmental compliance. Additionally, headpowder’s commitment to quality and customer service ensures that clients receive reliable, long-lasting solutions that meet their specific needs. By choosing headpowder, businesses can enhance safety, improve operational efficiency, and maintain compliance with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top