

Working Principle and Features of Borax Pneumatic Conveying Equipment
HeadPowder, a leading manufacturer in the field of material handling equipment, specializes in the design, production, and supply of advanced pneumatic conveying systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for industries requiring efficient and reliable transport solutions. Based in Shandong, China, HeadPowder leverages years of expertise to deliver customized solutions tailored to the unique needs of clients across various sectors.
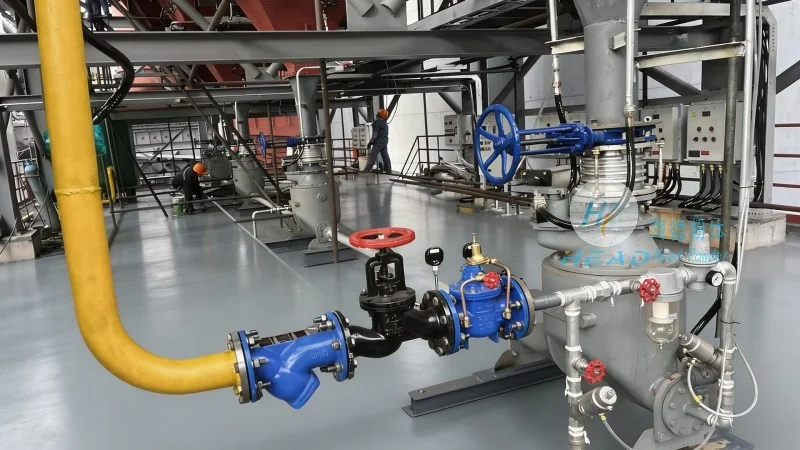
Introduction to Borax Pneumatic Conveying Equipment
Borax, a white crystalline powder commonly used in industrial applications such as glass manufacturing, detergents, and chemical processing, often requires specialized handling equipment to ensure safe and efficient transport. Pneumatic conveying systems, which utilize air or gas to move bulk materials, have become a preferred choice for borax handling due to their ability to handle fine powders and minimize dust exposure. HeadPowder's borax pneumatic conveying equipment is engineered to meet the demanding requirements of borax processing, offering a combination of performance, durability, and user-friendly operation.
Working Principle of Borax Pneumatic Conveying Systems
The core mechanism of borax pneumatic conveying equipment involves the use of a pressure or vacuum system to transport the material. In a typical pressure system, a blower or compressor generates compressed air that forces the borax particles through a pipeline. The air flow creates a low-pressure zone at the discharge point, drawing the material from the source and propelling it to the destination. This method is particularly effective for short to medium-distance transport and can handle a wide range of particle sizes and moisture content. The vacuum system operates on the opposite principle, using a vacuum pump to create a negative pressure that pulls the material into the pipeline. This approach is often used for longer distances or when the material needs to be transported from multiple sources to a central collection point.
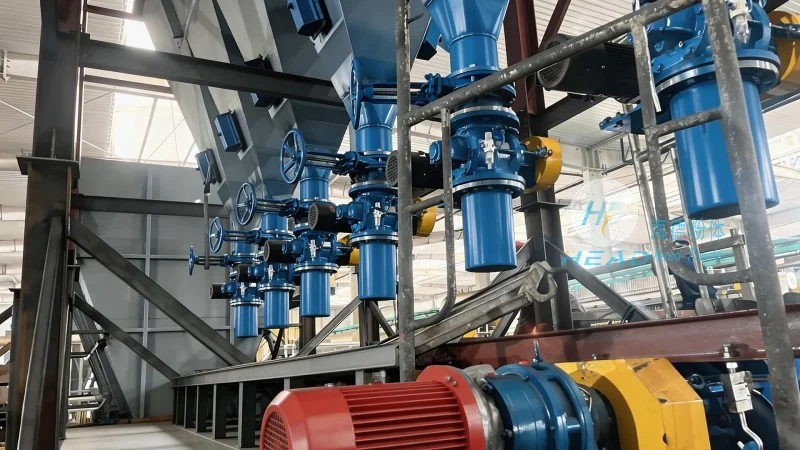
Key Features of Borax Pneumatic Conveying Equipment
HeadPowder's borax pneumatic conveying equipment is characterized by several key features that enhance its performance and usability. Firstly, the equipment is designed with high-efficiency air filtration systems to minimize dust emissions and ensure compliance with environmental regulations. This not only protects the environment but also maintains the quality of the borax by preventing contamination from external particles. Secondly, the system incorporates advanced control mechanisms that allow for precise regulation of air flow and pressure, ensuring consistent and reliable material transport. These controls can be adjusted in real-time to accommodate variations in material properties or process demands, providing flexibility and adaptability. Thirdly, the equipment is constructed from high-quality materials, such as stainless steel and corrosion-resistant alloys, which are resistant to the chemical properties of borax and other aggressive substances. This durability ensures long-term operation with minimal maintenance, reducing downtime and operational costs for clients. Additionally, the design incorporates easy-to-clean components and access points, facilitating regular maintenance and cleaning to maintain optimal performance. The equipment also features safety mechanisms, including pressure relief valves and emergency shut-off systems, to prevent accidents and protect personnel during operation.
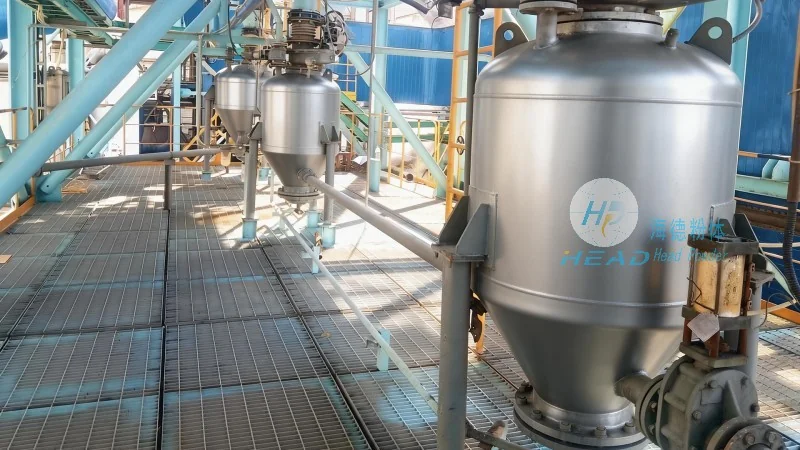
Benefits of Using Borax Pneumatic Conveying Equipment
The adoption of borax pneumatic conveying equipment offers numerous benefits for industrial applications. One of the primary advantages is the significant reduction in labor costs associated with manual handling of bulk materials. By automating the transport process, companies can minimize the need for manual labor, leading to increased efficiency and reduced operational expenses. Additionally, the equipment helps to improve workplace safety by eliminating the need for manual handling of fine powders, which can pose health risks such as respiratory issues. The enclosed system also prevents dust from spreading into the environment, reducing the risk of contamination and improving overall air quality. Another key benefit is the ability to transport borax over longer distances without the need for intermediate storage or transfer points. This streamlines the production process and enhances overall operational efficiency. Furthermore, the equipment's ability to handle varying particle sizes and moisture content makes it versatile and suitable for a wide range of industrial applications. The consistent and reliable transport of borax ensures that downstream processes, such as mixing or processing, receive a uniform material feed, leading to improved product quality and reduced waste.
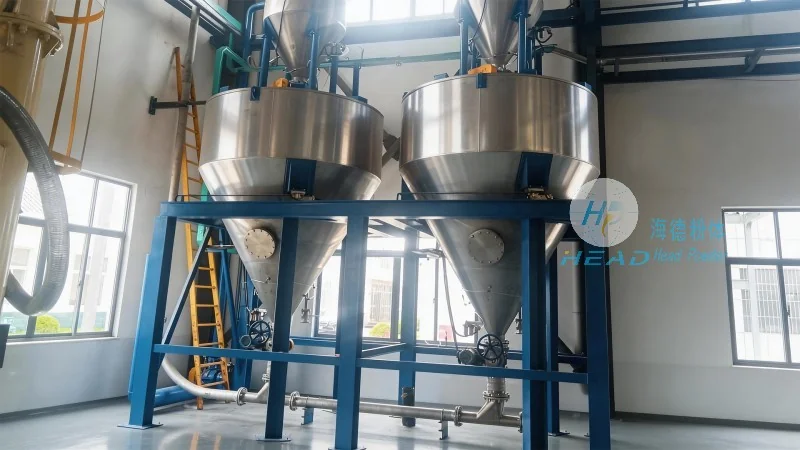
Application Examples in Industrial Settings
Borax pneumatic conveying equipment is widely used in various industrial settings where efficient material transport is critical. In the glass manufacturing industry, for example, borax is used as a flux to lower the melting point of silica, and pneumatic conveying systems are used to transport the borax from storage silos to the glass melting furnaces. The equipment ensures that the borax is delivered in a controlled manner, maintaining the required moisture content and particle size distribution. In the detergent and cleaning product industry, borax is used as a key ingredient, and the pneumatic conveying system helps to transport it from raw material storage to production lines. This ensures a consistent supply of borax, which is essential for maintaining product quality and meeting production targets. In the chemical processing industry, borax is used in the production of various chemicals, and the pneumatic conveying equipment facilitates the transport of the material from reaction vessels to storage tanks. The system's ability to handle high temperatures and corrosive substances makes it suitable for these demanding applications. Additionally, in the food processing industry, where borax may be used as a food additive, the equipment's hygienic design and enclosed system help to maintain the purity of the material, ensuring compliance with food safety regulations.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, stands as a leading provider of borax pneumatic conveying equipment, offering innovative solutions that enhance the efficiency and safety of material handling processes. The company's commitment to quality, durability, and customer satisfaction has earned it a reputation as a trusted partner in the industry. By leveraging advanced engineering and manufacturing techniques, HeadPowder delivers equipment that meets the highest standards of performance and reliability. The working principle and features of the borax pneumatic conveying systems, as described above, highlight the company's expertise in designing equipment tailored to the specific needs of borax handling. With a focus on continuous improvement and customer support, HeadPowder remains dedicated to providing solutions that drive operational excellence and sustainable growth for its clients.