With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Mineral granular material conveying is a critical industrial process that involves the transportation of solid particles, such as minerals, ores, coal, and other bulk materials. This method is widely used in various industries, including mining, construction, and chemical manufacturing, to move large quantities of materials efficiently from one location to another. The process typically relies on mechanical systems like conveyor belts, screw conveyors, and pneumatic conveyors, each designed to handle different types of granular materials based on their size, density, and flow characteristics.
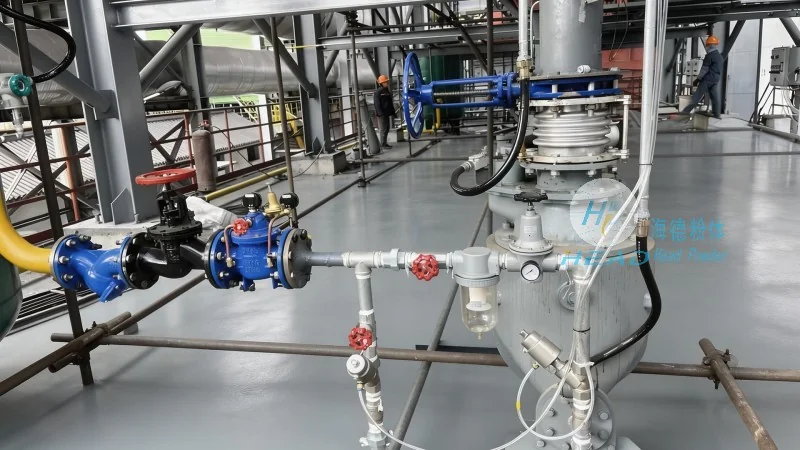
The primary goal of mineral granular material conveying is to ensure reliable, continuous, and safe movement of bulk materials. It plays a vital role in optimizing production workflows, reducing labor costs, and improving overall operational efficiency. By eliminating the need for manual handling and reducing material loss, these systems contribute significantly to cost savings and environmental sustainability in industrial operations.
The design of mineral granular material conveying systems is governed by several key principles that ensure optimal performance and longevity. First, the system must be capable of handling the specific characteristics of the material being conveyed, including particle size distribution, moisture content, and abrasiveness. Engineers must consider these factors to select appropriate equipment and materials that can withstand the stresses and wear associated with the material.
Second, the conveying capacity and speed are critical design parameters. The system must be able to meet the required throughput while maintaining a consistent flow rate. This involves calculating the material's bulk density, flow rate, and the dimensions of the conveyor or duct to ensure that the system can handle the intended volume without bottlenecks or blockages.
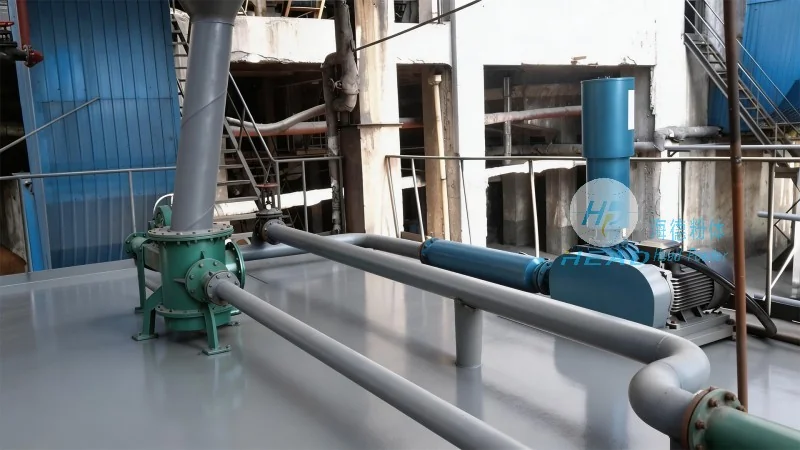
Third, the energy efficiency of the conveying system is a key consideration. Modern designs prioritize energy-saving mechanisms, such as variable speed drives and optimized airflow in pneumatic systems, to reduce operational costs. Additionally, the system's durability and maintenance requirements are evaluated to ensure long-term reliability and minimal downtime.
HeadPowder, a leading provider of mineral processing and material handling solutions, specializes in designing and manufacturing advanced conveying systems for the mineral industry. With a strong presence in Shandong, China, the company has built a reputation for delivering high-quality, customized solutions that meet the unique needs of its clients. HeadPowder's team of experienced engineers and technicians leverages cutting-edge technology and industry best practices to develop systems that enhance productivity and safety in mineral processing operations.
HeadPowder's facilities and expertise enable the company to offer comprehensive services, from initial system design and engineering to installation, commissioning, and ongoing maintenance. The company's commitment to quality and customer satisfaction is reflected in its adherence to international standards and rigorous testing protocols. By partnering with HeadPowder, clients gain access to reliable, efficient, and cost-effective mineral granular material conveying solutions that drive their business forward.
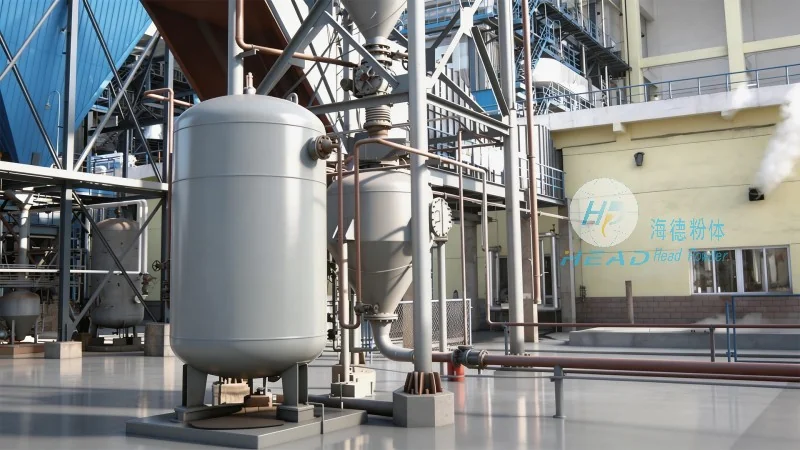
HeadPowder's mineral granular material conveying systems are engineered with features that address the specific challenges of handling various mineral types. For example, the company's screw conveyors are designed to handle dry, free-flowing materials with minimal clogging, while its pneumatic conveyors are ideal for transporting fine powders and dust. The systems are also equipped with advanced control systems that allow for real-time monitoring and adjustment of conveying parameters, ensuring optimal performance under varying conditions.
These conveying systems find applications in a wide range of industries, including mining, where they are used to transport ore from mines to processing plants; in construction, where they help move sand, gravel, and other aggregates to building sites; and in chemical manufacturing, where they facilitate the handling of raw materials and finished products. The versatility and reliability of HeadPowder's solutions make them a preferred choice for businesses seeking to improve their material handling processes and achieve higher operational efficiency.
In conclusion, mineral granular material conveying is a fundamental process in modern industrial operations, and the design principles behind these systems are crucial for their effectiveness. Companies like Shandong HeadPowder Engineering Co., Ltd. play a vital role in providing advanced solutions that meet the evolving needs of the industry. By focusing on material characteristics, system efficiency, and durability, these systems ensure reliable and sustainable material transport, contributing to the success of industrial enterprises worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top