With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Phosphate powder pneumatic conveying systems are essential in industrial applications where the efficient transport of bulk materials like phosphate is required. These systems utilize air or other gases to move powder materials through pipelines, offering a dust-free and flexible solution compared to traditional mechanical conveying methods. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd., based in China, specializes in designing and manufacturing such systems tailored to meet the specific needs of various industries.
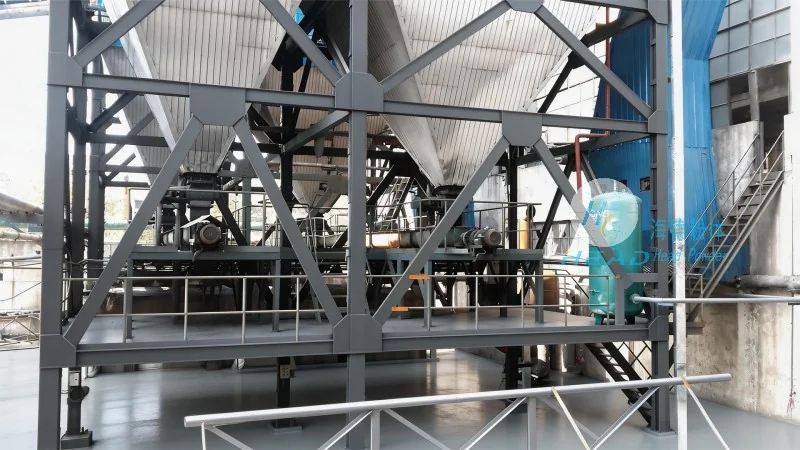
A typical phosphate powder pneumatic conveying system consists of several key components. The primary elements include a material feeder, which ensures a consistent flow of powder into the system; a conveying pipeline, where the powder is transported by the air stream; a pressure vessel or receiver, which collects the material at the end of the pipeline; and a blower or compressor that generates the necessary air pressure. Additionally, control valves and filters are often integrated to regulate the flow and maintain system efficiency. Each component plays a crucial role in ensuring the smooth and reliable operation of the entire system.
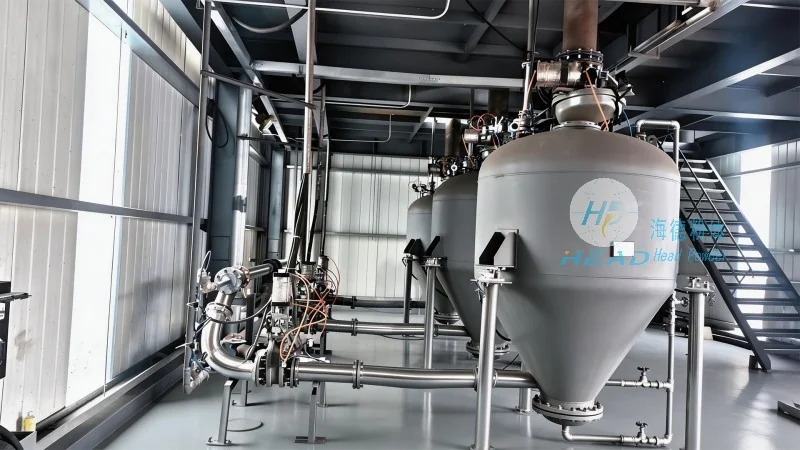
The design of a phosphate powder pneumatic conveying system follows specific principles to optimize performance and minimize operational issues. One of the fundamental principles is the selection of appropriate air velocity, which must be high enough to prevent material settling in the pipeline but low enough to avoid excessive wear and energy consumption. The system's design also considers the particle size and density of the phosphate powder, as these factors influence the required air pressure and flow rate. Furthermore, the layout of the pipeline, including the number of bends and vertical sections, is carefully planned to maintain consistent air flow and prevent blockages. Shandong HeadPowder Engineering Co., Ltd. employs advanced engineering techniques to ensure that each system is designed with these principles in mind, resulting in efficient and reliable operation.
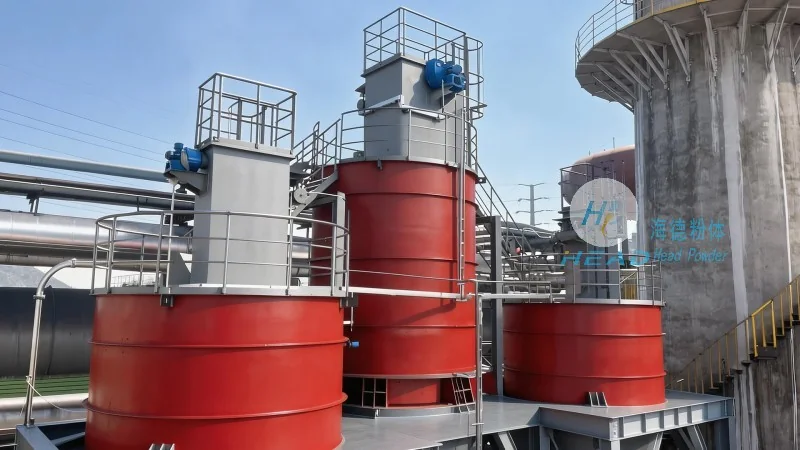
Compared to traditional mechanical conveying methods, phosphate powder pneumatic conveying systems offer several advantages. One of the most significant benefits is the ability to transport materials in a dust-free environment, which enhances workplace safety and reduces the risk of material contamination. Additionally, these systems provide flexibility in terms of layout, as they can be easily reconfigured to accommodate changes in production processes or facility expansions. The use of air as the conveying medium also allows for the transport of materials over long distances without the need for multiple transfer points. Furthermore, pneumatic conveying systems can handle a wide range of particle sizes and densities, making them suitable for various phosphate applications.
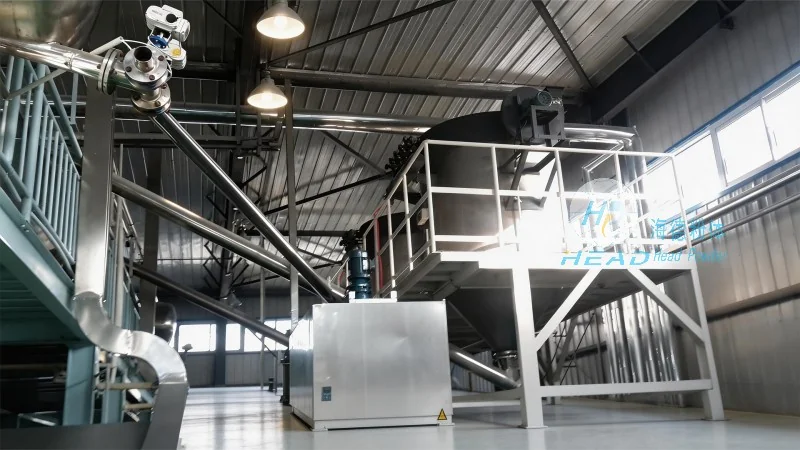
Phosphate powder pneumatic conveying systems are widely used in various industries, including the chemical, food, and agricultural sectors. In the chemical industry, these systems are used to transport raw materials like phosphate to production facilities, where they are processed into fertilizers or other chemical products. In the food industry, they are employed to move phosphate-based ingredients in food processing plants, ensuring a hygienic and efficient transfer process. The agricultural sector also benefits from these systems, as they are used to transport phosphate fertilizers to farms, improving the efficiency of fertilizer distribution. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented these systems in numerous projects across different industries, demonstrating their versatility and effectiveness.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top