With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Corn feed, a fundamental component in animal nutrition, necessitates efficient and reliable handling systems to preserve feed quality and streamline process flow. Pneumatic conveying equipment has become a preferred solution for transporting corn feed and other bulk powders due to its ability to handle fine particles, minimize dust, and maintain product integrity. This article explores the structure and operational principles of corn feed pneumatic conveying systems, detailing key components and their functional roles.
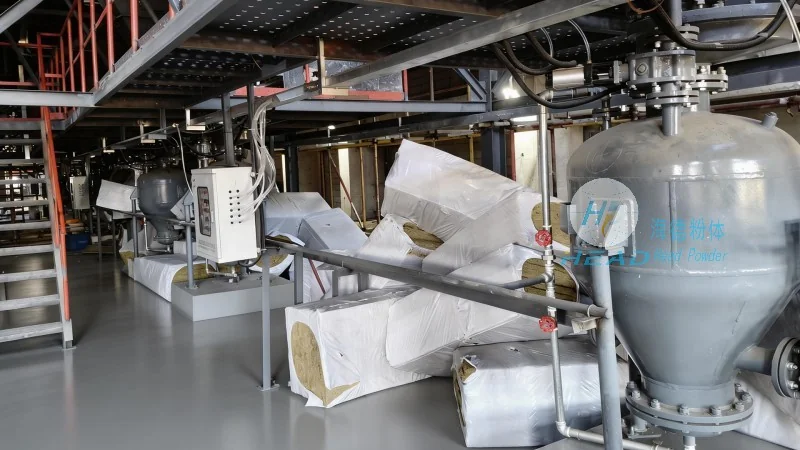
The corn feed pneumatic conveying system typically comprises several critical components that operate in unison to achieve effective material transport. The primary elements include a hopper or feeder for material storage and feeding, a conveying pipeline network, a blower or air compressor to generate the necessary air flow, a separation or filter system to remove dust and particles from the air stream, and a discharge outlet for the conveyed material. Each component plays a crucial role in the overall efficiency and performance of the system.
The conveying pipeline serves as the backbone of the pneumatic system, responsible for transporting corn feed particles through the air stream. The pipeline is usually constructed from stainless steel or other corrosion-resistant materials to withstand the abrasive nature of corn feed and prevent contamination. The design of the pipeline, including its diameter, length, and bends, is meticulously engineered to minimize pressure drop and ensure smooth material flow. The system may employ either positive pressure or negative pressure (vacuum) to move the material, with positive pressure being more common for corn feed applications due to its capacity to handle larger particles and higher material loads.
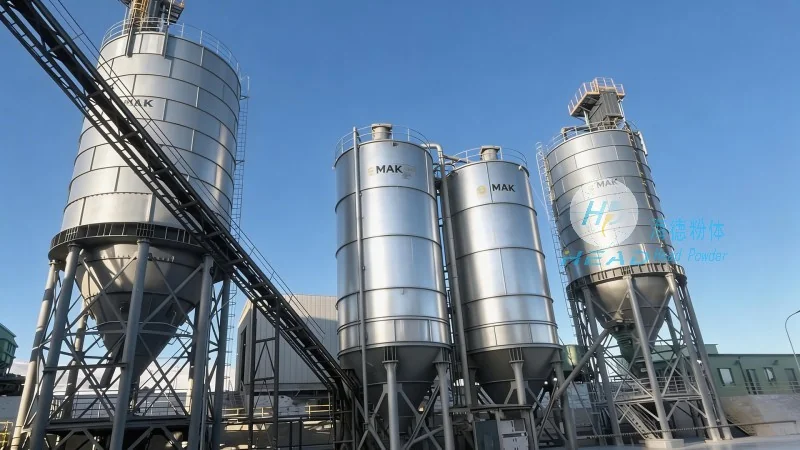
The blower or air compressor is the power source of the pneumatic conveying system, responsible for generating the air flow that propels the corn feed particles. The choice of blower type (e.g., centrifugal, rotary lobe) depends on the specific application requirements, such as the particle size, moisture content, and material flow rate. The blower must be capable of delivering sufficient air volume and pressure to overcome the resistance of the pipeline and the weight of the corn feed particles. Proper maintenance and sizing of the blower are essential to ensure consistent performance and prevent system downtime.
The feeder and hopper are critical components for controlling the flow of corn feed into the conveying system. The hopper is designed to store a sufficient quantity of corn feed, ensuring a steady supply to the feeder. The feeder, often a rotary valve or a screw feeder, regulates the material flow rate into the pipeline, preventing overloading and maintaining consistent air pressure. The design of the hopper and feeder must consider the bulk density and flow characteristics of corn feed to avoid bridging or segregation, which can lead to uneven material flow and system inefficiencies.
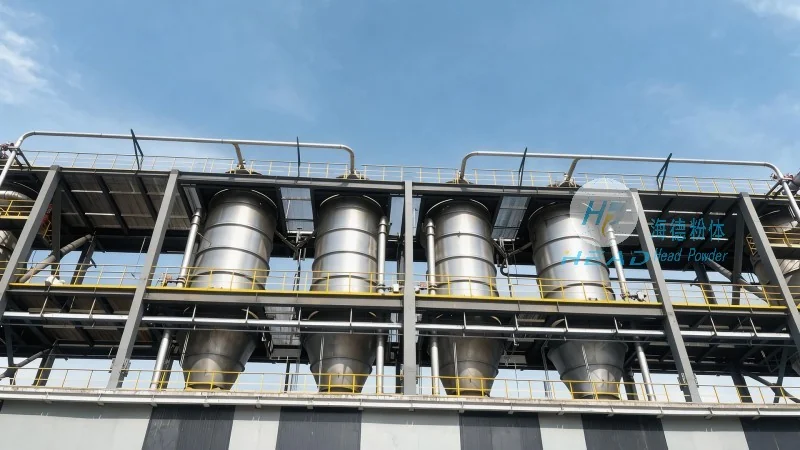
As corn feed is conveyed through the pipeline, fine particles and dust can be entrained in the air stream. The separation and filtration system is responsible for removing these particles from the air, preventing contamination of the feed and protecting the blower and other components from wear and damage. The system typically includes a cyclone separator or a bag filter, which uses centrifugal force or filtration media to capture the particles. The collected material is then returned to the hopper for re-conveying, while the clean air is discharged back into the environment or recirculated through the system.
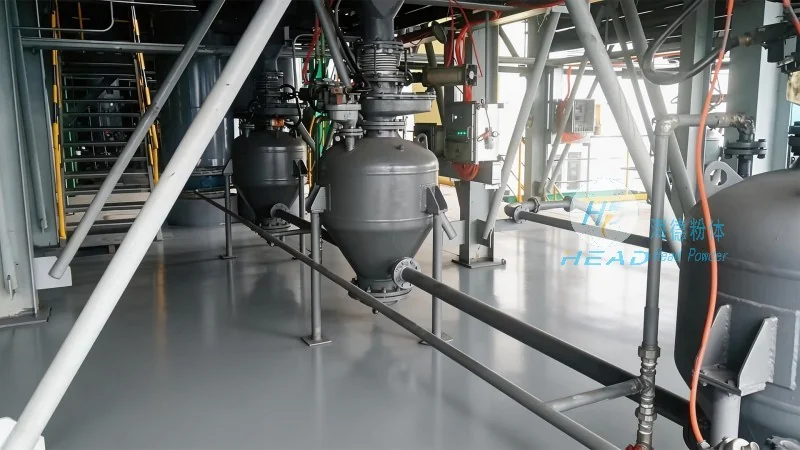
Corn feed pneumatic conveying systems are widely utilized in the animal feed industry for various applications, including the transport of raw corn feed from storage silos to processing facilities, the transfer of finished feed to packaging lines, and the handling of feed additives. The benefits of employing pneumatic conveying systems for corn feed include improved product quality through reduced dust and contamination, increased efficiency through automated material handling, and lower labor costs due to minimal manual intervention required. Additionally, the system can be easily integrated with other processing equipment, such as mixers and grinders, to form a complete feed production line.
Corn feed pneumatic conveying equipment is a sophisticated system that integrates mechanical and pneumatic principles to efficiently transport bulk corn feed. The structure and operational principles of the system, including the conveying pipeline, blower, feeder, and separation system, are carefully designed to ensure optimal performance and product integrity. By understanding the key components and their functions, users can select and operate a suitable pneumatic conveying system for their corn feed handling needs, thereby enhancing productivity and maintaining the quality of animal feed.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top