

Analysis of Sand Particle Pneumatic Conveying Systems
HeadPowder, a prominent engineering enterprise headquartered in Shandong, China, specializes in the development and deployment of advanced pneumatic conveying systems tailored for the transport of sand particles. These systems represent a pivotal technology for industries that demand efficient, reliable, and low-maintenance material handling solutions, especially in contexts where conventional mechanical conveying methods may be inadequate or impractical.

Exploring Pneumatic Conveying for Sand Particles
Pneumatic conveying systems operate by utilizing air or gas to move bulk materials, such as sand particles, through a pipeline network. This approach offers distinct advantages over traditional methods, including reduced equipment wear, lower maintenance requirements, and the ability to maintain a dust-free environment during material transport. The technology is particularly beneficial for applications that require seamless integration with other industrial processes, such as in construction, mining, and manufacturing sectors where sand is a critical raw material.
Key Components of a Sand Particle Pneumatic Conveying System
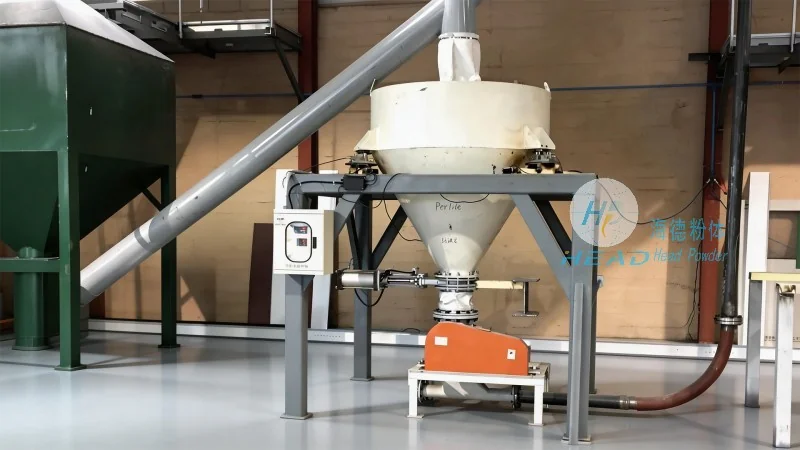
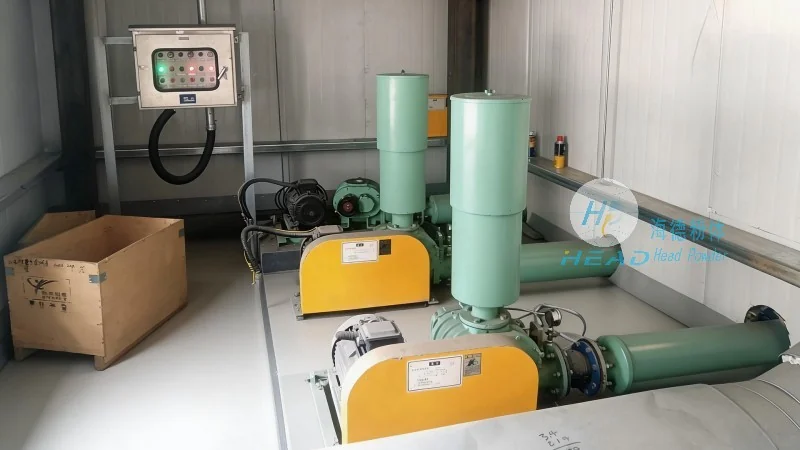
The foundation of a pneumatic conveying system for sand particles consists of several interdependent components that work together to ensure efficient material transport. These components include the feed hopper, which stores and meters the sand; the conveyor line, typically a pipeline where air and sand are mixed and propelled; the air supply system, which generates the necessary pressure or vacuum to drive the material; and the control system, which regulates flow and pressure to maintain optimal operation. Each component is engineered to accommodate the specific characteristics of sand particles, such as their size distribution, density, and flowability, ensuring consistent and reliable performance.
Benefits of Implementing Pneumatic Conveying for Sand Handling
Adopting a pneumatic conveying system for sand particles yields significant advantages for industrial operations. Firstly, it minimizes the risk of material contamination and dust exposure, which is essential for preserving product quality and ensuring worker safety. Secondly, the system reduces the need for manual labor, thereby enhancing operational efficiency and lowering labor costs. Thirdly, the technology is highly adaptable, allowing for integration with existing infrastructure and enabling the transport of materials over extended distances without intermediate storage or transfer points. Additionally, pneumatic conveying systems can handle a wide spectrum of sand types, from fine to coarse particles, making them versatile for diverse applications.
Customization and Scalability in Pneumatic Conveying Solutions
HeadPowder understands that each industrial application has unique requirements, and thus, their pneumatic conveying systems are highly customizable to meet specific operational needs. The company offers tailored solutions that can be scaled to accommodate varying production volumes and material handling demands. Whether a facility requires a small-scale system for laboratory use or a large-scale system for bulk material transport, HeadPowder’s engineering team can design a solution that optimizes performance and cost-effectiveness. The customization process involves a thorough analysis of material properties, operational parameters, and site constraints to ensure the final system complies with all performance and safety standards.
Installation and Maintenance Best Practices
The successful deployment of a sand particle pneumatic conveying system requires meticulous planning and professional installation. HeadPowder’s skilled technicians ensure that all components are properly installed and integrated, adhering to industry best practices and safety regulations. Regular maintenance is also crucial for sustaining the system’s efficiency and longevity. The company provides comprehensive maintenance services, including routine inspections, component replacement, and performance monitoring, to ensure the system operates at peak efficiency. By following a proactive maintenance schedule, industries can minimize downtime and maximize the return on their investment in the pneumatic conveying system.
Real-World Applications and Case Studies
HeadPowder has successfully implemented pneumatic conveying systems for sand particles across various industries, showcasing the technology’s effectiveness in practical settings. For instance, in a construction materials plant, the system was utilized to transport sand from storage silos to mixing facilities, improving material flow and reducing manual handling. In another scenario, a mining operation employed the system to transport sand from processing equipment to storage areas, enhancing operational efficiency and safety. These case studies underscore the versatility and reliability of pneumatic conveying systems in handling sand particles, making them an ideal choice for industries seeking to optimize their material handling processes.