With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications requiring efficient and reliable transport of magnesium sulfate heptahydrate, the air-driven conveying system offers a robust solution. This system is engineered to handle the unique characteristics of this chemical, ensuring safe and effective material movement from storage to processing units. The technology leverages pneumatic principles to achieve seamless operation, minimizing downtime and operational costs.
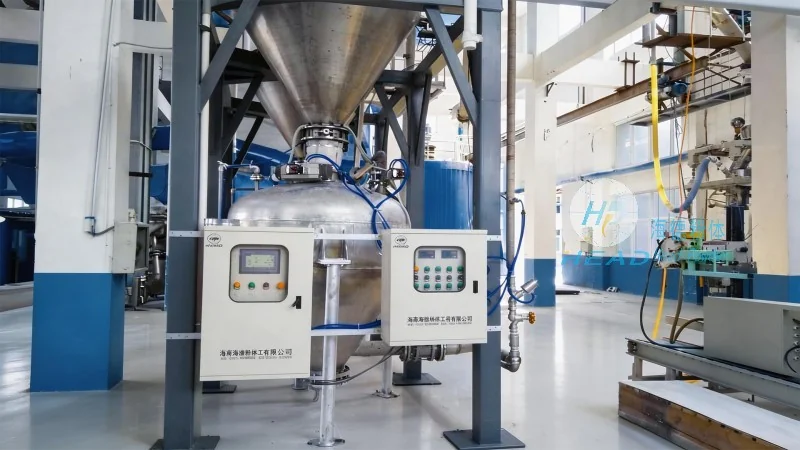
The air-driven magnesium sulfate heptahydrate conveying system comprises several critical components that work in tandem to ensure optimal performance. At the core is the material hopper, which stores the bulk magnesium sulfate heptahydrate. This hopper is equipped with a feeding mechanism that regulates the flow of material into the conveying line. The conveying line itself is typically made of durable, corrosion-resistant materials to withstand the chemical properties of magnesium sulfate heptahydrate. A series of airlocks and valves are integrated to control the flow direction and prevent backflow, maintaining system integrity. The system also includes a dust collection unit to manage any airborne particles, ensuring compliance with environmental regulations and workplace safety standards.
The air-driven conveying system operates by utilizing compressed air to transport the magnesium sulfate heptahydrate particles through the conveying line. As material enters the hopper, it is fed into the line under controlled pressure. The compressed air creates a positive pressure environment, propelling the material forward. This pneumatic transport method is particularly effective for handling fine or powdery materials like magnesium sulfate heptahydrate, as it minimizes material degradation and loss. The system's design allows for adjustable air pressure and flow rates, enabling operators to optimize performance based on the specific requirements of the application. This flexibility ensures that the system can adapt to varying production volumes and process conditions, enhancing overall operational efficiency.
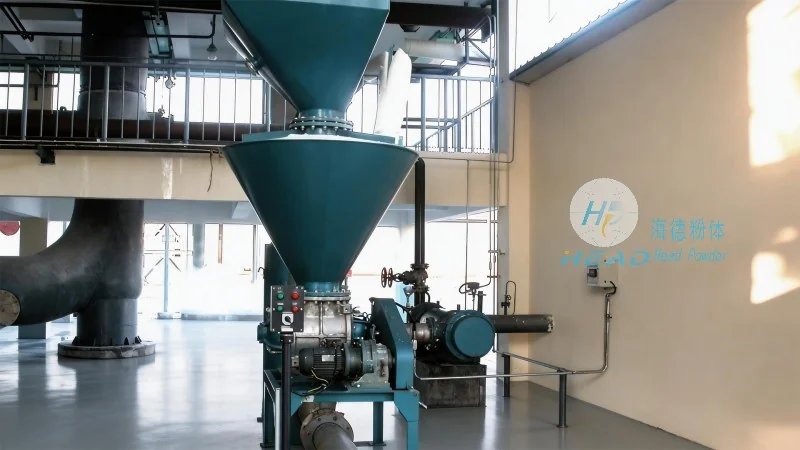
Implementing an air-driven magnesium sulfate heptahydrate conveying system provides several key advantages for industrial operations. First, it offers a dust-free and enclosed transport solution, reducing the risk of material contamination and improving workplace safety. Unlike traditional belt or bucket elevators, the pneumatic system eliminates the need for open-air handling, which is especially beneficial for handling hygroscopic or reactive materials like magnesium sulfate heptahydrate. Second, the system is highly flexible in terms of layout and installation. It can be configured to follow existing facility layouts, minimizing the need for extensive structural modifications. This adaptability reduces installation time and costs, making it a cost-effective solution for both new and existing facilities. Third, the air-driven system provides consistent and reliable material flow, reducing the likelihood of blockages or clogs that can occur with other conveying methods. The positive pressure design ensures that material moves continuously through the system, maintaining a steady supply to downstream processing units. Additionally, the system's low maintenance requirements contribute to long-term operational cost savings, as fewer moving parts and less wear and tear are involved compared to mechanical conveying systems.
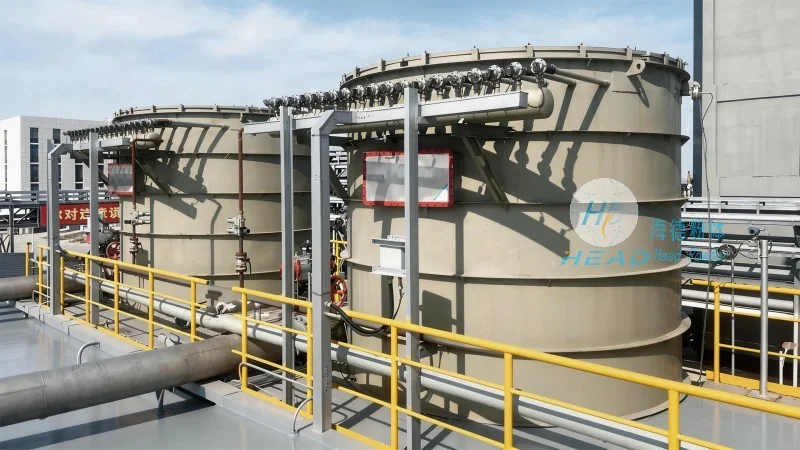
The air-driven magnesium sulfate heptahydrate conveying system is widely applicable across various industrial sectors, including chemical manufacturing, pharmaceuticals, and food processing. In chemical plants, it is commonly used to transport magnesium sulfate heptahydrate from storage silos to reaction vessels or packaging lines. The system's ability to handle bulk quantities efficiently supports high production throughput, making it ideal for large-scale operations. In pharmaceutical applications, the enclosed and dust-free nature of the system is crucial for maintaining product purity and meeting stringent quality control standards. The system's design can be customized to meet cGMP (current Good Manufacturing Practices) requirements, ensuring compliance with regulatory guidelines. Similarly, in food processing facilities, the system's hygienic design and ability to prevent cross-contamination make it suitable for handling food-grade magnesium sulfate heptahydrate used as a food additive. The integration of the system with existing production lines is straightforward, as it can be connected to existing storage and processing equipment with minimal modifications. This compatibility ensures a smooth transition and minimal disruption to ongoing operations.
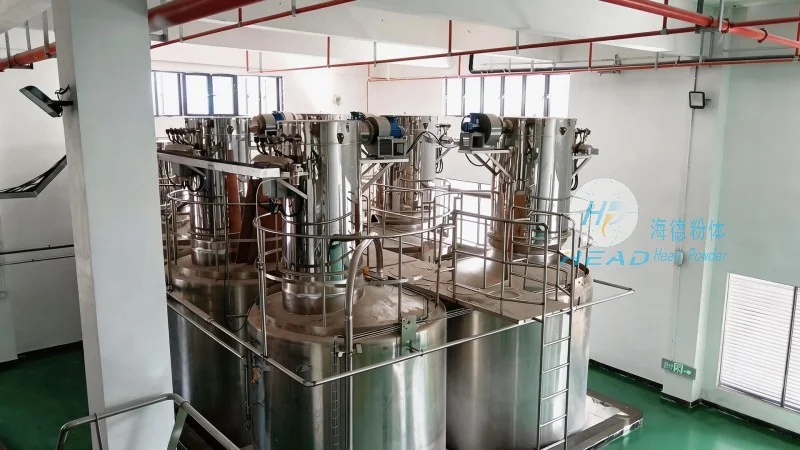
Shandong HeadPowder Engineering Co., Ltd. offers tailored solutions for the air-driven magnesium sulfate heptahydrate conveying system, ensuring that each installation meets the specific needs of the client. The company provides customization options for various parameters, including conveying capacity, air pressure, and system layout. Clients can specify the desired throughput rate, which ranges from low to high volumes, depending on their production requirements. The system can be scaled up or down to accommodate changes in production capacity, making it a flexible investment for growing businesses. Additionally, the company offers options for material handling accessories, such as agitators or mixers, to enhance the system's functionality. These accessories can be integrated to improve material flow or prevent agglomeration, ensuring consistent performance. The customization process involves detailed consultation with the client to understand their operational requirements and constraints. This collaborative approach ensures that the final system design is optimized for efficiency, reliability, and cost-effectiveness.
The installation of the air-driven magnesium sulfate heptahydrate conveying system requires careful planning and execution to ensure optimal performance. The system is typically installed in a pre-defined layout that considers the position of the material hopper, conveying line, and receiving equipment. Proper alignment of the components is crucial to prevent material blockages and ensure smooth operation. The installation process involves connecting the hopper to the conveying line, integrating the airlocks and valves, and connecting the dust collection unit. The system is then pressure-tested to verify that all components are functioning correctly and that there are no leaks. Maintenance of the air-driven system is relatively straightforward, with regular checks on air pressure, filter cleanliness, and material flow. The air filters need to be replaced periodically to maintain efficient air flow and prevent dust accumulation. The material hopper and conveying line should be inspected for signs of wear or corrosion, particularly in areas exposed to the chemical properties of magnesium sulfate heptahydrate. The airlocks and valves should be lubricated as needed to ensure smooth operation. By following a regular maintenance schedule, the system can achieve long operational life and minimal downtime. Shandong HeadPowder Engineering Co., Ltd. provides maintenance services and spare parts to support clients in keeping their systems in optimal condition.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top