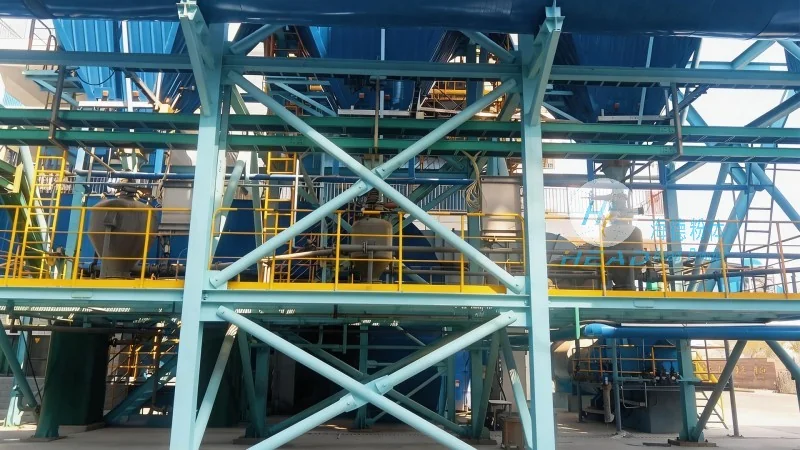
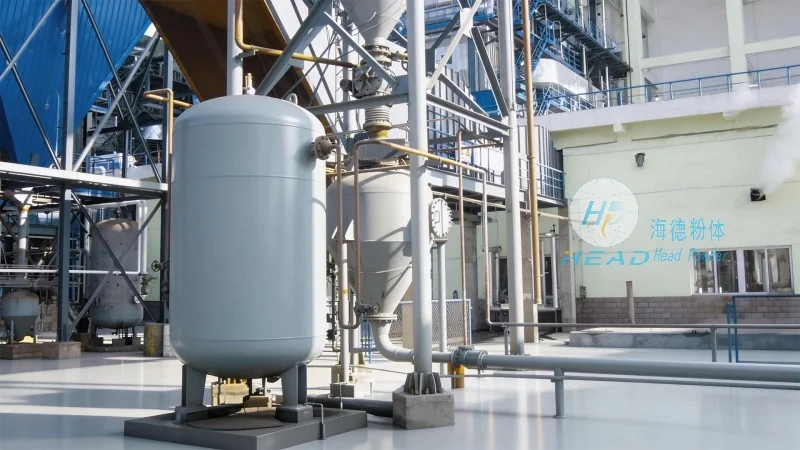
With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The dairy industry is a critical sector that demands the highest standards of hygiene, efficiency, and reliability. When processing and transporting milk powder, manufacturers face unique challenges related to dust control, cross-contamination prevention, and maintaining the integrity of the product. To address these challenges, modern facilities are increasingly turning to automated systems. A robust **powder milk conveying system** is essential for moving bulk quantities of powder safely and efficiently from storage silos to packaging lines or blending tanks. This technology not only minimizes manual labor but also ensures that the product remains uncontaminated throughout the process.
Every dairy processing plant has unique spatial constraints, production capacities, and product characteristics. Therefore, a one-size-fits-all approach is rarely effective. This is where **powder milk pneumatic conveying solution customization** becomes vital. A tailored solution is designed to fit the specific layout of the facility, accommodating the type of milk powder being handled—whether it is whole milk, skim milk, or specialized formula. Customization involves analyzing the flow properties of the powder, such as bulk density and angle of repose, to determine the optimal conveying parameters. By working with experienced engineers, manufacturers can ensure that the system integrates seamlessly with existing equipment, optimizing the workflow and reducing operational bottlenecks.
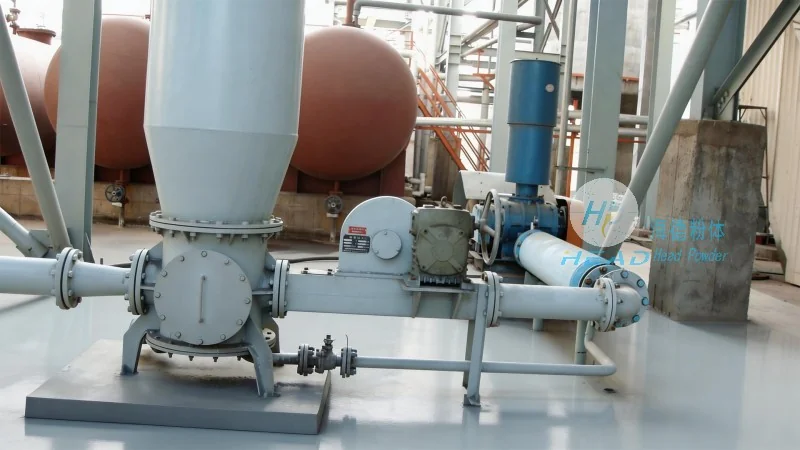
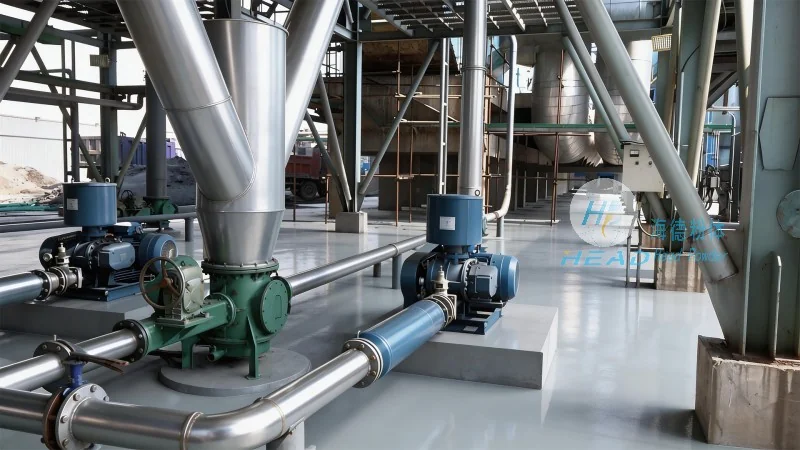
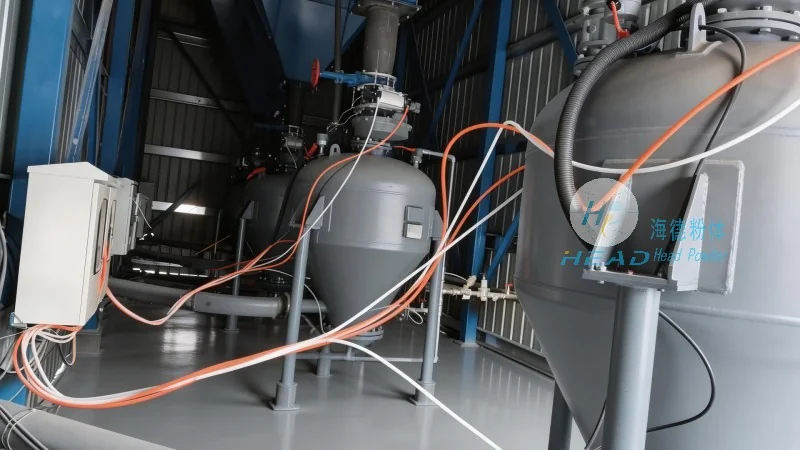
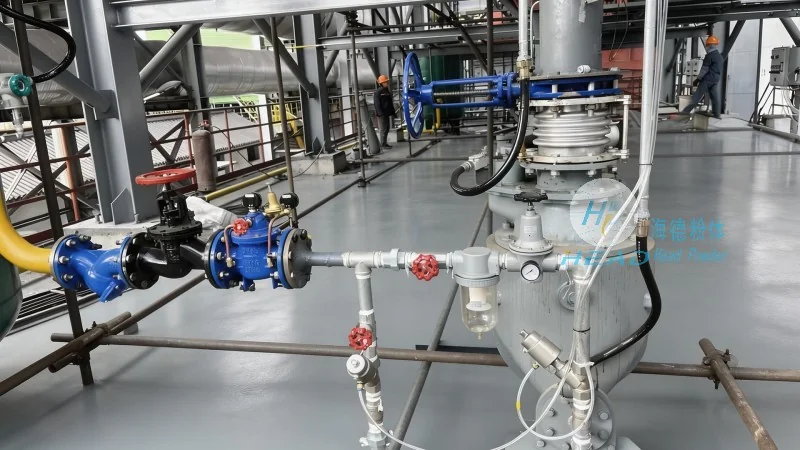
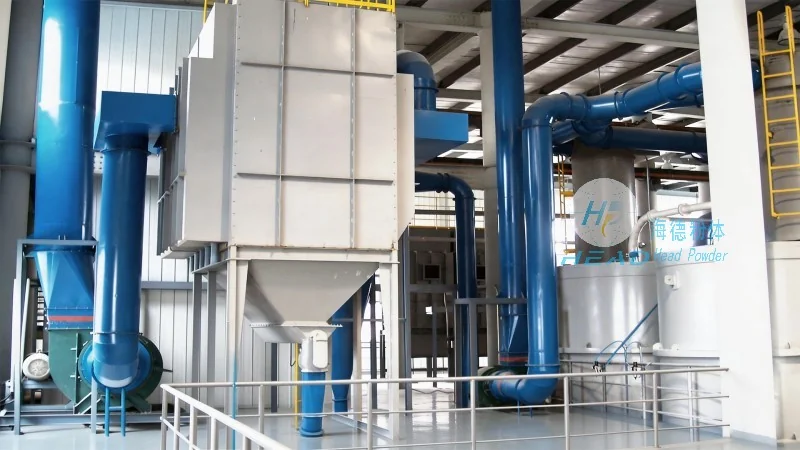
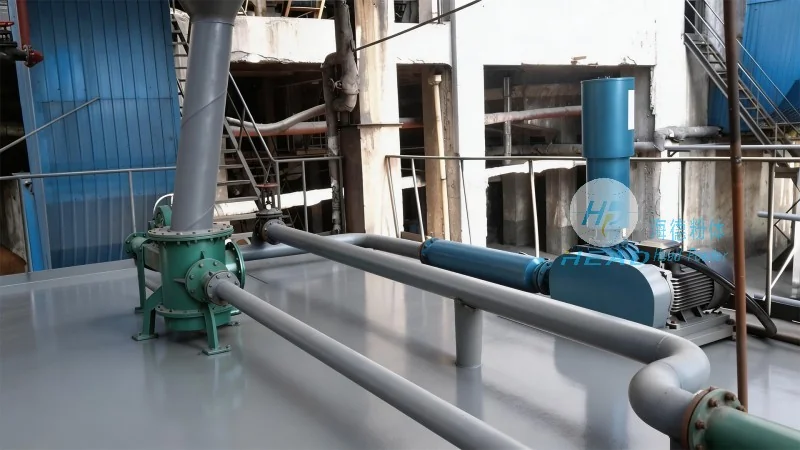
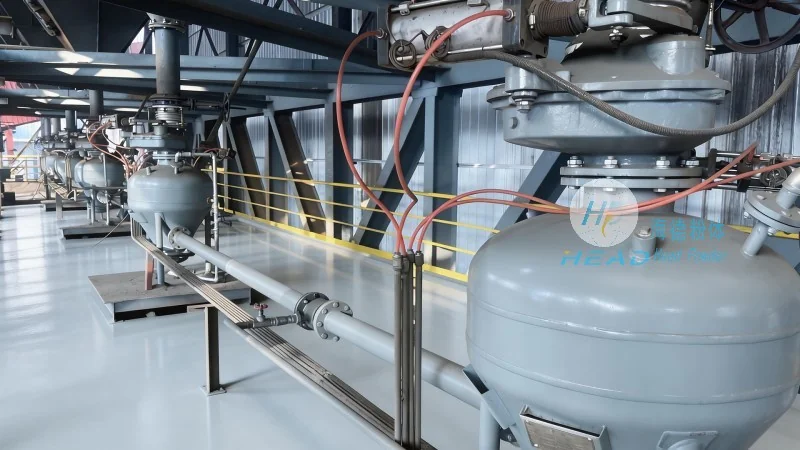
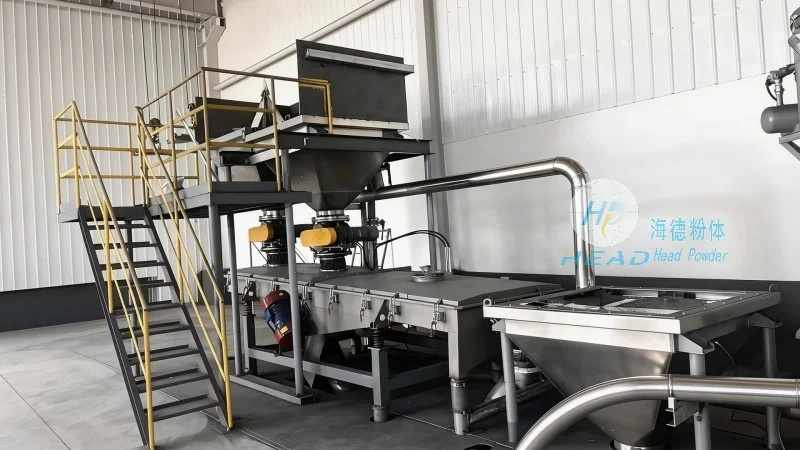
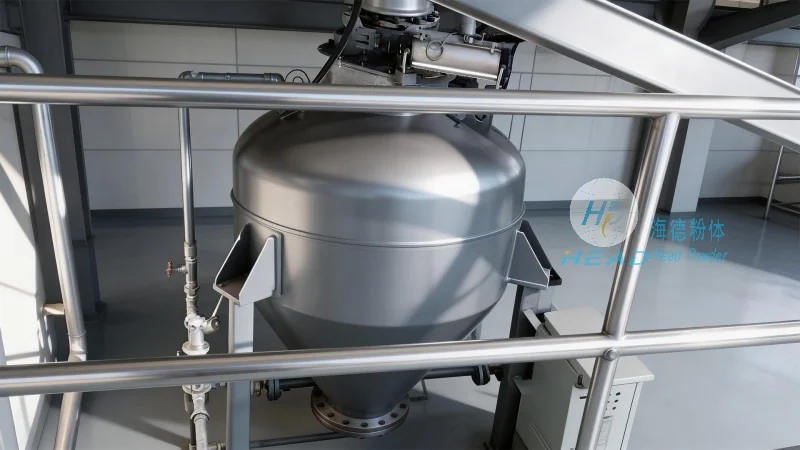
The core of any efficient transport method lies in the quality of the **powder milk conveying system equipment**. High-grade materials and precision engineering are non-negotiable in the food industry. Leading manufacturers utilize food-grade stainless steel, typically 304 or 316L, for all contact parts to ensure compliance with strict sanitary standards. Key components of this equipment include specialized rotary valves, airlocks, and pneumatic conveying lines that are designed to prevent backflow and ensure airtight operations. Additionally, advanced filtration systems are integrated into the equipment to capture fine dust particles, protecting both the product and the environment. The reliability of this machinery directly impacts the uptime of the production line, making equipment quality a top priority.
Choosing the right partner is crucial for the success of a conveying project. A professional **powder milk pneumatic conveying manufacturer** brings years of technical knowledge and industry experience to the table. This expertise is reflected in the design and performance of the systems provided. A reputable manufacturer does not just sell hardware; they provide comprehensive engineering support, from the initial conceptual design to the final installation and commissioning. They understand the nuances of pneumatic transport, such as the differences between dilute-phase and dense-phase conveying, and can recommend the most energy-efficient method for specific applications. This level of expertise ensures that the system will perform reliably under varying operational conditions.
Developing a successful project requires a detailed **powder milk pneumatic conveying scheme**. This scheme serves as the blueprint for the entire installation, detailing the layout of pipes, the placement of vacuum pumps or blowers, and the configuration of the receiving stations. A well-structured scheme takes into account the distance the powder needs to travel, the elevation changes, and the specific requirements of the destination equipment. It also includes safety protocols, such as explosion-proof measures, which are critical when handling combustible powders. By meticulously planning every aspect of the scheme, engineers can prevent common issues such as blockages, excessive wear on pipes, or inconsistent feeding rates.
Implementing a state-of-the-art **powder milk conveying system** offers significant advantages in terms of operational efficiency and safety. Pneumatic conveying is a closed-loop process, which drastically reduces the risk of external contamination and significantly lowers the amount of dust emitted into the workplace. This is not only better for worker health but also complies with environmental regulations. Furthermore, automated systems reduce the reliance on manual handling, which can lead to errors and physical strain on employees. The ability to control the flow of powder remotely allows for precise adjustments to production speeds, ensuring that the packaging and filling operations run smoothly without interruption.
Shandong Headpowder Engineering Co., Ltd. stands at the forefront of providing these advanced solutions. As a dedicated provider of **powder milk pneumatic conveying solution customization**, the company focuses on delivering systems that are tailored to the specific needs of the dairy sector. Their commitment to quality is evident in every project, from the initial consultation to the final handover. By leveraging cutting-edge technology and adhering to rigorous quality control standards, Headpowder ensures that every system meets the highest industry benchmarks.
For those interested in upgrading their production line or designing a new facility, direct communication with the engineering team is the first step towards a successful implementation. To discuss specific requirements and obtain a detailed proposal, please contact **Manager Zhang** at the company's headquarters in Shandong, China. **Manager Zhang** is available to provide expert guidance and answer any questions regarding system design and equipment selection. For more information, please reach out via WeChat at 15662777102. Shandong Headpowder Engineering Co., Ltd. is ready to assist in creating a more efficient and sanitary future for powder milk processing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top