With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
In the realm of industrial material handling, the transportation of fine powders presents unique challenges that require specialized engineering solutions. A prime example of this is the recent project undertaken by Shandong Headpowder Engineering Co., Ltd. in Calgary, Canada. This initiative highlights the critical importance of reliable and efficient material transport systems in North American industrial settings. The project focused on the pneumatic conveying of pulverized coal ash, a byproduct that demands precision and care during handling. By deploying a state-of-the-art system, the team ensured that the material was moved from the source to the destination with minimal loss and maximum efficiency, setting a new standard for industrial operations in the region. This case study serves as a testament to the capabilities of advanced engineering in managing difficult materials.
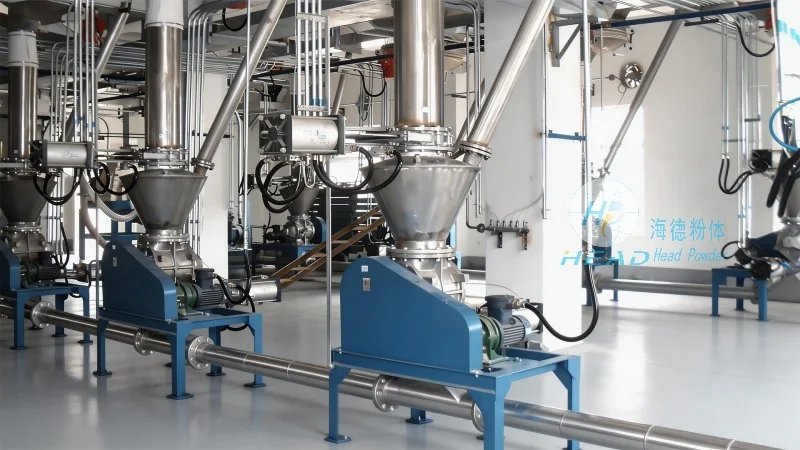
Pulverized coal ash, often referred to as fly ash, is a fine, powdery substance that is generated as a byproduct of burning pulverized coal in thermal power plants. In an industrial environment like Calgary, managing this material is not merely a logistical task but a critical operational requirement. The fine particulate nature of fly ash poses significant risks, including dust explosions, environmental contamination, and equipment wear. Traditional methods of transport, such as belt conveyors or manual scooping, often fail to address these risks effectively. Dust emissions can lead to regulatory fines and health hazards for workers, while the abrasive nature of the ash can degrade mechanical components over time. Therefore, the challenge was to develop a solution that could handle the material safely, maintain a clean working environment, and ensure the longevity of the equipment.
To address these challenges, the project implemented a sophisticated closed-system pneumatic conveying solution. This technology is a cornerstone of modern material handling and is specifically designed to transport dry bulk materials like pulverized coal ash through a pipeline using compressed air or a vacuum. The system operates by creating a pressure differential that moves the material through the pipeline from the receiving point to the storage or processing area. Unlike open conveyors, this method completely isolates the material from the external environment. This closed-loop design is essential for maintaining air quality and preventing dust pollution, making it an ideal choice for urban and industrial environments alike. The system's ability to handle high volumes of material with consistent flow rates makes it a superior alternative to mechanical conveying methods.
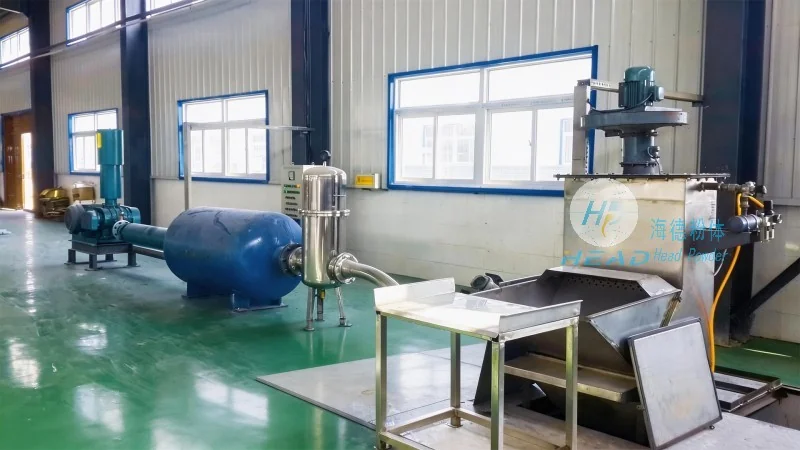
Shandong Headpowder Engineering Co., Ltd. has established itself as a premier provider of pneumatic conveying systems, with a growing portfolio of successful projects across the globe. The company's expertise in this field is rooted in deep technical knowledge and years of practical experience. As a company based in Shandong, China, Headpowder combines manufacturing precision with engineering innovation to deliver solutions that meet international standards. The Calgary project is a clear illustration of the company's ability to adapt its technology to the specific needs of the North American market. By focusing on quality materials and rigorous testing, Headpowder ensures that every system installed is robust, reliable, and capable of withstanding the demands of heavy industrial use. Their commitment to excellence has made them a trusted partner for businesses looking to optimize their material handling processes.
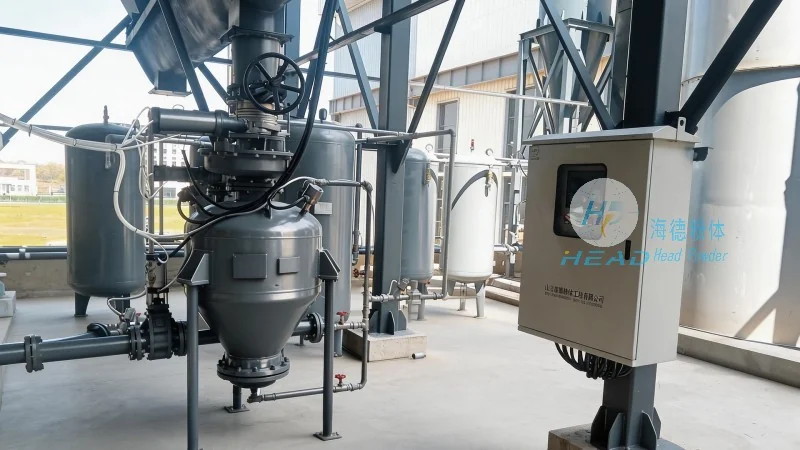
The pneumatic conveying system installed in Calgary offers numerous technical advantages that contribute to the overall efficiency of the facility. One of the primary benefits is the reduction of material loss. Because the system is fully enclosed, there is virtually no spillage or leakage during the transportation process. This not only preserves the material but also reduces the need for costly cleanup and maintenance. Additionally, the system is highly energy-efficient, utilizing advanced control systems to optimize air pressure and flow rates. This ensures that the energy consumption is kept to a minimum while still maintaining high throughput. The automation of the process also reduces the need for manual intervention, thereby lowering labor costs and minimizing the risk of human error. Furthermore, the system is designed to be easily expandable, allowing the facility to increase its production capacity in the future without significant infrastructure changes.

Environmental sustainability and workplace safety are paramount in the design of the Headpowder pneumatic conveying system. The closed-system design effectively eliminates dust emissions, ensuring compliance with strict environmental regulations. This is particularly important in regions like Calgary, where air quality standards are rigorously enforced. By preventing dust from escaping into the atmosphere, the system protects the surrounding ecosystem and reduces the carbon footprint of the facility. Safety is also a top priority; the system is equipped with multiple safety sensors and emergency stop mechanisms to prevent accidents. The absence of moving parts in the pipeline reduces the risk of mechanical injuries, creating a safer work environment for operators. This holistic approach to design ensures that the facility not only operates efficiently but also does so in a manner that is responsible and sustainable.
For companies in North America and beyond looking to upgrade their material handling infrastructure, Shandong Headpowder Engineering Co., Ltd. offers the expertise and technology needed to succeed. The team is dedicated to providing customized solutions that address the unique challenges of each project. To discuss your specific requirements or to learn more about how a pneumatic conveying system can benefit your operations, please contact our project manager, Mr. Zhang. You can reach him directly via WeChat at 15662777102. Mr. Zhang and his team are ready to provide the technical support and guidance necessary to bring your project to fruition.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top