

Working Principle and Features of Flower Bio-organic Fertilizer Conveying Equipment
Flower bio-organic fertilizer conveying equipment plays a crucial role in the modern agricultural and horticultural sectors, facilitating the efficient transport of organic materials used in flower cultivation. Understanding its working principle and key features is essential for optimizing operational efficiency and ensuring the quality of the final fertilizer product.
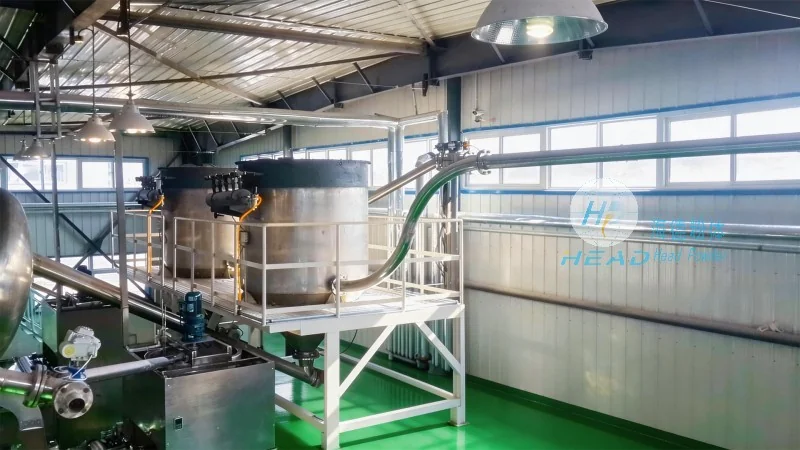
Working Principle of Flower Bio-organic Fertilizer Conveying Equipment
The operation of flower bio-organic fertilizer conveying equipment typically involves several integrated components working in tandem to process and transport organic matter. The process begins with the intake of raw materials, such as composted organic waste, which is then fed into a hopper or loading chamber. From there, the material is transferred to a conveyor system, often utilizing screw conveyors, belt conveyors, or pneumatic systems depending on the specific design and material characteristics. The equipment may incorporate mechanisms like rotary valves or feeders to regulate the flow rate, ensuring a consistent and controlled movement of the bio-organic material through the system. Subsequent stages may include mixing or conditioning processes to enhance the uniformity of the fertilizer, followed by the final discharge into storage or packaging units. This systematic approach allows for a seamless and efficient workflow, minimizing downtime and maximizing productivity in the production of flower bio-organic fertilizers.
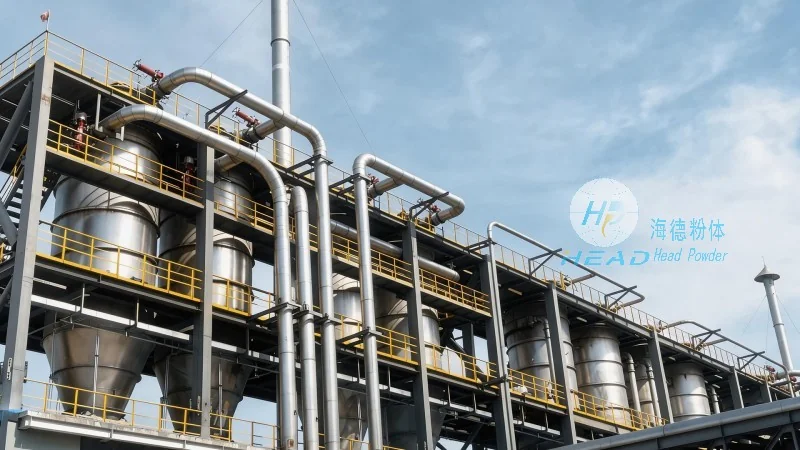
Key Features of Flower Bio-organic Fertilizer Conveying Equipment
HeadPowder, a leading manufacturer based in Shandong, China, offers advanced flower bio-organic fertilizer conveying equipment characterized by several notable features. Firstly, the equipment is designed with durability and low maintenance in mind, utilizing high-quality materials and robust construction to withstand the rigorous demands of continuous operation in agricultural settings. The systems are equipped with user-friendly control panels that allow operators to easily adjust parameters such as speed, flow rate, and material consistency, enhancing operational flexibility. Additionally, the equipment incorporates advanced safety features, including overload protection and emergency stop mechanisms, to ensure safe and reliable operation. Another critical feature is the integration of monitoring systems, which provide real-time data on performance metrics, enabling proactive maintenance and optimizing equipment lifespan. The equipment also prioritizes energy efficiency, employing variable speed drives and optimized conveyor designs to reduce power consumption while maintaining high throughput. These features collectively contribute to improved productivity, reduced operational costs, and enhanced overall performance in the production of high-quality flower bio-organic fertilizers.
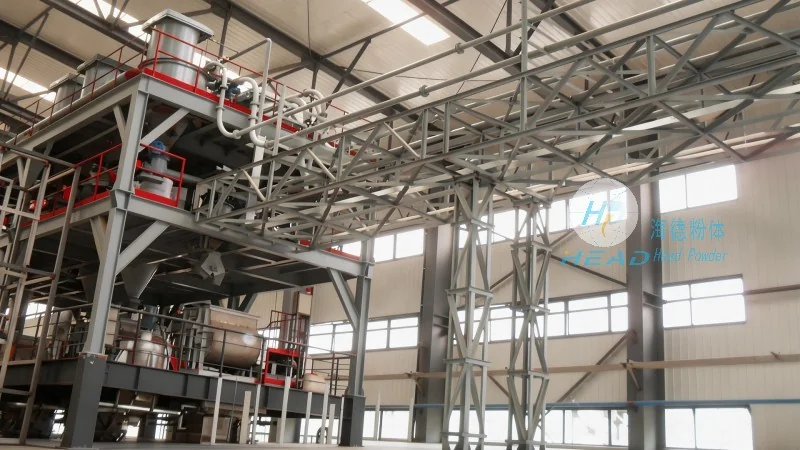
Company Information and Commitment to Quality
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is dedicated to providing innovative and reliable solutions for the agricultural industry. With a strong focus on research and development, the company continuously enhances its product line to meet the evolving needs of modern farming and horticulture. The company’s flower bio-organic fertilizer conveying equipment is engineered to deliver consistent performance, ensuring that farmers and gardeners can rely on efficient and effective fertilizer production processes. By adhering to strict quality standards and employing skilled engineering expertise, HeadPowder ensures that its equipment meets the highest industry benchmarks, supporting sustainable agricultural practices and contributing to the growth of the flower cultivation sector. The company’s commitment to customer satisfaction and technological advancement positions it as a trusted partner for businesses seeking to optimize their fertilizer production operations.