With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For industrial applications involving sulfur pellets, efficient and reliable material handling is crucial. The sulfur pellet pneumatic conveying system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution designed to meet the demands of modern processing facilities. This system integrates advanced engineering principles and robust construction to ensure optimal performance in transporting sulfur pellets with precision and minimal loss.
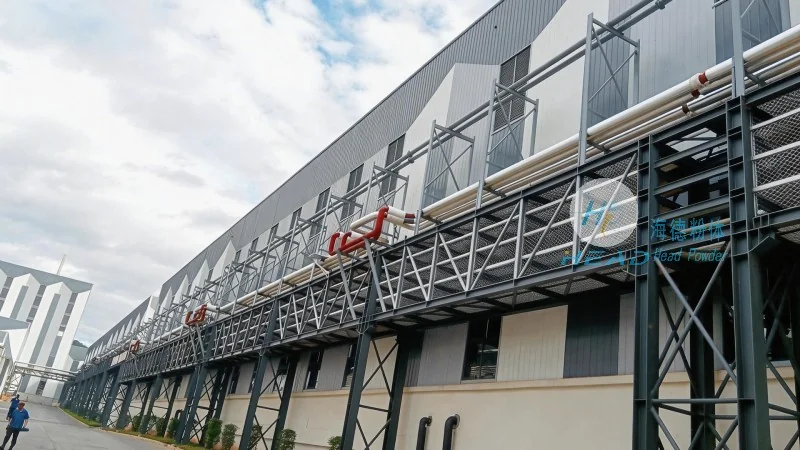
The sulfur pellet pneumatic conveying system is a specialized piece of equipment engineered to transport sulfur pellets through a pressurized or vacuum air stream. HeadPowder, a leading manufacturer in material handling solutions, has designed this system to address the unique challenges associated with handling sulfur pellets, such as their density, size, and potential for dust generation. The system is built to ensure safe, efficient, and cost-effective material transport, making it an essential component for sulfur processing plants.
The pneumatic conveying system for sulfur pellets consists of several critical components, each playing a vital role in the overall operation. The primary components include the hopper, feeder, air compressor or vacuum pump, conveying pipeline, and the receiving hopper. The hopper is designed to store the sulfur pellets and feed them into the system at a controlled rate. The feeder, typically a rotary valve or screw feeder, ensures a consistent flow of pellets into the conveying line. The air compressor or vacuum pump generates the necessary pressure or vacuum to move the pellets through the pipeline. The conveying pipeline, often made of corrosion-resistant materials like stainless steel or special coatings, is designed to withstand the chemical properties of sulfur and prevent material buildup or corrosion. The receiving hopper collects the sulfur pellets at the destination point, completing the transport process.
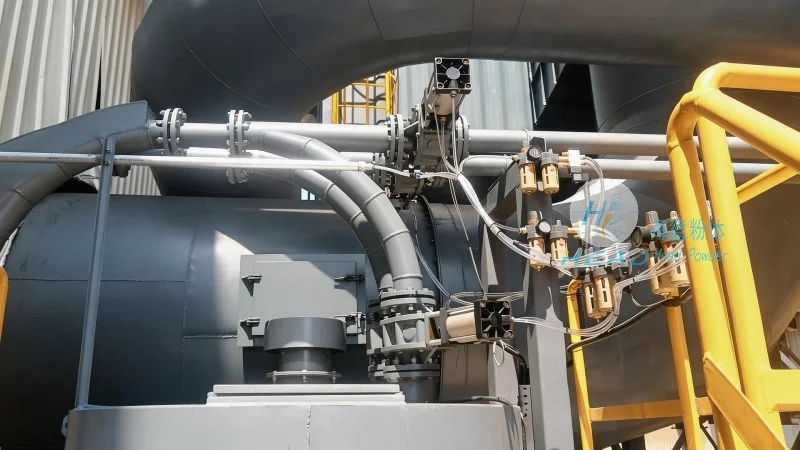
The operation of the sulfur pellet pneumatic conveying system is based on the principles of pneumatic transport, which involves the movement of solid particles suspended in a gas stream. In this system, sulfur pellets are introduced into the hopper and then fed into the conveying pipeline by the feeder. The air compressor or vacuum pump then creates a pressure differential, either by blowing air into the pipeline (positive pressure system) or by creating a vacuum (negative pressure system). This pressure differential propels the sulfur pellets along the pipeline, where they are carried by the air stream. The pellets remain suspended in the air until they reach the receiving hopper, where the air is filtered and the pellets are collected. The system is designed to maintain a consistent flow rate and pressure, ensuring that the sulfur pellets are transported without clogging or degradation.
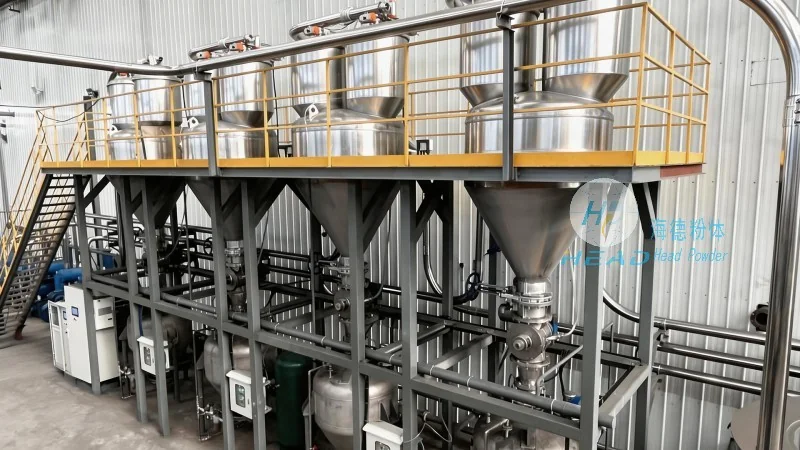
Implementing a sulfur pellet pneumatic conveying system offers several advantages over traditional material handling methods. First, it provides a dust-free and enclosed transport process, reducing the risk of environmental contamination and improving workplace safety. Second, the system minimizes material loss and degradation, as the pellets are not subjected to excessive friction or impact during transport. Third, the system is highly efficient, with lower energy consumption compared to other methods like belt conveyors or bucket elevators. Additionally, the system can be easily integrated into existing processing lines, allowing for seamless material flow and increased productivity. The robust construction and corrosion-resistant materials used in the system ensure long-term reliability and low maintenance costs, making it a cost-effective solution for sulfur processing facilities.
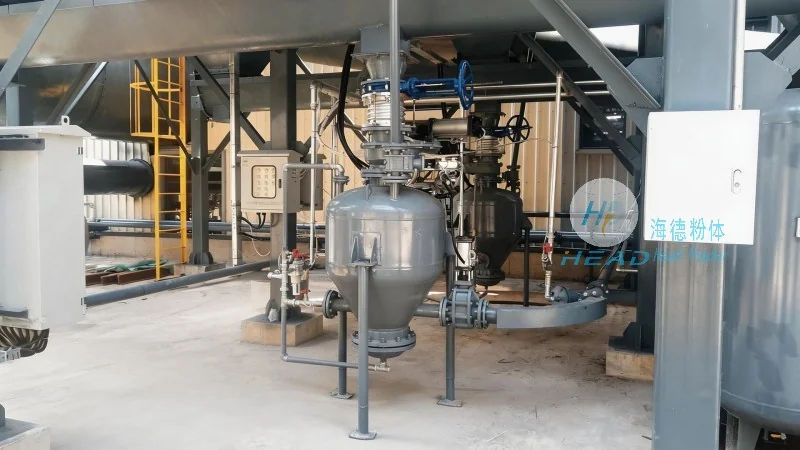
The sulfur pellet pneumatic conveying system is widely used in various industrial applications, particularly in the chemical and fertilizer industries. It is commonly employed in sulfur processing plants to transport sulfur pellets from storage silos to reactors, or from production lines to packaging areas. The system is also used in other industries where sulfur pellets are a key raw material, such as in the production of sulfuric acid or in the manufacturing of sulfur-based fertilizers. The versatility of the system allows it to handle different pellet sizes and densities, making it suitable for a wide range of applications. The system's ability to maintain a consistent flow rate and pressure ensures that the processing lines operate smoothly, reducing downtime and increasing overall productivity.
The sulfur pellet pneumatic conveying system developed by Shandong HeadPowder Engineering Co., Ltd. is a reliable and efficient solution for transporting sulfur pellets in industrial settings. By integrating advanced engineering principles and robust construction, the system ensures optimal performance, safety, and cost-effectiveness. HeadPowder, with its expertise in material handling solutions, provides high-quality equipment and technical support to ensure that clients achieve their processing goals. With its headquarters in Shandong, China, HeadPowder serves clients globally, delivering customized solutions tailored to their specific needs. The company's commitment to quality and innovation has made it a trusted partner in the material handling industry, providing reliable equipment for various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top