With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of high-efficiency pneumatic conveying systems tailored for cement and mineral powders. This article provides a detailed introduction to the structure and working principles of their cement and mineral powder pneumatic conveying equipment, highlighting key components and operational mechanisms that ensure reliable and efficient material transport.
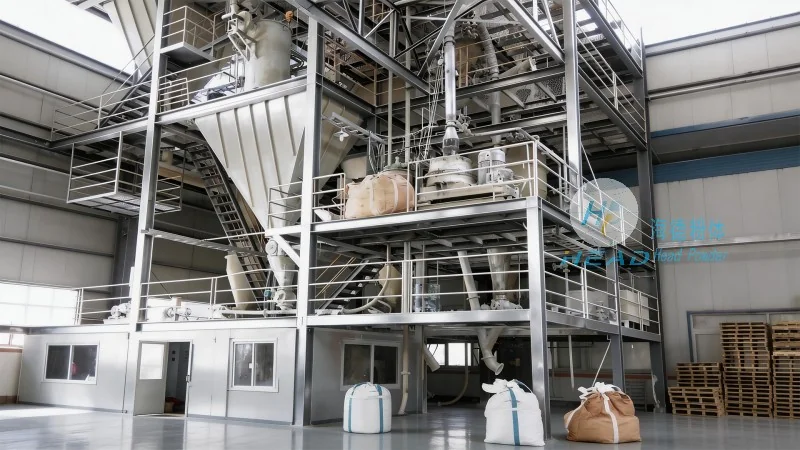
The core components of a pneumatic conveying system for cement and mineral powders typically include a hopper for material storage, a feeder to control the flow rate, a conveying line (often equipped with pressure vessels or vacuum units), and a dust collection system. The hopper is designed to hold the bulk material, ensuring a consistent supply to the feeder. The feeder, which may be a rotary valve or a screw feeder, regulates the material discharge rate, preventing overloading or underloading of the conveying line. The conveying line is the main pathway for transporting the powder, and it can operate under positive pressure (pressure conveying) or negative pressure (vacuum conveying), depending on the system design and application requirements. The dust collection system is crucial for maintaining air quality and preventing material loss, typically consisting of filters and a blower to capture and recycle the powder.
The operation of a cement and mineral powder pneumatic conveying system involves the use of air as the conveying medium. In positive pressure systems, a blower or compressor generates high-pressure air that is introduced into the hopper, lifting the material and pushing it through the conveying line to the discharge point. The air and material mixture travels through the pipeline, with the pressure maintaining the material in suspension. In negative pressure systems, a vacuum pump creates a low-pressure environment at the discharge end, drawing the material and air mixture from the hopper through the line to the collection point. The air flow rate is carefully controlled to ensure that the powder particles remain suspended and do not settle, which is critical for preventing blockages and maintaining system efficiency. The system also includes check valves and pressure relief devices to manage pressure fluctuations and protect the equipment from damage.
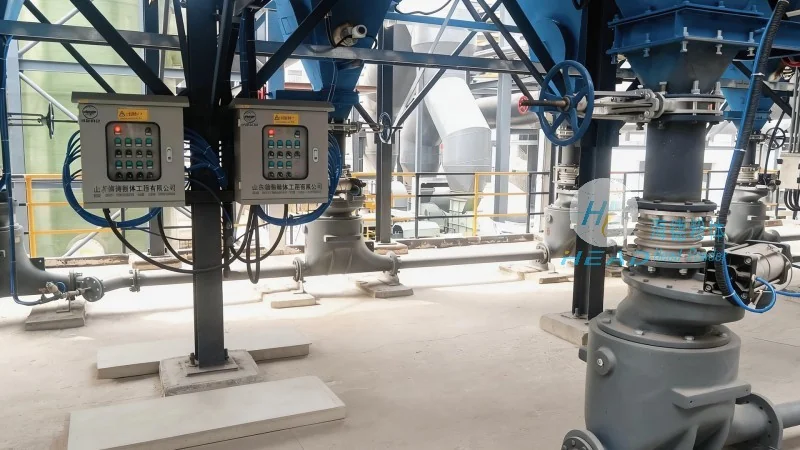
Pneumatic conveying offers several advantages over traditional mechanical conveying methods for cement and mineral powders. It eliminates the need for mechanical components like belts or buckets, reducing maintenance costs and the risk of mechanical failure. The enclosed system prevents dust contamination and environmental pollution, making it suitable for industrial applications where dust control is essential. Additionally, pneumatic conveying allows for flexible system layouts, as the conveying line can be routed around obstacles and in various configurations without the need for complex machinery. The system also provides better control over material flow, enabling precise dosing and preventing material degradation due to friction or exposure to air.
Cement and mineral powder pneumatic conveying equipment is widely used in various industries, including cement production, mining, and chemical processing. In cement plants, it is used to transport raw materials like limestone and clay from storage silos to the grinding mills. In mining operations, it helps in transporting ore and mineral powders from processing facilities to storage or further processing units. The equipment is also utilized in chemical plants for conveying powders such as calcium carbonate and other mineral additives. The versatility of the system makes it suitable for a wide range of applications, from small-scale laboratory use to large-scale industrial production.
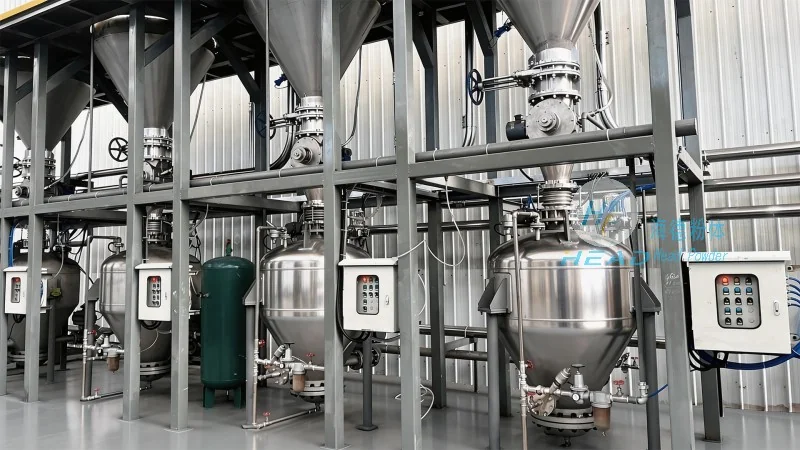
Proper maintenance is essential to ensure the long-term performance and reliability of cement and mineral powder pneumatic conveying systems. Regular inspection of the hopper, feeder, and conveying line for wear and tear is necessary to prevent material buildup and blockages. The dust collection system should be cleaned and maintained regularly to avoid clogging and ensure efficient operation. The air compressor or vacuum pump should be checked for proper functioning, with filters and lubrication maintained as per manufacturer recommendations. Operational considerations include monitoring the air pressure and flow rate to ensure optimal performance, and adjusting the system parameters based on the type and quantity of material being conveyed. Proper training of operators on the system's operation and maintenance is also crucial to prevent accidents and ensure safe and efficient operation.
HeadPowder's cement and mineral powder pneumatic conveying equipment represents a reliable and efficient solution for material transport in various industrial applications. By understanding the key components and working principles of the system, users can make informed decisions about its implementation and maintenance. The advantages of pneumatic conveying, including reduced maintenance, improved dust control, and flexible system design, make it a preferred choice for many industries. With proper operation and maintenance, these systems can provide long-term performance and contribute to increased productivity in material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top