With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Wheat bran, a byproduct of the milling process, is a critical component in various food products and industrial applications. Efficient and reliable material conveying systems are essential for handling wheat bran, ensuring consistent quality and operational efficiency. This article provides a detailed overview of the operation process and working principles of wheat bran material conveying systems, highlighting key components, mechanisms, and best practices for optimal performance.
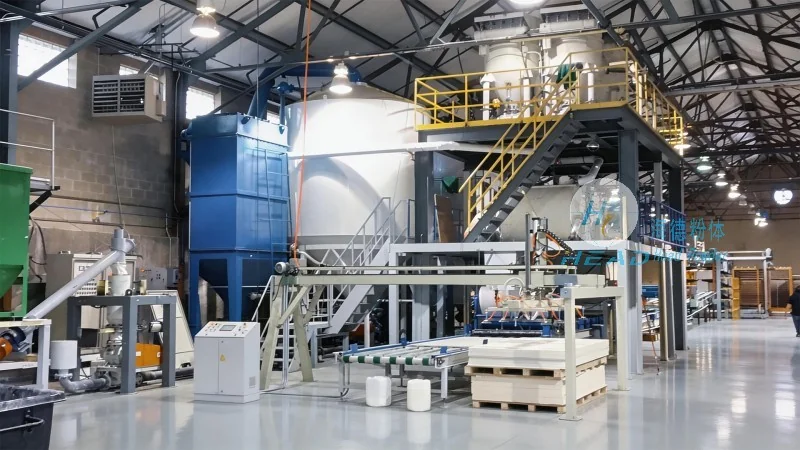
HeadPowder, a leading manufacturer in material handling solutions, specializes in designing and manufacturing advanced conveying systems tailored to the food and agricultural industries. With a strong focus on innovation and quality, the company has established itself as a trusted partner for businesses requiring efficient and hygienic material transport solutions. HeadPowder's expertise lies in understanding the unique challenges of handling wheat bran and similar bulk materials, enabling the development of customized systems that meet stringent industry standards.
The operation of wheat bran material conveying systems involves several critical components that collaborate to ensure smooth material transport. These components include feed hoppers, conveyor mechanisms (such as belt or screw conveyors), drive systems, control panels, and discharge chutes. Each component plays a vital role in the overall functionality. The feed hopper collects and stores the wheat bran, providing a consistent feed to the conveyor. The conveyor itself transports the material along its length, using gravity or rotational force to move the material forward. Drive mechanisms, including electric motors and gearboxes, supply the necessary power to operate the conveyor. Control panels allow operators to monitor and adjust system performance, ensuring optimal operation. Finally, discharge chutes direct the material to its final destination, such as a storage silo or processing unit.
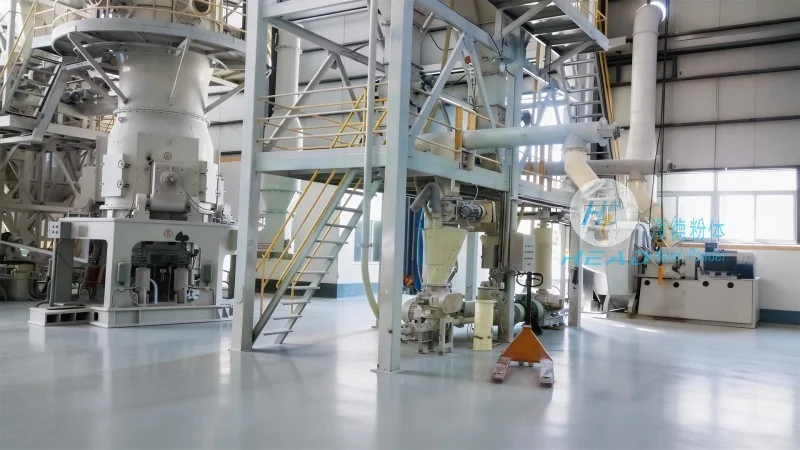
The working principle of wheat bran material conveying systems is based on mechanical transport principles. The system operates by using a conveyor to move wheat bran from the feed point to the discharge point. The feed hopper collects the material and feeds it into the conveyor. The conveyor then transports the material along its length, with the drive mechanism providing the torque to rotate components and ensure continuous movement. The control panel enables operators to adjust speed and direction, while monitoring system performance. This integrated approach ensures efficient and safe material transport, minimizing loss or contamination risks.
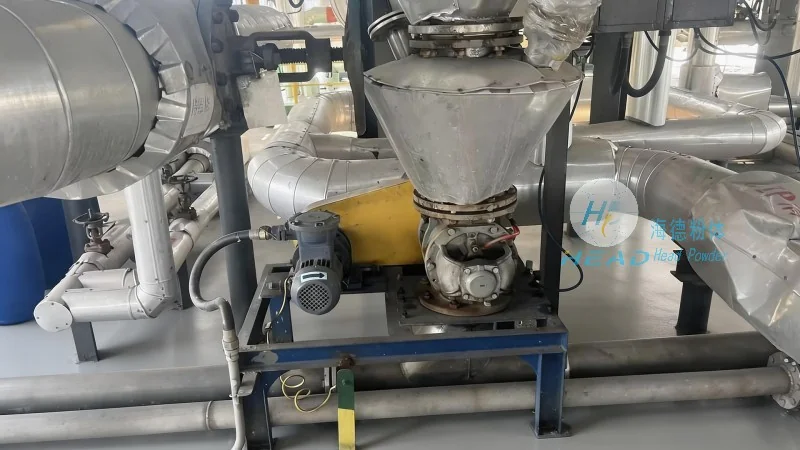
The operation process of wheat bran material conveying systems typically involves several steps for smooth handling. First, the system is prepared by checking component alignment and functionality. Next, the wheat bran is loaded into the feed hopper, ensuring even distribution and no obstructions. The conveyor is then started, with the drive mechanism activated and speed adjusted to the desired level. System performance is monitored, checking discharge rate, material flow, and signs of blockages. Finally, the system is shut down by stopping the conveyor and emptying the hopper and conveyor. This process ensures controlled, efficient material transport, minimizing downtime and maximizing productivity.
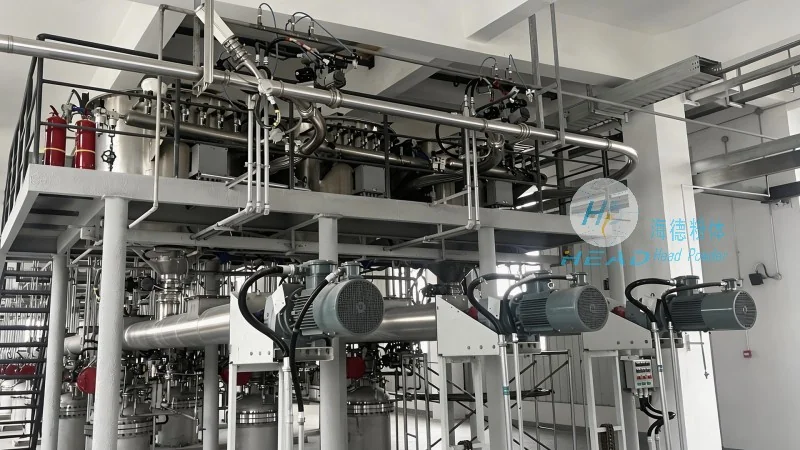
Advanced wheat bran material conveying systems offer significant advantages for businesses in the food and agricultural sectors. These systems enhance efficiency and productivity by reducing labor and time for material handling. They also improve safety by minimizing spills and accidents. Additionally, they help maintain wheat bran quality by preventing contamination and ensuring consistent moisture levels. The use of advanced materials and design features extends equipment lifespan, reducing maintenance costs and downtime. Overall, investing in a high-quality conveying system from a reputable manufacturer like Shandong HeadPowder Engineering Co., Ltd. provides substantial returns through increased efficiency, improved product quality, and reduced operational costs.
In summary, wheat bran material conveying systems are indispensable for efficient handling of this valuable byproduct. The operation process and working principles involve mechanical components and intelligent control systems working in tandem to ensure reliable material transport. By understanding these components and processes, businesses can make informed decisions when selecting and implementing a conveying system that meets their specific needs. With the expertise and commitment to quality from manufacturers like HeadPowder, businesses can achieve optimal performance and productivity in their wheat bran handling operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top