With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Silage material, a critical component in modern agricultural and livestock operations, often requires efficient and reliable transportation methods to ensure optimal handling and processing. Pneumatic conveying systems have emerged as a leading solution for moving bulk powders like silage, offering a versatile and effective approach to material handling. This article explores the principles and applications of pneumatic conveying for silage material, highlighting how advanced systems can enhance operational efficiency and sustainability in agricultural settings.
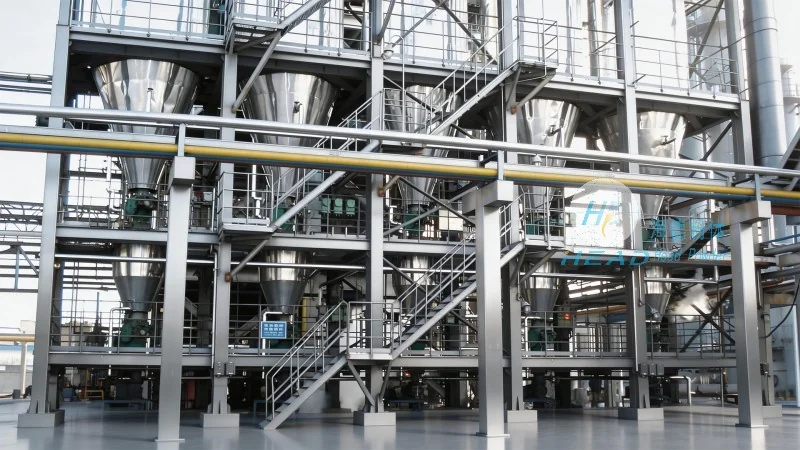
Pneumatic conveying involves the use of air or gas to transport bulk materials through a pipeline system. In the context of silage, this technology is particularly valuable due to the material's characteristics—such as its moisture content, density, and tendency to clump or agglomerate. Traditional methods like belt conveyors or bucket elevators may struggle with these properties, leading to inefficiencies and increased maintenance costs. Pneumatic systems, on the other hand, provide a continuous, low-maintenance solution that minimizes material degradation and loss.
A typical silage pneumatic conveying system consists of several key components, each playing a crucial role in the overall operation. The primary elements include a material feed hopper, a conveying line (often equipped with bends and elbows), a dust collector or filter system, and a discharge outlet. The feed hopper is designed to evenly distribute the silage material into the conveying line, while the line itself is constructed from durable materials like stainless steel to withstand the corrosive and abrasive nature of silage. The dust collector is essential for maintaining air quality and preventing material buildup in the system, ensuring compliance with environmental regulations and operational safety.
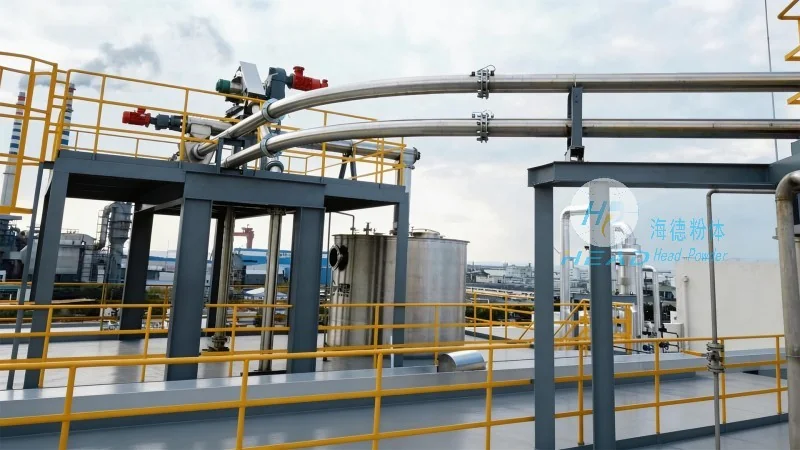
Implementing a pneumatic conveying system for silage material offers numerous advantages that can significantly improve operational performance. One of the most notable benefits is the reduction in material handling time and labor costs. Unlike manual or mechanical methods, pneumatic systems can transport large volumes of silage quickly and continuously, streamlining processes from storage to processing. Additionally, these systems minimize product contamination and degradation, as the material remains enclosed within the pipeline, reducing exposure to external elements and handling errors. Environmental benefits are also significant, as pneumatic conveying reduces dust emissions and energy consumption compared to traditional methods, aligning with sustainable agricultural practices.
The versatility of pneumatic conveying systems makes them suitable for a wide range of silage handling applications. From on-farm storage and processing to industrial-scale silage production, these systems can be customized to meet specific operational needs. For example, in dairy farms, pneumatic conveyors can efficiently move silage from storage silos to feeding stations, ensuring consistent feed quality for livestock. In larger agricultural operations, these systems can integrate with existing infrastructure, such as silos and processing plants, to create a seamless material flow. The ability to adjust conveying speed and pressure allows operators to optimize performance based on material characteristics and demand, further enhancing efficiency.
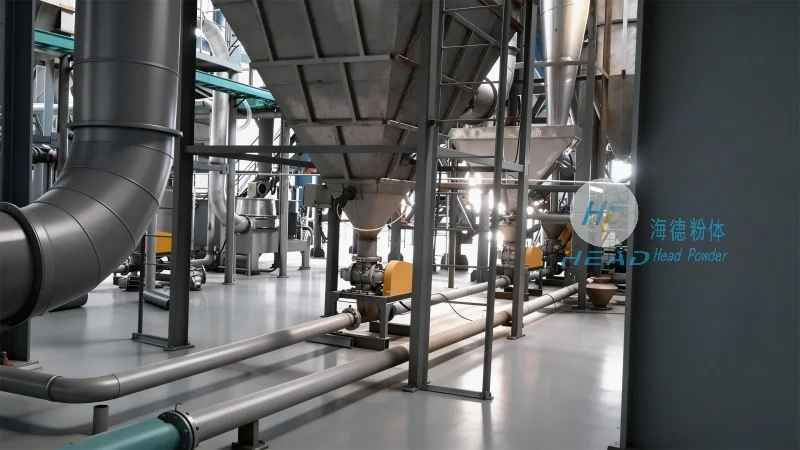
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying solutions, specializes in designing and manufacturing systems tailored to the unique needs of silage material. With decades of experience in the industry, HeadPowder has developed advanced pneumatic conveying systems that address the challenges of handling bulk powders like silage. Their systems are engineered to maximize efficiency, minimize downtime, and ensure compliance with industry standards. By leveraging cutting-edge technology and robust materials, HeadPowder's solutions help agricultural operations achieve higher productivity and lower operational costs. The company's commitment to innovation and customer satisfaction has made it a trusted partner for farms and processing facilities seeking reliable silage handling solutions.
As agricultural operations continue to evolve, the demand for efficient and sustainable material handling solutions will only increase. Pneumatic conveying systems, particularly those designed for silage material, offer a forward-thinking approach to addressing these needs. By combining advanced technology with practical design, these systems provide a reliable and effective means of transporting bulk powders while minimizing environmental impact. For agricultural businesses looking to enhance their operational efficiency and sustainability, investing in a pneumatic conveying system from a reputable provider like Shandong HeadPowder Engineering Co., Ltd. is a strategic decision that can yield long-term benefits. The future of silage handling lies in innovative, efficient technologies that support the growth and success of modern agriculture.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top