With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading enterprise in the field of material handling technology, specializes in the design, manufacturing, and implementation of pneumatic conveying systems for rare earth mineral powders. The company, based in Shandong, China, has established itself as a trusted partner for industries requiring efficient and reliable transport solutions for these specialized materials.
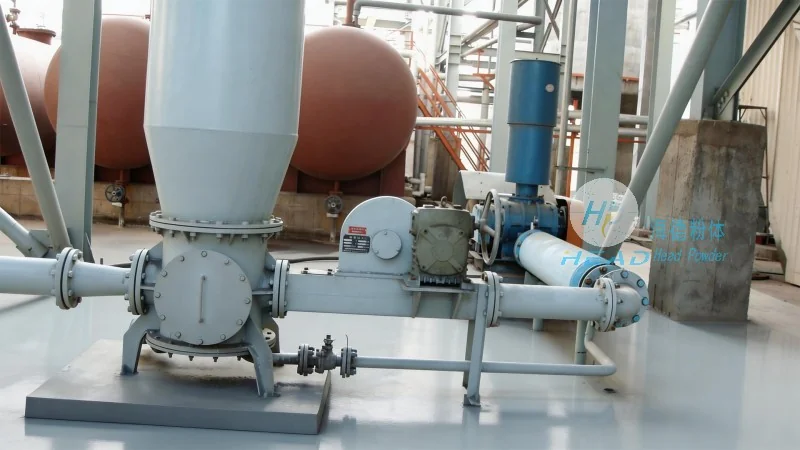
Pneumatic conveying is a method used to transport bulk materials like rare earth mineral powders through a pipeline using air or other gas as the conveying medium. This technology offers significant advantages over traditional mechanical conveying methods, including reduced equipment wear, lower maintenance costs, and the ability to handle materials that are difficult to transport via conventional means. The system typically consists of a series of components that work together to ensure the safe and efficient movement of the material from the source to the destination.
The core principle behind pneumatic conveying is the use of differential pressure to move the material through the pipeline. In a typical system, a blower or compressor generates a flow of air that creates a pressure differential between the inlet and outlet of the conveying line. The rare earth mineral powder is introduced into the system at the inlet, where it is mixed with the air stream. As the air flows through the pipeline, it carries the powder particles along, maintaining a suspension that allows for smooth transport. The system may include various components such as feeders, cyclones, filters, and control valves to regulate the flow and ensure proper separation of the material from the air at the discharge point.
The operation of a rare earth mineral powder pneumatic conveying system involves several key steps that ensure optimal performance and material integrity. The process begins with the preparation of the material at the source, where the rare earth mineral powder is loaded into a hopper or storage silo. A feeder, such as a rotary valve or screw feeder, then meters the material at a controlled rate into the conveying line. Simultaneously, the air supply system, which includes the blower and associated piping, generates the necessary airflow to initiate the conveying process.
Once the material is introduced into the pipeline, the air flow carries the powder particles through the system. The conveying line may include bends, expansions, or other components that help maintain the suspension and prevent material settling or blockages. At the discharge end, a cyclone or other separation device is used to separate the powder from the air stream. The separated powder is collected in a receiving hopper or storage container, while the air is either filtered and recirculated or discharged to the atmosphere, depending on the system design and environmental regulations.
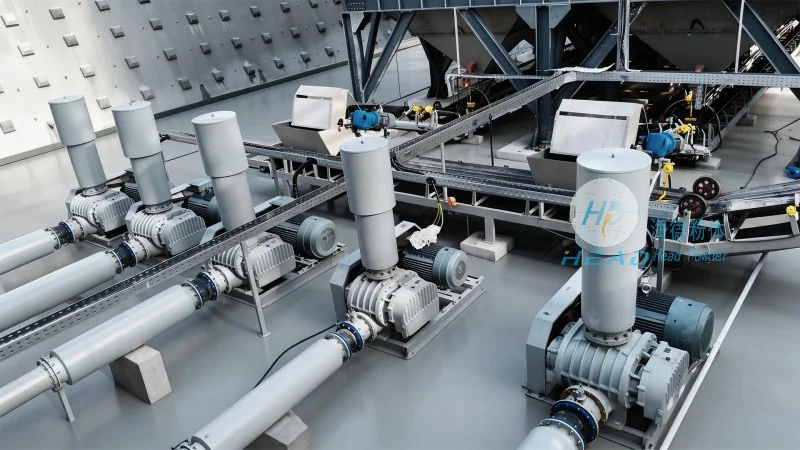
Several critical components are integral to the successful operation of a rare earth mineral powder pneumatic conveying system. The blower or compressor is the primary source of air pressure, providing the necessary force to move the material through the pipeline. The feeder is responsible for controlling the flow rate of the material, ensuring a consistent and uniform feed into the system. The conveying line, typically made of stainless steel or other corrosion-resistant materials, is designed to withstand the abrasive nature of the rare earth mineral powder and maintain airtight integrity to prevent leaks.
Additional components may include cyclones for material separation, filters to remove dust from the air stream, and control valves to regulate the pressure and flow within the system. These components work in tandem to ensure that the material is transported efficiently and that the air is properly managed to maintain system performance and compliance with safety and environmental standards.
Implementing a pneumatic conveying system for rare earth mineral powders offers numerous benefits that enhance operational efficiency and material handling capabilities. One of the primary advantages is the ability to handle materials that are prone to caking or agglomeration, as the air suspension prevents particle-to-particle contact and maintains the material in a free-flowing state. This reduces the risk of blockages and equipment damage, which are common issues with mechanical conveying systems.
Another key benefit is the reduced maintenance requirements compared to mechanical systems. Since there are no moving parts in direct contact with the material (except for the feeder), the system experiences less wear and tear, leading to lower maintenance costs and longer equipment life. Additionally, pneumatic conveying allows for flexible system design, enabling the integration of multiple conveying lines and the ability to transport materials over long distances without the need for intermediate storage or transfer points.
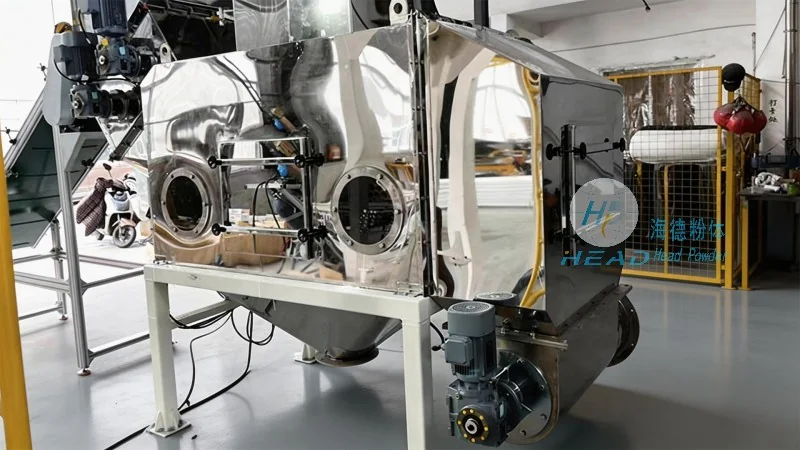
Furthermore, the system provides better control over the material flow, allowing for precise dosing and regulation of the powder delivery. This is particularly important in industrial processes where the quality and consistency of the rare earth mineral powder are critical, such as in the production of rare earth alloys, magnets, and other high-value products. The ability to maintain a consistent flow rate and particle size distribution ensures that downstream processes operate efficiently and produce high-quality end products.
HeadPowder's pneumatic conveying systems are widely used in various industries that rely on rare earth mineral powders for their manufacturing processes. These include the electronics industry, where rare earth elements are used in the production of permanent magnets for motors and generators; the automotive industry, which utilizes rare earth materials in catalytic converters and other components; and the renewable energy sector, where rare earths are essential for the production of wind turbine components and solar panels.
In each of these applications, the efficient and reliable transport of rare earth mineral powders is crucial to maintaining production schedules and ensuring product quality. HeadPowder's systems are designed to meet the specific requirements of these industries, providing customized solutions that address the unique challenges of material handling in each application. The company's expertise in system design and implementation ensures that clients receive tailored solutions that optimize their material transport processes and enhance overall operational performance.
As the demand for rare earth mineral powders continues to grow in various high-tech industries, the importance of efficient material handling solutions cannot be overstated. Pneumatic conveying systems, such as those offered by HeadPowder, provide a reliable and effective means of transporting these specialized materials while minimizing operational risks and costs. With its headquarters in Shandong, China, HeadPowder remains committed to delivering innovative and high-quality pneumatic conveying solutions that meet the evolving needs of its clients in the global market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top