With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in advanced powder handling solutions. This article explores the fundamental principles of negative pressure vacuum pneumatic conveying systems and their diverse applications across various industries.
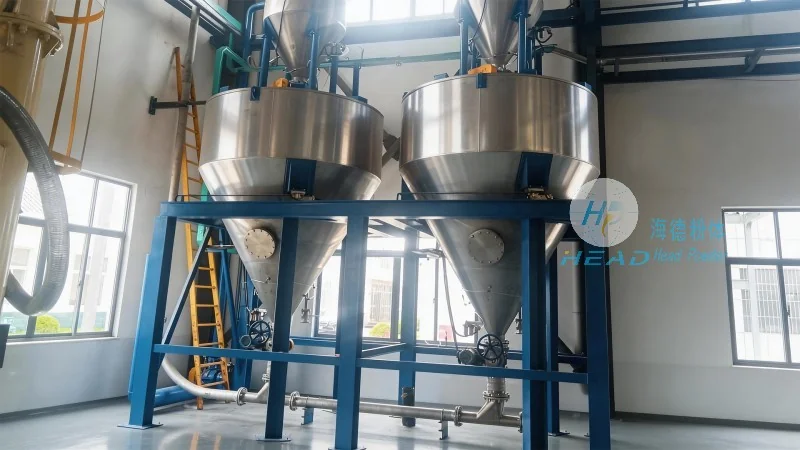
The negative pressure vacuum system operates by creating a pressure differential between the conveying line and the surrounding environment. A vacuum pump is used to draw air and powder particles from the source container into the pipeline. As the vacuum pump extracts air, it generates a negative pressure within the system, which pulls the powder particles along with the air stream. This method effectively transports dry powders over long distances without the need for positive pressure, reducing energy consumption and operational costs.
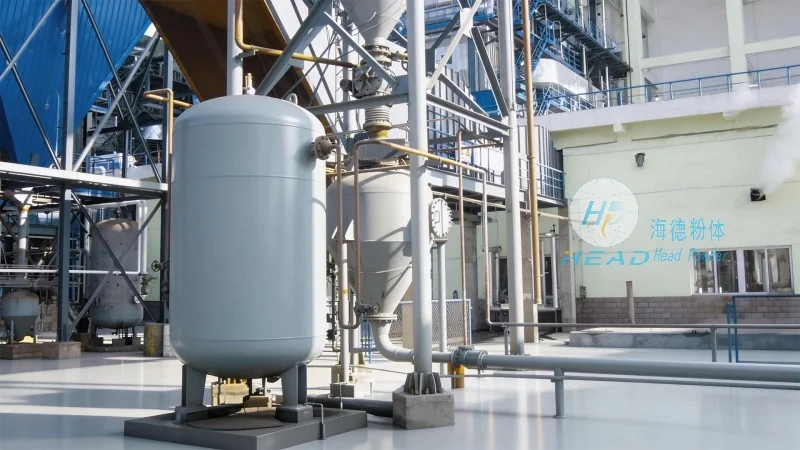
The negative pressure vacuum powder conveying system consists of several critical components that work in tandem to ensure efficient operation. These include a vacuum pump, a hopper or feeder for powder loading, a filter to separate powder from air, and a discharge valve for material release. The vacuum pump is the heart of the system, responsible for maintaining the negative pressure. The feeder controls the flow rate of powder into the pipeline, preventing clogging and ensuring consistent conveying. The filter is essential for capturing fine powder particles and preventing contamination of the air stream, which is then safely vented or recycled. The discharge valve regulates the release of material at the destination, allowing for controlled unloading.
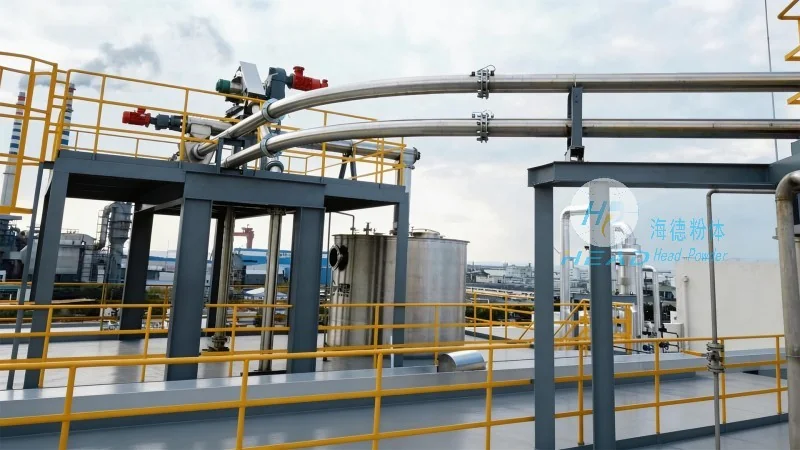
Negative pressure vacuum pneumatic conveying is widely utilized in industries where the handling of sensitive or hazardous powders is required. In the chemical industry, it is used to transport raw materials and finished products, such as pigments, catalysts, and powders used in pharmaceuticals. The food and beverage sector employs this technology for conveying ingredients like flour, sugar, and spices, ensuring hygienic and dust-free processing. The pharmaceutical industry benefits from the system's ability to handle sterile powders, maintaining contamination control and meeting stringent regulatory standards. Additionally, in the agricultural sector, negative pressure vacuum conveying is used for transporting fertilizers and other agricultural powders, providing a cost-effective and efficient method for material transport.
Compared to positive pressure systems, negative pressure vacuum conveying offers several advantages. It reduces energy consumption as it does not require high-pressure air to push the material. The system is also more suitable for long-distance conveying as the negative pressure can maintain a consistent flow over extended pipelines. Furthermore, it minimizes product degradation as the powder is not subjected to high pressure or turbulence, which can cause agglomeration or particle breakage. The system is also more environmentally friendly, as it does not release high-pressure air into the environment, reducing noise and air pollution. Additionally, the negative pressure system is safer for handling hazardous materials, as it prevents the release of toxic or flammable powders into the atmosphere.
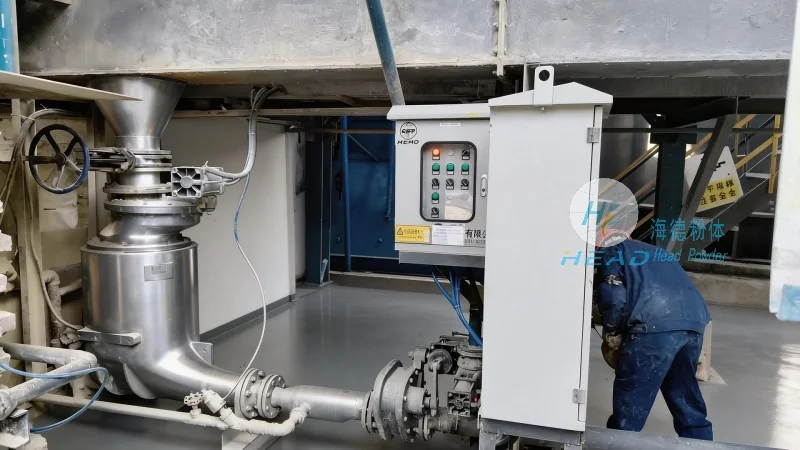
Shandong HeadPowder Engineering Co., Ltd. is a trusted provider of negative pressure vacuum powder pneumatic conveying systems, offering customized solutions tailored to the specific needs of various industries. With a focus on innovation and quality, HeadPowder ensures that its systems meet the highest standards of efficiency, safety, and reliability. The company's expertise in powder handling technology enables it to deliver effective solutions for a wide range of applications, contributing to improved productivity and operational excellence in powder processing industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top