With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Centralized powder bulk material pneumatic conveying equipment serves as a pivotal component in modern industrial material handling systems, enabling efficient transport of bulk powders and granular materials from various sources to designated destinations. This technology is engineered to handle a wide array of materials, including chemicals, food additives, pharmaceuticals, and other fine powders, ensuring safe, reliable, and efficient material transfer within industrial processes. The system typically integrates advanced pneumatic technology with centralized control mechanisms, facilitating seamless coordination of material flow and process management across facilities.
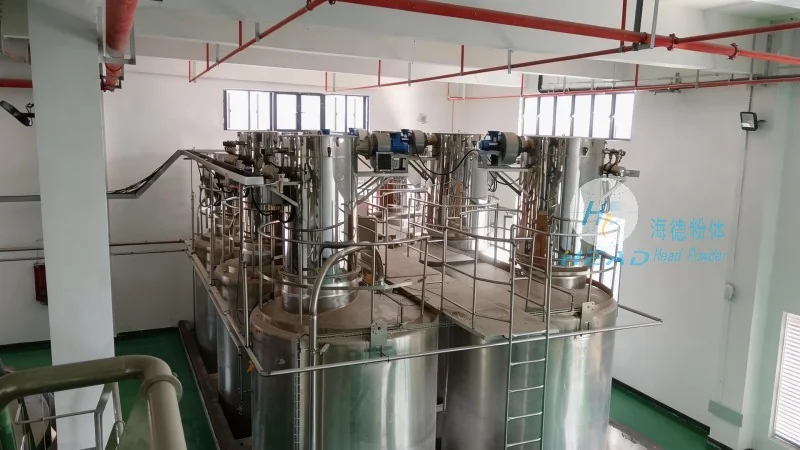
HeadPowder, a leading manufacturer in powder handling technology, specializes in the research, development, and production of advanced pneumatic conveying systems. With a strong focus on innovation and customer-centric solutions, the company has established itself as a trusted partner for industries requiring high-performance material transport solutions. HeadPowder's headquarters is located in Shandong, China, where the company leverages local expertise and manufacturing capabilities to deliver cutting-edge equipment tailored to diverse industrial needs. The company's commitment to quality, reliability, and technological advancement has earned it a reputation for excellence in the powder handling industry.
The core principle of centralized powder bulk material pneumatic conveying equipment revolves around the use of compressed air or other gases to transport solid materials through a pipeline network. The system operates by creating a pressure differential between the material source and the destination, which propels the powder particles through the conveying line. Two primary system types exist: pressure and vacuum. Pressure systems utilize compressed air to push material forward, while vacuum systems employ suction to draw material from the source to the destination. The choice between these systems depends on factors such as material characteristics, distance, and system layout. In centralized configurations, the equipment is designed to manage multiple material sources and destinations, allowing for flexible and efficient material distribution across a facility.
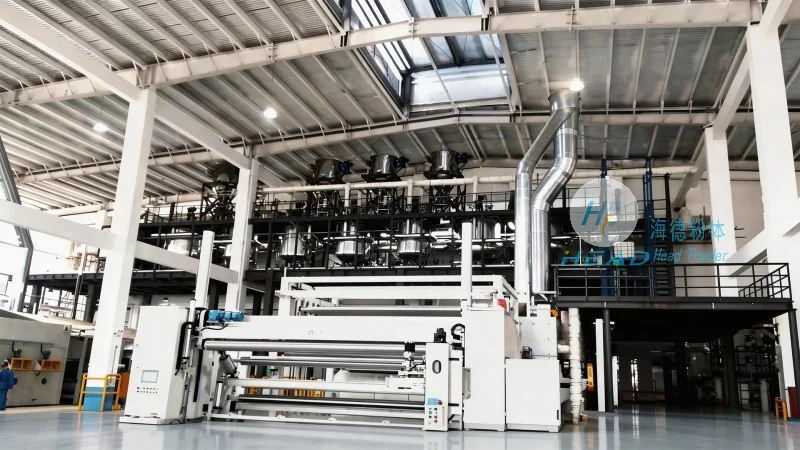
The centralized pneumatic conveying system comprises several critical components that work in unison to ensure smooth operation. These include the material feed hopper, which stores and feeds the powder into the conveying line; the air compressor or vacuum pump, which provides the necessary pressure or suction; the conveying pipeline, which transports the material; and the control system, which monitors and regulates material and air flow. The material feed hopper is equipped with a rotary valve or feeder to control discharge rate, preventing material bridging and ensuring consistent flow. The air compressor or vacuum pump generates the required pressure or vacuum, introduced into the pipeline via venturi or air injection devices. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, handles diverse powder types while maintaining hygiene standards. The control system, often integrated with sensors and automation, enables real-time monitoring of pressure, flow rate, and material levels, allowing automatic adjustments for optimal operation.
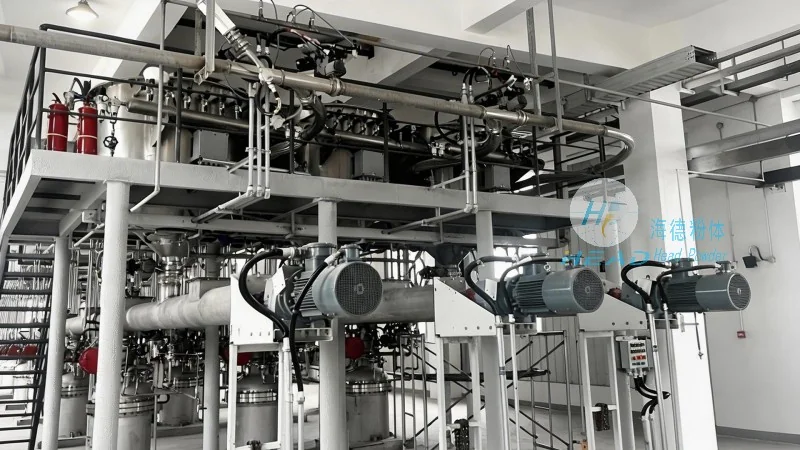
The centralized powder bulk material pneumatic conveying equipment is widely adopted across various industrial sectors due to its versatility and efficiency. In the chemical industry, it is used to transport raw materials, intermediates, and finished products, ensuring safe handling of hazardous powders. The food and pharmaceutical industries rely on this equipment for the transport of food additives, powders, and active pharmaceutical ingredients (APIs), where hygiene and contamination control are paramount. In the cement and construction materials sector, the system conveys cement, fly ash, and other bulk materials to production lines and storage facilities. Additionally, in the mining and mineral processing industries, pneumatic conveying systems transport ore powders and other mineral products from processing plants to storage or shipping locations. The equipment's ability to handle diverse materials and flexible system design makes it suitable for small-scale laboratory operations to large-scale industrial production lines.
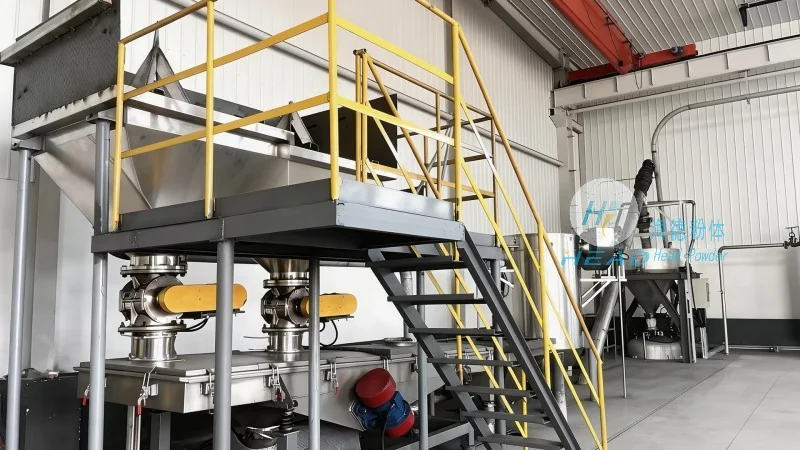
Centralized powder bulk material pneumatic conveying equipment offers numerous advantages over traditional material handling methods. One key benefit is reduced material handling costs, as the system eliminates manual labor and minimizes material loss or contamination risks. The equipment enhances process efficiency through continuous, automated material flow, reducing downtime and improving production throughput. Another significant advantage is improved safety and hygiene, as the system operates in a closed environment, preventing dust emissions and ensuring compliance with environmental regulations. The centralized control system allows for easy monitoring and maintenance, reducing on-site inspections and minimizing operational disruptions. Furthermore, the system's flexibility enables easy integration with existing production lines and expansion of the conveying network as production needs grow. The use of stainless steel and other corrosion-resistant materials ensures long-term durability and low maintenance costs, contributing to overall cost-effectiveness.
Centralized powder bulk material pneumatic conveying equipment, as a sophisticated solution for industrial material handling, continues to evolve with technological advancements. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of developing innovative systems that meet modern industry demands. Integration of automation, sensors, and advanced control technologies enhances system performance and reliability, making them more efficient and user-friendly. As industries pursue higher productivity, better safety standards, and sustainable operations, the role of centralized pneumatic conveying equipment becomes increasingly critical. With its ability to handle diverse materials, ensure safe and efficient transport, and adapt to changing production needs, this equipment remains a vital component in the future of industrial material handling.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top