With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
White sugar, a staple in global food and beverage industries, requires efficient and reliable handling from production to distribution. Pneumatic conveying systems have emerged as a key technology for transporting white sugar, offering advantages such as hygienic operation, minimal product contamination, and the ability to handle fine powders. This article explores the fundamental principles of white sugar pneumatic conveying systems and highlights the specific working scene characteristics that make them suitable for sugar processing applications.
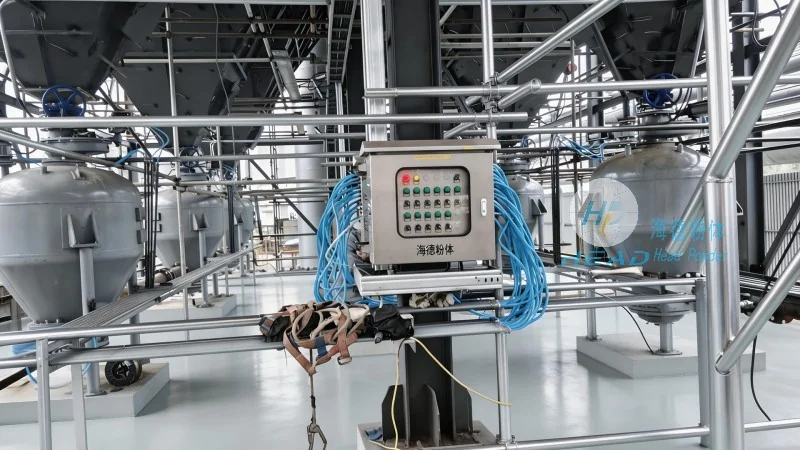
Headpowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of advanced material handling solutions. With a focus on industrial applications, Headpowder provides tailored pneumatic conveying systems that meet the unique demands of the sugar industry. The company's expertise in material flow technology ensures that their systems are optimized for efficiency, durability, and compliance with industry standards.
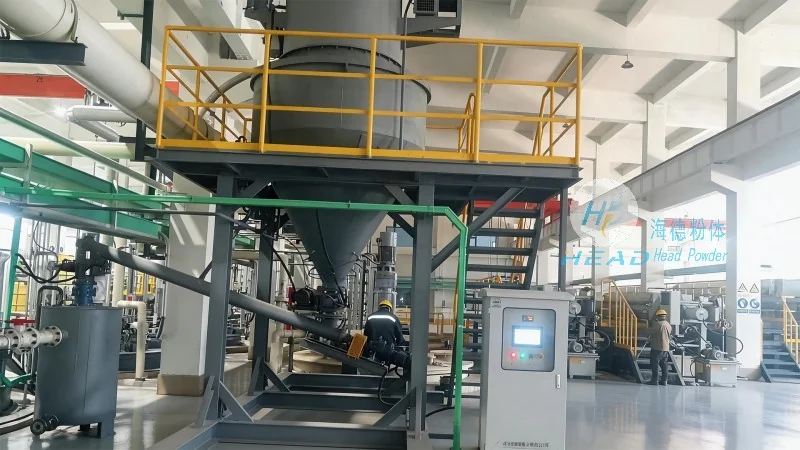
Pneumatic conveying systems operate by using air or gas to transport bulk materials like white sugar through a pipeline network. The core principle involves creating a pressure differential that propels the sugar particles along the conveying line. There are two main types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push the material, while vacuum systems create a negative pressure to draw the material. For white sugar, which is a fine powder, pressure systems are often preferred due to their ability to handle high volumes and maintain consistent flow rates. The system typically includes a hopper for material storage, a feeder to control the flow rate, a conveying line, and a receiver for the delivered sugar. The air flow is regulated to ensure that the sugar particles are suspended and transported without clogging or degradation.
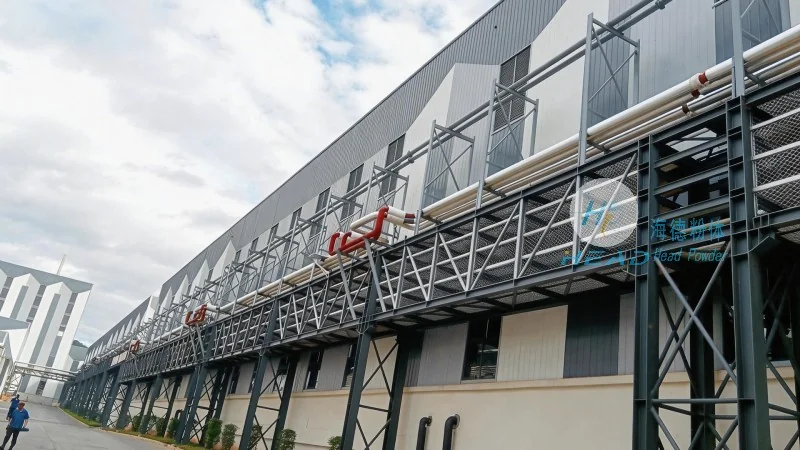
The working scene characteristics of white sugar pneumatic conveying systems are tailored to the specific requirements of sugar processing facilities. These characteristics include: 1. Hygienic Design: The systems are constructed with materials that are easy to clean and sanitize, such as stainless steel, to meet food safety regulations. 2. Low Product Contamination: The enclosed pipeline design prevents cross-contamination and exposure to external elements, preserving the quality and purity of the white sugar. 3. Energy Efficiency: Modern systems incorporate energy-saving features, such as variable frequency drives (VFDs), to optimize air consumption and reduce operational costs. 4. Scalability: The systems can be designed to handle varying production volumes, from small-scale operations to large industrial facilities. 5. Minimal Downtime: Robust components and regular maintenance schedules ensure that the system operates with minimal interruptions, maintaining production continuity. 6. Customization: Headpowder offers customized solutions that adapt to specific plant layouts, material properties, and operational constraints, ensuring optimal performance.
White sugar pneumatic conveying systems are widely used in various stages of sugar processing, including: 1. Raw Material Handling: Transporting raw sugar from storage silos to processing units. 2. Intermediate Processing: Moving sugar slurry or fine powder between refining stages. 3. Packaging and Distribution: Conveying finished white sugar into packaging lines or storage tanks. 4. Waste Management: Handling sugar residues or byproducts for recycling or disposal. Each application requires a specific system configuration to address the unique challenges of that stage, such as varying particle sizes, moisture content, or flow rates.

Headpowder's pneumatic conveying systems for white sugar offer several advantages that enhance operational efficiency and product quality. These include: 1. Expert Engineering: The company's team of engineers designs systems based on thorough analysis of material properties and process requirements, ensuring optimal performance. 2. High Reliability: Robust components and rigorous quality control measures result in systems with long service life and low maintenance needs. 3. Compliance with Standards: The systems meet international food safety and industrial standards, providing peace of mind for manufacturers. 4. Cost-Effective Operation: Energy-efficient designs and reduced downtime lower long-term operational costs. 5. Comprehensive Support: Headpowder provides installation, training, and after-sales support to ensure smooth integration and operation of the system.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top