With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Stainless steel bulk bag pneumatic conveying systems represent a sophisticated method for transporting bulk materials efficiently and safely. This technology is particularly valued in industries where material handling demands precision, hygiene, and durability. The system leverages compressed air to move materials from a bulk bag into processing equipment, offering a solution that minimizes contamination and reduces manual labor. As a key component in material handling, understanding its principles and application scenarios is crucial for optimizing operational efficiency.
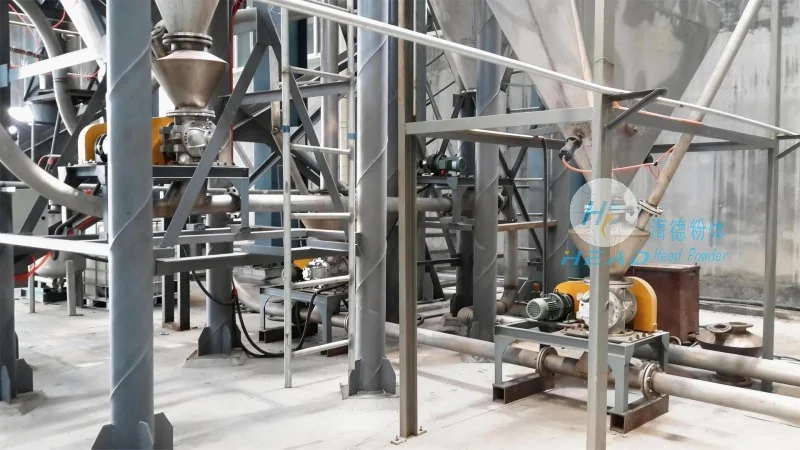
The fundamental principle of pneumatic conveying involves the use of air to transport particulate materials. In the case of stainless steel bulk bag systems, the process typically operates under positive pressure, where compressed air is introduced into the bulk bag to displace the material. This method ensures that the material is moved without direct contact with the conveying line, preserving its integrity and preventing contamination. The stainless steel construction of the equipment further enhances this by providing corrosion resistance and maintaining a clean environment, which is essential for industries dealing with food, pharmaceuticals, or sensitive chemicals. The system’s design allows for controlled flow rates, enabling precise dosing and reducing material waste.
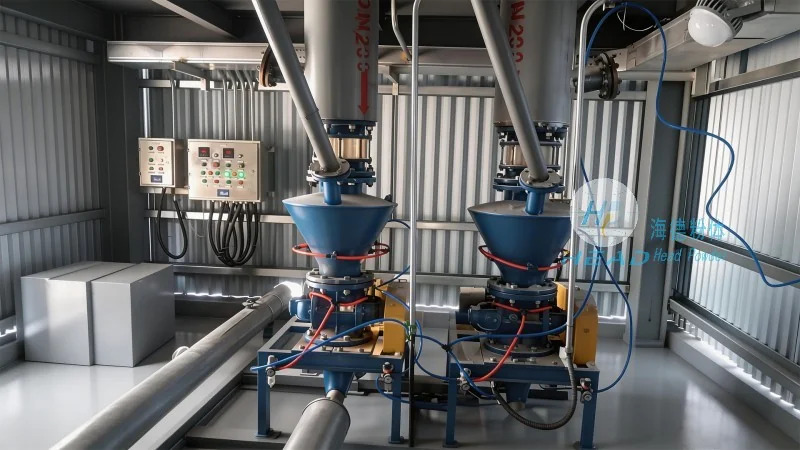
One of the primary advantages of this technology is its ability to handle a wide range of materials, from fine powders to granules, while maintaining high purity standards. The stainless steel construction ensures that the system is resistant to corrosion and can withstand harsh chemical environments, making it suitable for diverse industrial applications. Additionally, the bulk bag design offers flexibility in material storage and transportation, as bags can be easily replaced or reused, reducing inventory costs. The pneumatic conveying process also minimizes dust generation compared to traditional methods like belt conveyors, contributing to a cleaner and safer working environment. For companies operating in sectors such as food processing, pharmaceutical manufacturing, or chemical production, these benefits translate into improved product quality and regulatory compliance.
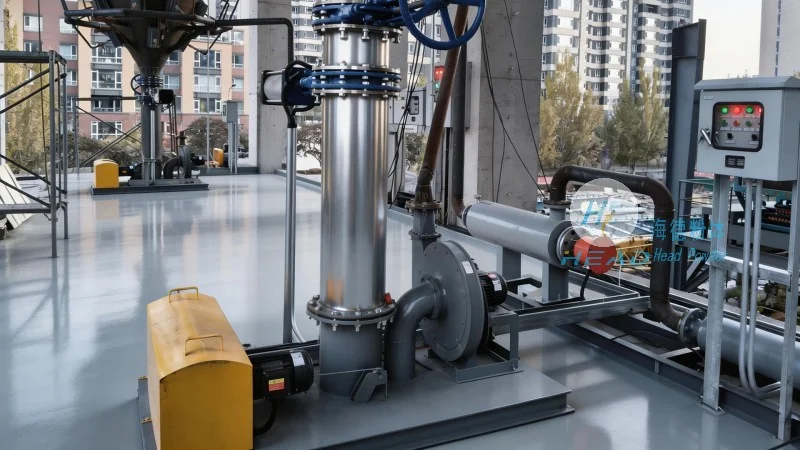
The working scene characteristics of stainless steel bulk bag pneumatic conveying systems vary based on the industry and specific application requirements. In food and beverage industries, for instance, the system is often used to handle ingredients like flour, sugar, or spices, where hygiene and contamination prevention are paramount. The stainless steel components and enclosed conveying process ensure that the materials remain free from external contaminants, meeting stringent food safety standards. In pharmaceutical manufacturing, similar principles apply, as the system can transport active pharmaceutical ingredients (APIs) or excipients with minimal risk of cross-contamination. The ability to control the flow rate and maintain a sterile environment makes it ideal for sensitive drug production. In the chemical industry, the system is used for handling corrosive or abrasive materials, where the stainless steel construction protects against wear and corrosion. The bulk bag’s capacity allows for large-scale material handling, reducing the frequency of material changes and improving overall production throughput. Additionally, the system’s compact design makes it suitable for facilities with limited space, as it can be integrated into existing production lines without extensive modifications.
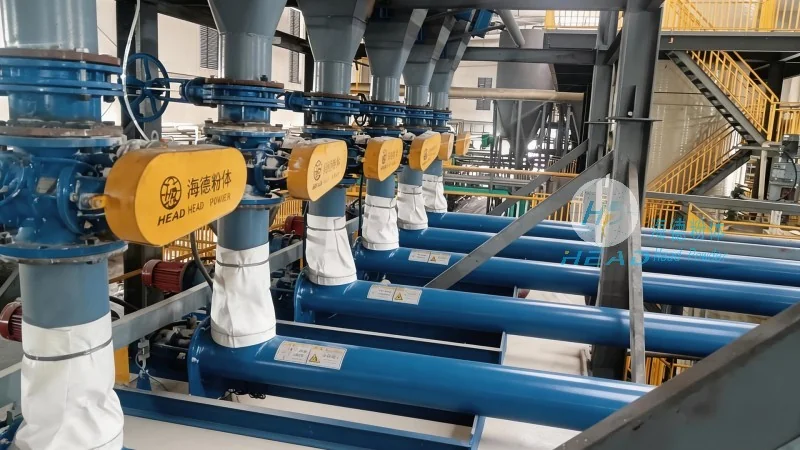
Real-world applications of stainless steel bulk bag pneumatic conveying systems demonstrate their effectiveness in enhancing operational efficiency. For example, in a food processing plant, the system can be used to transfer bulk ingredients from storage bags into mixing or packaging equipment. By automating the material transfer process, the plant reduces labor costs and minimizes the risk of human error. The stainless steel construction ensures that the system remains clean and sanitary, which is critical for maintaining product quality and meeting regulatory requirements. In a pharmaceutical facility, the system may be used to transport raw materials into a tablet press or capsule filling machine. The precise control of material flow allows for consistent product quality, reducing the likelihood of batch failures. The bulk bag’s ability to hold large quantities of material also reduces downtime associated with frequent material replenishment. In the chemical industry, the system can handle bulk chemicals for manufacturing processes, such as the production of fertilizers or coatings. The stainless steel components withstand the corrosive nature of these materials, extending the system’s lifespan and reducing maintenance costs. Overall, the integration of stainless steel bulk bag pneumatic conveying into these applications results in improved productivity, reduced operational costs, and enhanced product safety.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top