With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
For businesses in the food processing industry, efficient and reliable handling of cereal powders is crucial. Cereal powder conveyors, also known as bulk handling systems, are specialized equipment designed to transport and manage these fine powders with precision. This article explores the working principles and key features of such systems, highlighting how they enhance operational efficiency and product quality.
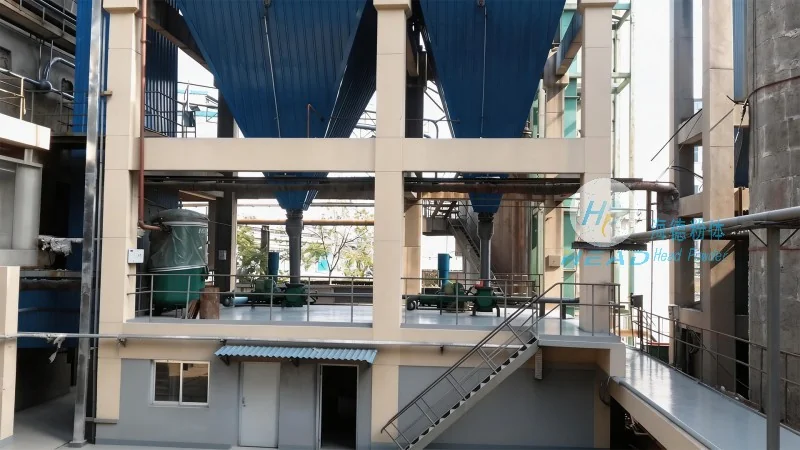
The core functionality of a cereal powder conveyor revolves around the movement of powders from a storage or processing point to a destination, such as a packaging line or storage silo. These systems typically operate on the principle of pneumatic or mechanical transport, depending on the specific design and application requirements. Pneumatic conveyors use air pressure to move powders through a pipeline, while mechanical conveyors rely on belts, screws, or other mechanical components to transfer the material. The choice of mechanism depends on factors like the powder's characteristics, the distance to be covered, and the desired level of control.
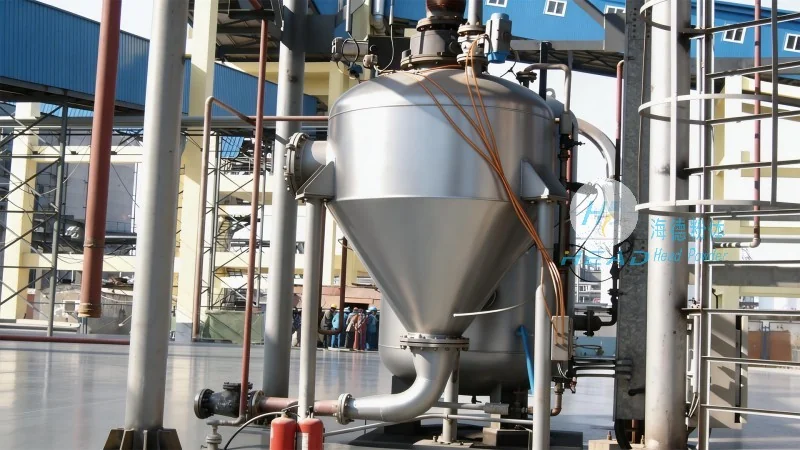
HeadPowder, a leading manufacturer based in Shandong, China, offers advanced cereal powder conveyors with several notable features. These systems are engineered for high efficiency, ensuring minimal product loss and consistent flow rates. The conveyors are designed with materials that resist corrosion and wear, making them suitable for handling various cereal powders, including wheat, corn, and oats. Additionally, the systems incorporate advanced control mechanisms that allow for precise regulation of flow, preventing issues like clogging or overloading. The design also prioritizes hygiene, with components that are easy to clean and maintain, which is essential for food-grade applications.
Implementing a cereal powder conveyor system brings numerous benefits to food processing operations. Firstly, it significantly improves productivity by automating the material handling process, reducing the need for manual labor and minimizing downtime. The consistent flow of powders ensures that production lines run smoothly, leading to higher output and better resource utilization. Secondly, the systems enhance product quality by maintaining the integrity of the cereal powder, preventing contamination or degradation during transport. This is particularly important for sensitive products that require careful handling. Thirdly, the advanced control features allow for better monitoring and adjustment, enabling operators to respond quickly to changes in production needs. Overall, cereal powder conveyors contribute to a more efficient, reliable, and cost-effective operation.
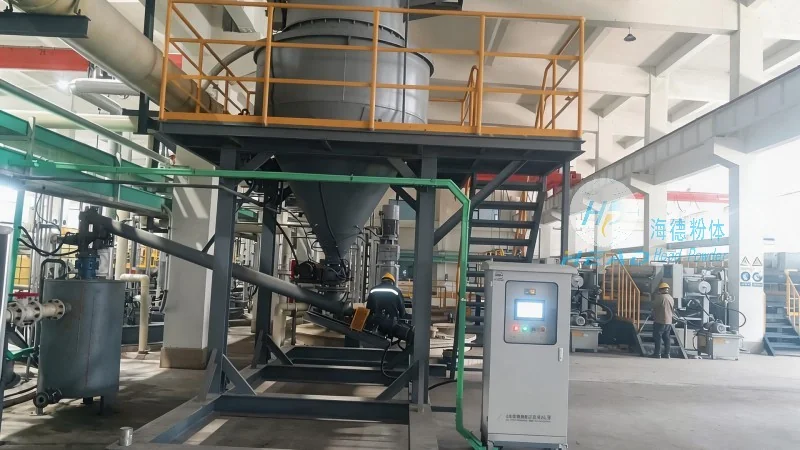
Cereal powder conveyors are essential equipment for modern food processing facilities, offering a reliable solution for the efficient handling of cereal powders. With their advanced working principles and key features, these systems enhance operational efficiency, product quality, and overall productivity. HeadPowder, with its expertise in bulk handling equipment, provides high-quality conveyors that meet the specific needs of food processing businesses. By investing in such systems, companies can ensure smooth operations and maintain the high standards required in the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top