

Working Principle and Features of a Potassium Carbonate Pneumatic Conveying System
For industrial applications involving the handling of potassium carbonate, efficient and reliable material transport is crucial. A pneumatic conveying system specifically designed for this purpose offers a solution that combines advanced technology with operational efficiency. This article explores the working principle and key features of a potassium carbonate pneumatic conveying system, highlighting how it addresses the unique challenges associated with handling this chemical compound.
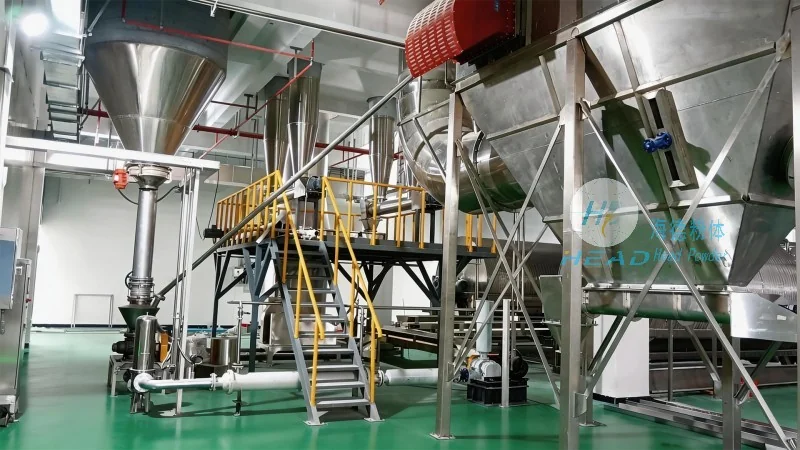
Overview of the Potassium Carbonate Pneumatic Conveying System
The potassium carbonate pneumatic conveying system is engineered to transport bulk potassium carbonate from storage silos or processing units to various destinations such as packaging lines, reactors, or storage areas. It operates on the principle of using compressed air or other gases to move the material through a network of pipes. This method eliminates the need for mechanical components like conveyor belts or buckets, reducing maintenance requirements and enhancing safety in handling potentially hazardous materials.
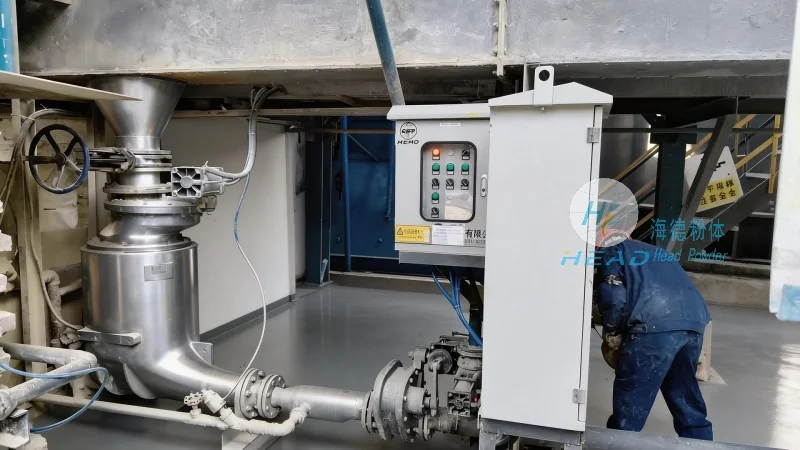
Working Principle of the System
The core mechanism of the potassium carbonate pneumatic conveying system involves several key steps. First, the potassium carbonate is introduced into the system, typically from a hopper or storage vessel. The material is then fed into a conveying line where it is mixed with a stream of compressed air. As the air flows through the pipe, it creates a low-pressure zone that draws the material along with it, forming a slurry or suspension. This mixture travels through the pipeline under pressure, reaching the destination point where the air is separated from the material, often through a cyclone or filter system. The separated potassium carbonate is then discharged, while the air is either recirculated or vented to the atmosphere. The system's design ensures that the material is transported smoothly without clogging or degradation, maintaining product integrity throughout the process.
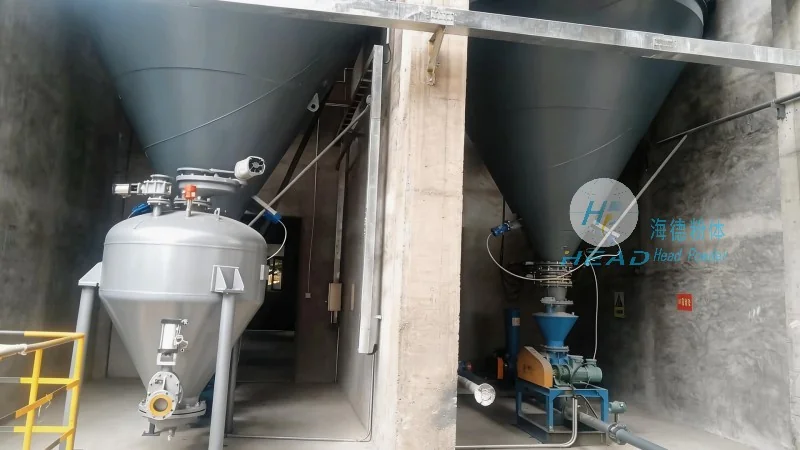
Key Features and Advantages
Several notable features define the performance and benefits of a potassium carbonate pneumatic conveying system. Firstly, it provides a dust-free and enclosed transport environment, which is essential for maintaining product quality and ensuring workplace safety. Unlike traditional bulk handling methods, this system minimizes exposure to airborne particles, reducing the risk of inhalation hazards and contamination. Secondly, the system offers high efficiency in material transport, with the ability to handle large volumes of potassium carbonate at a consistent rate. This efficiency is achieved through optimized air flow and pipe design, which minimizes energy consumption while maximizing throughput. Thirdly, the system is highly flexible, allowing for multiple delivery points and the integration with other processing equipment. This flexibility enables manufacturers to adapt the system to changing production needs without significant modifications. Additionally, the system's low maintenance requirements contribute to operational cost savings, as there are fewer moving parts and less wear on components compared to mechanical conveyors. The enclosed design also helps in controlling temperature and moisture levels, which are critical factors for preserving the quality of potassium carbonate during transport.
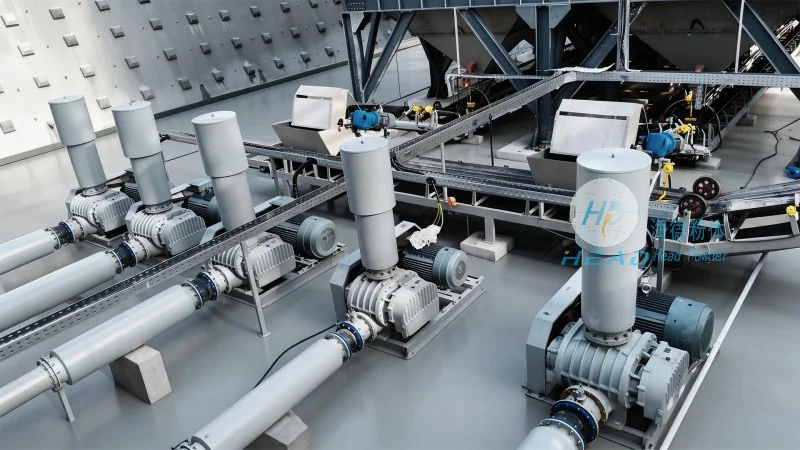
Company Information and Application
Shandong HeadPowder Engineering Co., Ltd., a leading provider of bulk material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the needs of the chemical industry. With a focus on innovation and customer satisfaction, the company has developed advanced systems that ensure reliable and efficient transport of potassium carbonate and other similar materials. The company's expertise in material flow dynamics and system integration allows them to deliver customized solutions that meet specific operational requirements. By leveraging their experience and technical capabilities, Shandong HeadPowder Engineering Co., Ltd. helps clients optimize their material handling processes, improve productivity, and enhance overall operational efficiency. The company's commitment to quality and safety ensures that their systems are compliant with industry standards and regulations, providing peace of mind to clients operating in the chemical sector.