

What is a High-Temperature Ash Material Pneumatic Conveying System? And What Are Its Design Principl
High-temperature ash material pneumatic conveying systems represent a sophisticated approach to material handling in industries that generate significant volumes of hot ash as a byproduct of combustion processes. These systems are engineered to transport ash and similar high-temperature materials from the source of generation to a designated disposal or processing location using compressed air as the primary conveying medium. The core challenge in designing such systems lies in addressing the dual demands of thermal resistance and efficient material transport, as the ash can reach temperatures of 200°C or higher and may be abrasive, posing risks to conventional equipment. Consequently, the design must incorporate specialized components capable of withstanding these harsh conditions while maintaining the necessary air pressure and flow rates to move the material effectively.
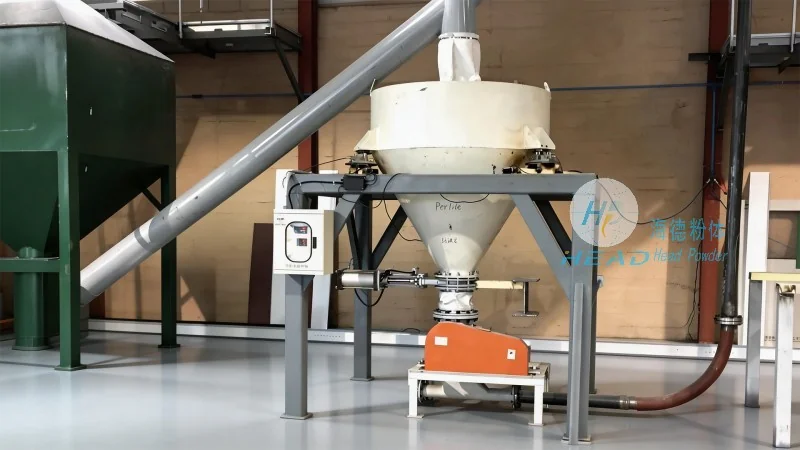
Key Components and Their Functions in High-Temperature Ash Pneumatic Conveying
The effectiveness of a high-temperature ash material pneumatic conveying system depends on the integration of several critical components, each playing a vital role in the overall operation. The first component is the ash hopper or feeder, which stores the material and feeds it into the system at a controlled rate. This hopper is typically made from high-temperature-resistant materials like stainless steel or heat-resistant alloys to prevent deformation or failure under extreme temperatures. The second key component is the blower or air compressor, which generates the necessary air pressure to move the ash through the pipeline. The choice of blower type—such as a centrifugal or positive displacement blower—depends on the system’s capacity and the specific characteristics of the ash, such as particle size and moisture content. The third component is the pipeline network, which consists of insulated or non-insulated pipes designed to withstand the high temperatures of the material-air mixture. The pipes are often equipped with bends, elbows, and other fittings that minimize pressure loss and ensure smooth material flow. The final component is the receiver or discharge unit, which collects the conveyed ash and discharges it into a storage bin or for further processing. This unit is also constructed from high-temperature-resistant materials to handle the hot material without degradation.
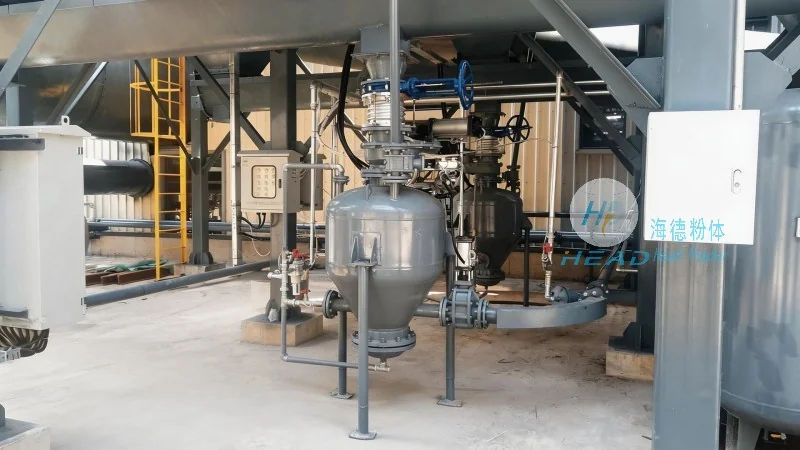
Design Principles for Ensuring System Efficiency and Reliability
The design principles guiding the development of high-temperature ash material pneumatic conveying systems prioritize thermal stability, material handling efficiency, and operational safety. Thermal stability is achieved through the use of materials with high thermal conductivity and resistance to oxidation, such as stainless steel grades like 304 or 316, which can withstand temperatures up to 400°C or higher. The system’s design also incorporates insulation in critical areas, such as the hopper and pipeline, to reduce heat loss and prevent external components from overheating. Material handling efficiency is optimized by selecting the appropriate air velocity and pressure, which is determined by factors like the ash’s bulk density, particle size distribution, and the system’s total length. A common design approach is to maintain an air velocity of 20-30 meters per second to ensure the ash particles remain suspended in the air stream without settling or causing blockages. System reliability is enhanced through the inclusion of monitoring and control systems, including temperature sensors, pressure gauges, and flow meters, which provide real-time data on the system’s performance. Additionally, safety features like automatic shutdown mechanisms are integrated to prevent over-pressurization or overheating, protecting both the equipment and personnel from potential hazards.
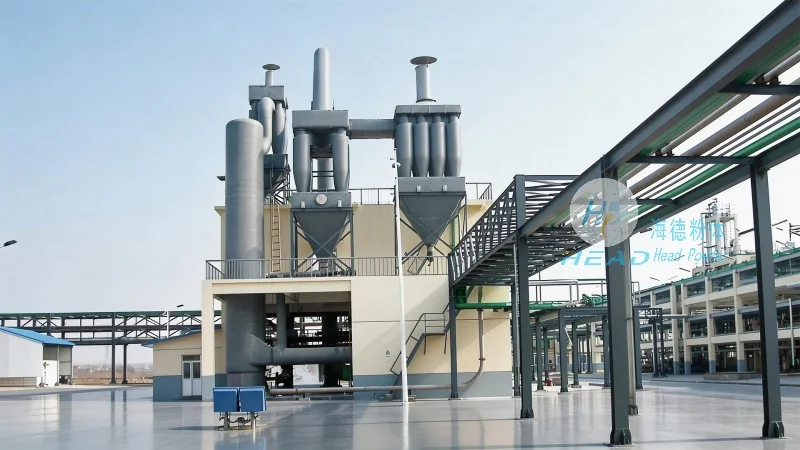
Applications and Benefits in Industrial Settings
High-temperature ash material pneumatic conveying systems find extensive applications in power plants, where they are used to transport ash from boilers, cyclones, and other combustion equipment to ash storage facilities or for recycling. In these settings, the systems help reduce the need for manual handling of hot and heavy ash, which improves worker safety and reduces labor costs. The benefits of these systems extend beyond efficiency and safety; they also contribute to environmental sustainability by preventing ash spillage and reducing the risk of dust emissions. Furthermore, the systems can be integrated with other waste management processes, such as ash pelletization or utilization in construction materials, to enhance the overall value of the ash byproducts. The reliability and durability of high-temperature ash pneumatic conveying systems make them a preferred choice for facilities that require consistent and long-term material transport solutions.
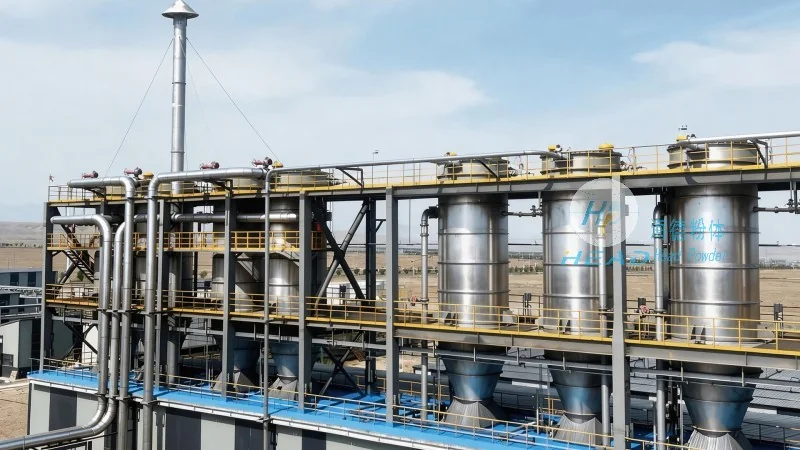
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name HeadPowder, is a prominent player in the global market for pneumatic conveying systems and industrial equipment. Headquartered in Shandong, China, the company has built a reputation for delivering high-quality, customized solutions tailored to the unique needs of its clients. With a team of experienced engineers and technicians, HeadPowder specializes in the design, manufacturing, and installation of high-temperature ash material pneumatic conveying systems, as well as other related equipment such as dust collectors and material handling units. The company’s commitment to research and development has enabled it to develop advanced technologies that address the challenges of handling hot and abrasive materials, ensuring that its products meet the highest standards of performance and reliability. HeadPowder serves a diverse range of industries, including power generation, cement production, and chemical processing, providing comprehensive material handling solutions that enhance operational efficiency and reduce environmental impact. Through its dedication to quality and customer satisfaction, HeadPowder has established itself as a trusted partner for facilities seeking reliable and efficient high-temperature ash handling systems.