With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
Wheat pneumatic conveying equipment is a specialized system designed to transport wheat and other bulk grains efficiently through an air-based mechanism. This technology is widely used in agricultural and food processing industries to ensure safe, clean, and reliable movement of grain from storage to processing units. The core principle involves using compressed air to create a flow that carries the wheat particles through a pipeline, eliminating the need for mechanical components like belts or buckets that can introduce contamination or wear over time.
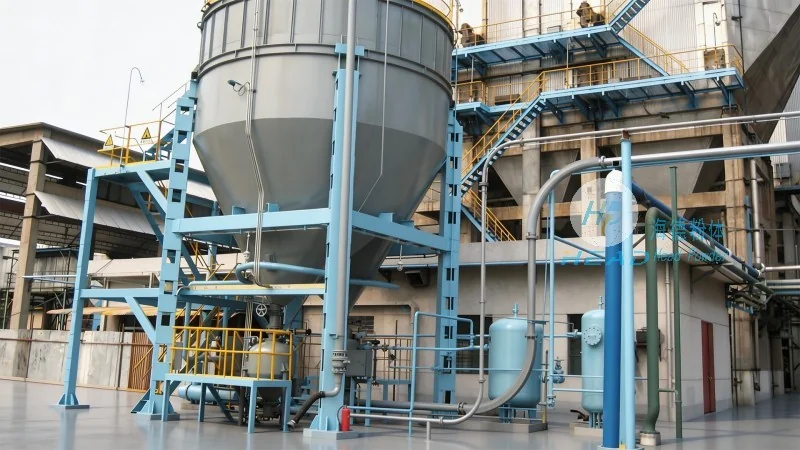
The system typically consists of several critical components that work in tandem to achieve effective grain transport. At the heart of the system is the air compressor, which generates the necessary pressure to move the wheat. This is followed by the feed hopper, where the wheat is loaded and fed into the system. The conveying line itself is a sealed pipeline that carries the wheat and air mixture. Along the line, there may be inlet and outlet valves to control the flow direction and manage the discharge of grain at the destination. Additionally, filters and cyclones are used to separate the wheat from the air, ensuring that the grain remains clean and free from dust or debris.
The operation of the wheat pneumatic conveying system follows a systematic process. First, the wheat is introduced into the feed hopper, where it is metered and fed into the conveying line. Simultaneously, the air compressor supplies compressed air into the line. The air and wheat mixture then travels through the pipeline, with the air pressure creating a flow that lifts and transports the wheat particles. As the mixture moves, it passes through the conveying line, which may include bends or changes in direction. At the receiving end, the air and wheat are separated using a cyclone or filter. The air is discharged, while the wheat is collected in a storage or processing container. This process is continuous and can be adjusted to handle varying volumes of wheat, making it suitable for both small-scale and large-scale operations.
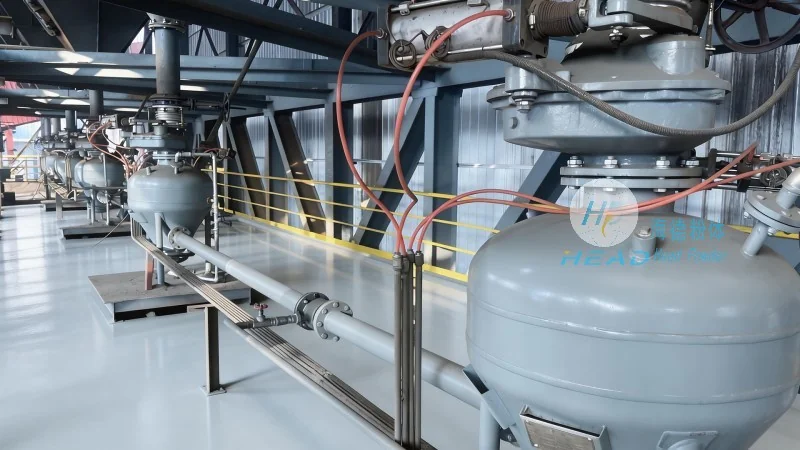
Compared to traditional mechanical conveying methods, wheat pneumatic conveying offers several advantages that make it a preferred choice in many industries. One of the most significant benefits is the hygienic and clean operation. Since the system is enclosed, there is no direct contact between the wheat and external elements, reducing the risk of contamination from dust, insects, or other environmental factors. This is particularly important for food-grade products like wheat, where quality and safety are paramount. Additionally, the system is low maintenance as it has fewer moving parts compared to belt or bucket elevators, which can reduce downtime and operational costs. The flexibility of the system also allows for easy integration with other processing equipment, such as milling or packaging machines, enabling a seamless workflow from storage to final product.
Wheat pneumatic conveying equipment is widely applied in various stages of the agricultural and food processing chain. In grain storage facilities, the system is used to transfer wheat from silos or storage bins to processing plants, ensuring efficient movement without the need for manual handling. During the milling process, the equipment can transport wheat from the cleaning and grading stages to the grinding and sifting units, maintaining the grain's quality and preventing damage. In food production, the system is also used to move wheat flour or other processed products from storage to packaging lines, ensuring a consistent and clean supply. The versatility of the system makes it suitable for both raw wheat and processed products, catering to the diverse needs of the food industry.
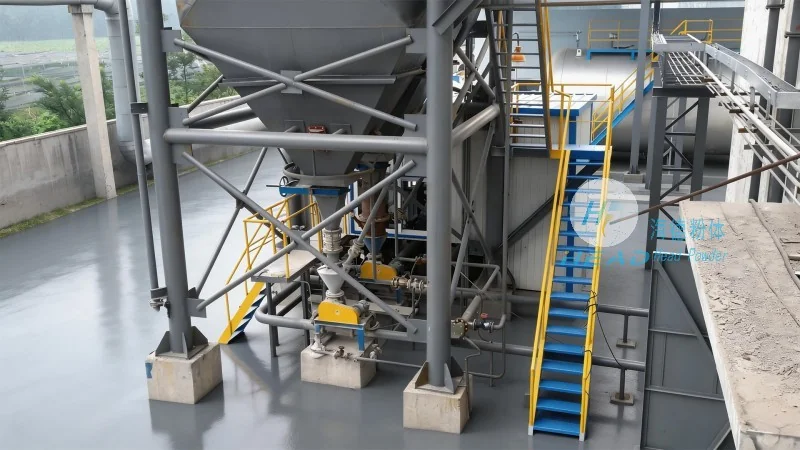
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized wheat pneumatic conveying systems to meet the specific requirements of different clients. The company understands that each agricultural or food processing facility has unique operational needs, such as varying grain volumes, storage capacities, or processing capabilities. Therefore, their engineers work closely with clients to develop tailored solutions that optimize efficiency and performance. The systems can be scaled from small, compact units for small-scale farms to large, industrial systems for major grain processing plants. Additionally, the company offers options for different conveying methods, such as pressure or vacuum systems, depending on the client's specific application and budget. This flexibility ensures that clients receive a system that is not only effective but also cost-efficient and easy to maintain.
Ensuring the longevity and reliability of wheat pneumatic conveying equipment is a top priority for Shandong HeadPowder Engineering Co., Ltd. The company adheres to strict quality control standards in the design, manufacturing, and testing of their systems. Each component is carefully selected and assembled to meet industry standards, ensuring durability and performance under various operating conditions. Regular maintenance is also crucial for the optimal operation of the system. The company provides comprehensive maintenance services, including routine inspections, cleaning, and replacement of worn parts. By following a regular maintenance schedule, clients can extend the lifespan of their equipment and minimize the risk of breakdowns. Additionally, the company offers training programs for clients to ensure that operators are well-versed in the proper use and maintenance of the system, further enhancing its reliability and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top