

Principle of Anhydrous Sodium Sulfate Pneumatic Conveying System
Understanding the Anhydrous Sodium Sulfate Pneumatic Conveying System
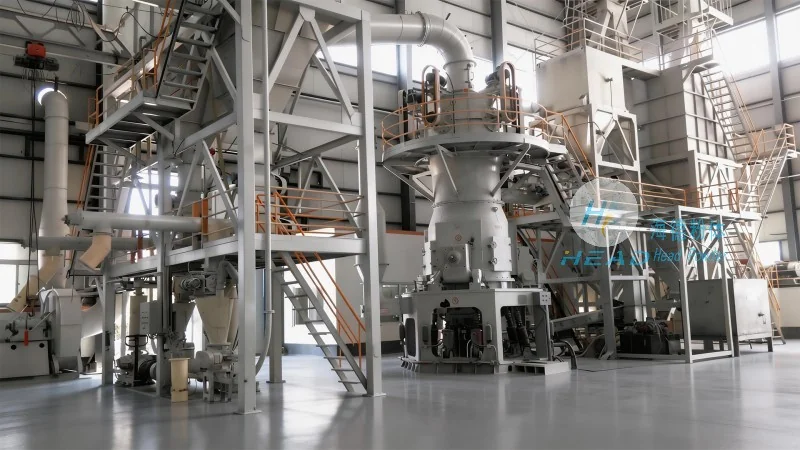
Introduction to the System
The anhydrous sodium sulfate pneumatic conveying system is a specialized industrial solution designed to transport bulk materials, specifically anhydrous sodium sulfate, through a pipeline using air or other gas as the conveying medium. This technology offers an efficient and reliable method for material handling, eliminating the need for traditional mechanical conveyors and reducing operational complexities in material transport processes.
Core Components and Functionality
The system comprises several key components that work in tandem to ensure smooth operation. The primary components include a material feeder, which accurately meters the anhydrous sodium sulfate into the conveying line; a gas source, typically a blower or compressor, that generates the necessary air pressure to move the material; a conveying pipeline network that transports the material from the source to the destination; and a separation and collection system that removes the material from the air stream at the end of the line.
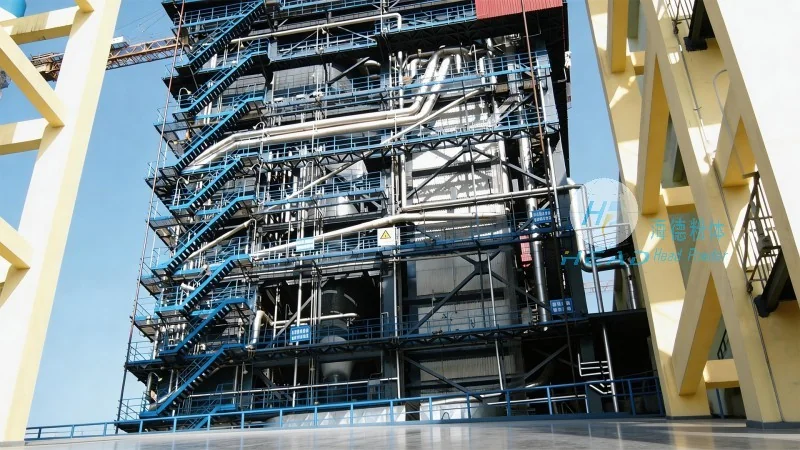
Working Principle of Pneumatic Conveying
The fundamental principle behind pneumatic conveying is the use of differential pressure to move particles through a pipeline. In the case of anhydrous sodium sulfate, the material is introduced into the pipeline at a controlled rate, and the gas source provides a steady flow of air. The air velocity is maintained above the minimum velocity required to keep the particles suspended, preventing them from settling or clogging the pipeline. As the material travels through the system, it is carried by the air stream until it reaches the receiving hopper or storage tank, where a separator (such as a cyclone or filter) captures the material and returns the air to the system for reuse.
Application Scenarios in Industrial Settings
This system is widely utilized in various industrial applications where the handling of anhydrous sodium sulfate is critical. For instance, in chemical manufacturing plants, the system can be integrated into production lines to transport raw materials or finished products between processing units. In mining and mineral processing facilities, it may be employed to move bulk anhydrous sodium sulfate from storage silos to processing equipment. Additionally, in food and pharmaceutical industries, where material purity and contamination control are paramount, the pneumatic conveying system ensures a clean and hygienic transport process.
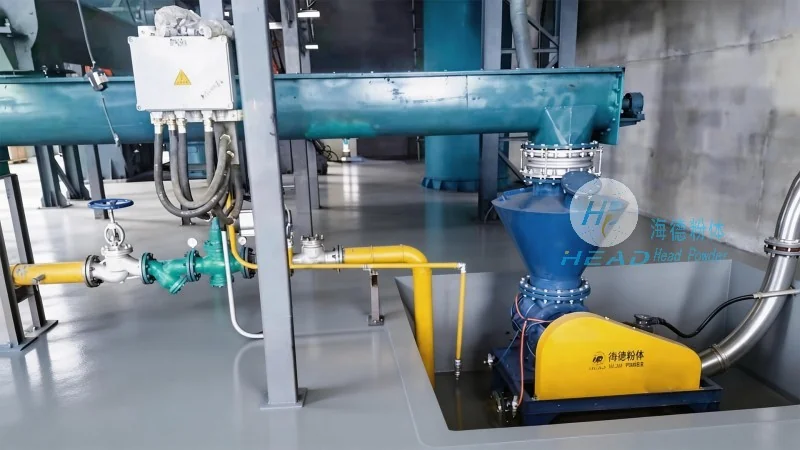
Advantages of the Pneumatic Conveying System
Compared to traditional mechanical conveyors, the anhydrous sodium sulfate pneumatic conveying system offers several advantages. Firstly, it eliminates the need for moving parts in the conveying line, reducing maintenance requirements and increasing system reliability. Secondly, the system is highly flexible, allowing for changes in material flow direction or destination without significant modifications. Thirdly, it provides better control over material flow rates and pressure, ensuring consistent and efficient transport. Furthermore, the system is more hygienic and dust-free, which is particularly important in industries where material contamination must be minimized. Lastly, the system can handle a wide range of particle sizes and moisture content, making it versatile for various applications.
HeadPowder: Expert Provider of Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of advanced pneumatic conveying systems, including those for anhydrous sodium sulfate. With years of experience in the engineering and manufacturing of material handling equipment, HeadPowder specializes in designing and installing customized systems that meet the specific needs of clients. The company is headquartered in Shandong, China, and leverages its expertise in mechanical engineering, fluid dynamics, and industrial automation to deliver high-quality, reliable, and efficient conveying solutions.
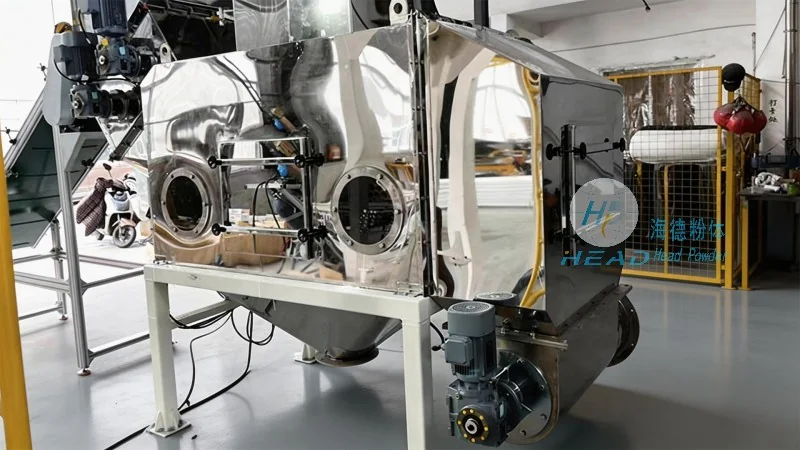
System Customization and Technical Support
HeadPowder understands that each industrial application has unique requirements, and therefore, the company offers comprehensive customization options for its pneumatic conveying systems. Clients can work with HeadPowder's engineering team to design a system that matches their specific material characteristics, production capacity, and operational environment. The company provides detailed technical support throughout the entire process, from system design and installation to maintenance and troubleshooting. This ensures that clients receive a system that is not only efficient but also easy to operate and maintain.
Conclusion: Reliable and Efficient Material Handling
The anhydrous sodium sulfate pneumatic conveying system, as provided by HeadPowder, represents a cutting-edge solution for bulk material transport. By leveraging the principles of pneumatic conveying, this system offers superior efficiency, reliability, and flexibility compared to traditional methods. With its robust design and comprehensive support, HeadPowder's systems are ideal for industries that require consistent and high-quality material handling solutions. Whether for chemical, mining, or food processing applications, the anhydrous sodium sulfate pneumatic conveying system from HeadPowder ensures that material transport is carried out safely, efficiently, and with minimal downtime.