With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
White sugar pneumatic conveying systems are critical in the sugar processing industry, enabling efficient and safe material handling. These systems utilize air to transport sugar from one location to another, offering advantages such as reduced contamination, improved hygiene, and enhanced operational flexibility. The classification of these systems is essential for understanding their design, functionality, and suitability for various industrial applications.
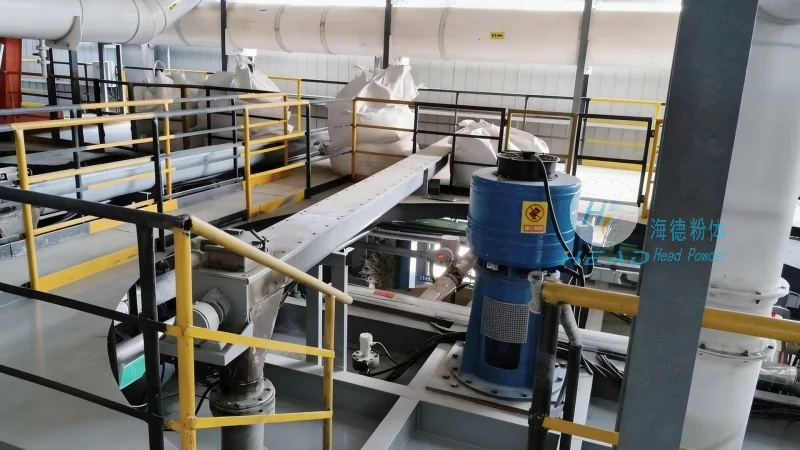
There are primarily two main categories of pneumatic conveying systems used in white sugar handling: pressure and vacuum systems. Each type has distinct characteristics and applications.
Pressure systems operate by forcing air or gas into a sealed pipeline, creating positive pressure that propels the sugar particles. These systems are suitable for long-distance and high-volume conveying, often used in large-scale sugar processing plants. They typically use high-pressure air compressors and can handle a wide range of sugar types, including granulated, powdered, and crystalline forms. The pressure system's design ensures minimal product degradation and maintains consistent flow rates, making it ideal for continuous production lines.
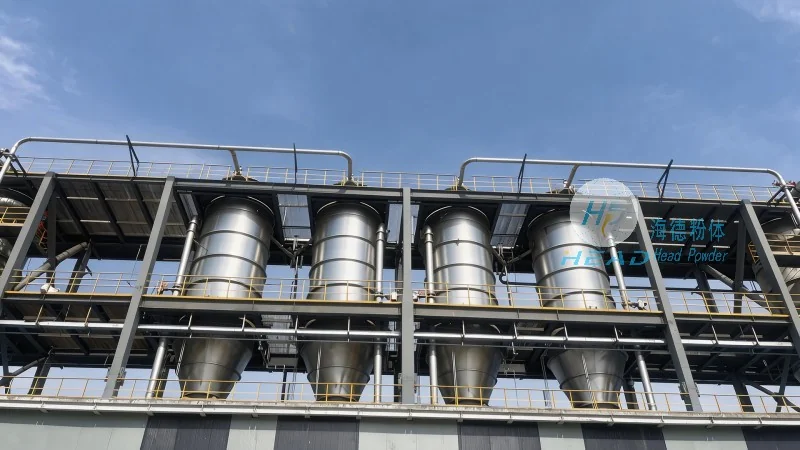
Vacuum systems, on the other hand, create a negative pressure environment by extracting air from the pipeline, drawing the sugar particles into the system. This method is commonly used for shorter distances and lower volume requirements. Vacuum systems are advantageous for handling sensitive or delicate sugar products, as they minimize mechanical stress and prevent product breakage. They are often employed in applications where the sugar needs to be transported from a lower elevation to a higher one or when the system must operate in a closed environment to maintain hygiene standards.
The application of white sugar pneumatic conveying systems varies based on the specific needs of the sugar processing facility. These systems are widely used in sugar refineries, where they facilitate the transport of raw sugar, intermediate products, and finished white sugar between processing stages. For instance, in a typical sugar refinery, the system may be used to convey raw sugar from storage silos to the refining equipment, then transport refined sugar to packaging lines. This seamless integration enhances production efficiency and reduces manual handling, which is crucial for maintaining product quality and safety.
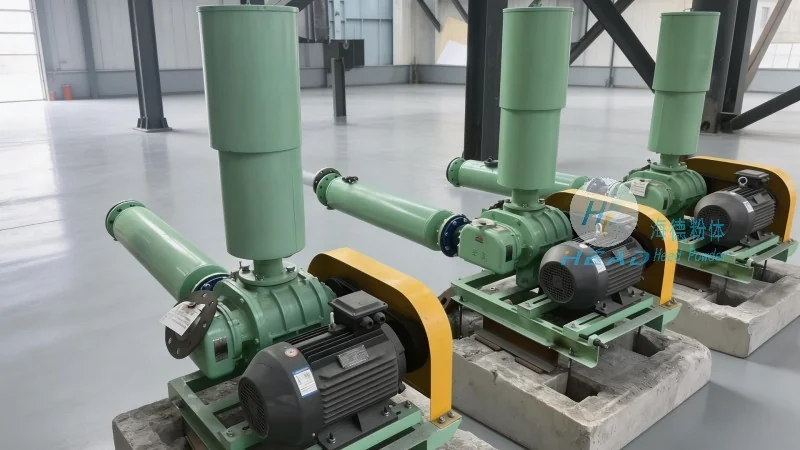
In addition to refinery operations, pneumatic conveying systems are also applied in sugar storage and distribution centers. They help in moving large quantities of white sugar from bulk storage tanks to packaging machines or loading vehicles. The systems ensure that the sugar remains in a controlled environment, preventing moisture absorption and contamination, which are critical factors in preserving the product's quality and shelf life. Furthermore, these systems are used in sugar blending operations, where different types of sugar or additives are mixed to create customized products, such as brown sugar or flavored syrups. The precise control offered by pneumatic conveying systems allows for accurate blending ratios, ensuring consistent product characteristics.
White sugar pneumatic conveying systems offer several key features that make them a preferred choice in the industry. One of the primary benefits is the ability to maintain product purity and hygiene. Unlike mechanical conveying methods, which may introduce contaminants or cause product degradation, pneumatic systems use enclosed pipelines and controlled air flow, minimizing the risk of cross-contamination. This is particularly important in food processing industries, where strict hygiene standards are mandatory.
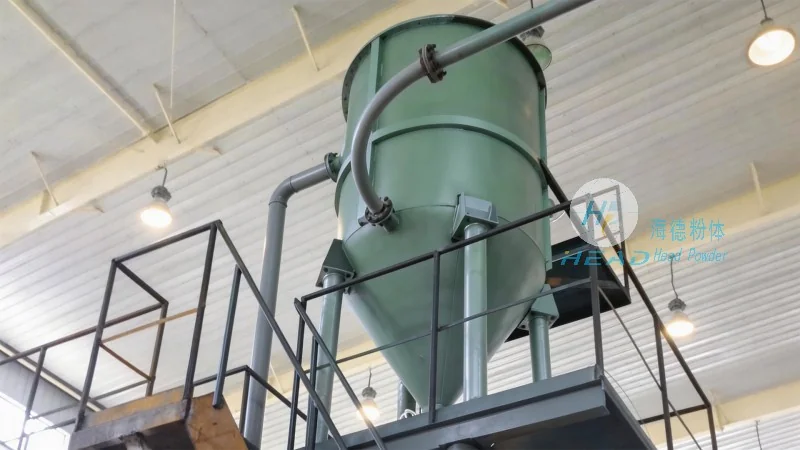
Another significant advantage is the energy efficiency and cost-effectiveness of these systems. By utilizing compressed air, the systems can transport large volumes of sugar with relatively low energy consumption compared to traditional methods like bucket elevators or belt conveyors. This results in lower operational costs and reduced environmental impact. Additionally, the systems are designed for easy maintenance and cleaning, which simplifies the overall operation and ensures compliance with regulatory requirements.
The flexibility and scalability of white sugar pneumatic conveying systems are also notable. These systems can be customized to accommodate varying production capacities and operational needs. Whether a small-scale operation or a large industrial facility, the systems can be adjusted to handle different sugar types and quantities. This adaptability makes them suitable for both new installations and retrofitting existing sugar processing plants. Furthermore, the systems can be integrated with other processing equipment, such as classifiers, separators, and packaging machines, creating a comprehensive material handling solution.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top