With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced foam powder conveying systems. These systems are engineered to efficiently transport bulk powders using a unique foam-assisted method, offering significant advantages over traditional conveying technologies. The company’s expertise lies in integrating innovative solutions that enhance material handling efficiency while ensuring minimal product degradation.
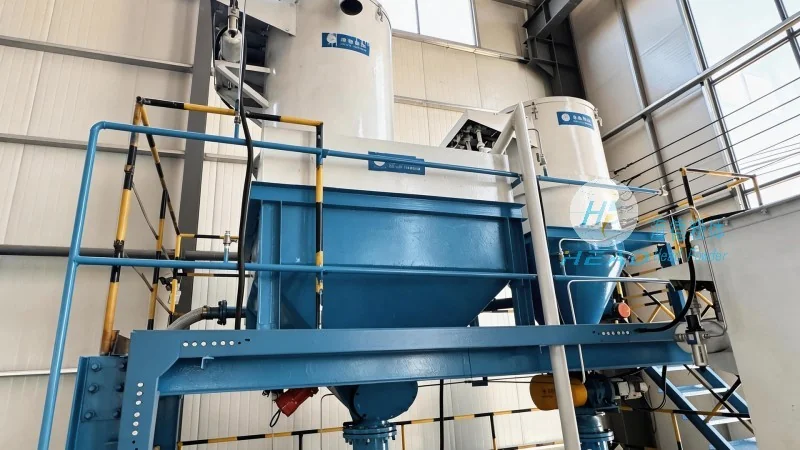
The foam powder conveyor system consists of several critical components that work in tandem to achieve effective material transport. At the core of the system is a foam generator, which produces a stable foam by mixing air with a liquid (typically water or a specialized solution). This foam is then introduced into a hopper or feeder containing the bulk powder. As the foam flows through the powder bed, it creates a fluidized state, reducing the particle-particle friction and allowing the powder to be carried through the conveying pipeline. The system also includes a control unit that regulates the foam-to-powder ratio, ensuring optimal conveying performance and preventing issues such as clogging or material degradation.
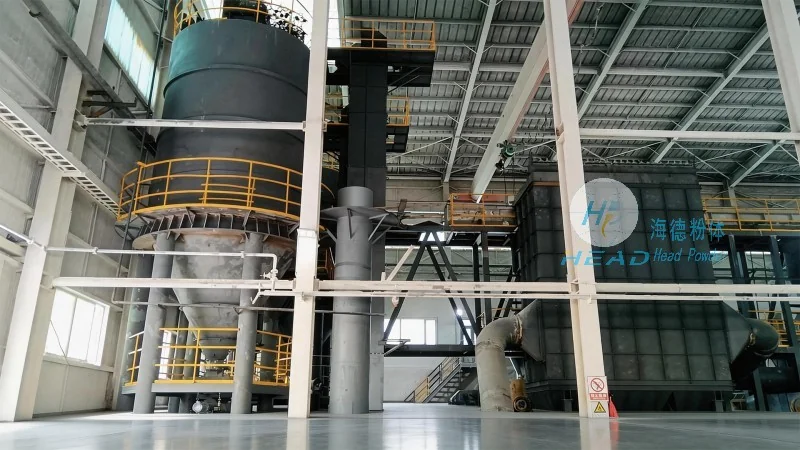
The operation of a foam powder conveyor begins with the preparation of the foam and the loading of the powder. First, the foam generator is activated, and the liquid is pumped to create a consistent foam. Simultaneously, the bulk powder is fed into the hopper. The foam then flows over the powder, creating a homogeneous mixture. This mixture is then drawn into the conveying pipeline by a vacuum or pressure system, depending on the specific design. The foam acts as a carrier, allowing the powder to be transported over long distances with minimal energy consumption. The process concludes when the foam-powder mixture reaches the destination, where the foam is separated (often by a separator or by allowing the foam to dissipate), leaving the powder in its original state. The system is designed to be automated, with sensors monitoring the foam and powder levels to maintain consistent performance.
HeadPowder’s foam powder conveying systems offer several advantages that make them ideal for various industrial applications. One of the primary benefits is the ability to transport fine or cohesive powders that are difficult to handle with traditional methods. The foam reduces particle friction, preventing agglomeration and ensuring a smooth flow. Additionally, the system minimizes product degradation, as the gentle conveying action reduces the risk of breakage or contamination. The energy efficiency of foam-assisted conveying is another key advantage, as it requires less power compared to other high-pressure systems. Furthermore, the flexibility of the system allows it to handle a wide range of powder types, from pharmaceuticals to food products, making it a versatile solution for diverse industries.
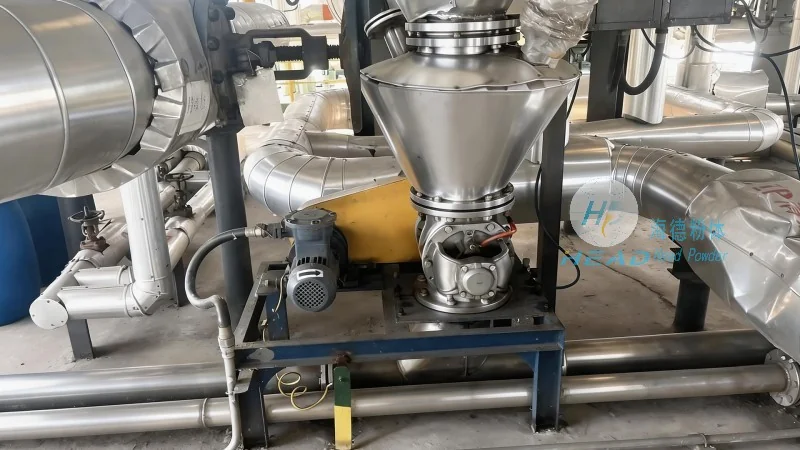
The foam powder conveyor technology developed by HeadPowder is widely used in various industrial sectors. In the pharmaceutical industry, it is employed to transport sensitive powders, ensuring compliance with stringent quality standards. The food industry utilizes these systems for handling dry ingredients, maintaining hygiene and preventing cross-contamination. The chemical industry also benefits from the ability to transport reactive or hazardous powders safely, as the foam reduces the risk of dust explosions and material exposure. Additionally, the system is used in the agricultural sector for handling fertilizers and other bulk agricultural products, improving efficiency in material handling and storage.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top