With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced powder handling solutions. The automatic tonne bag feeding powder material conveyor is a critical piece of equipment designed to efficiently transfer bulk powders from tonne bags into processing systems. This article delves into the operation process and underlying working principles of this equipment, highlighting its key components and operational flow.
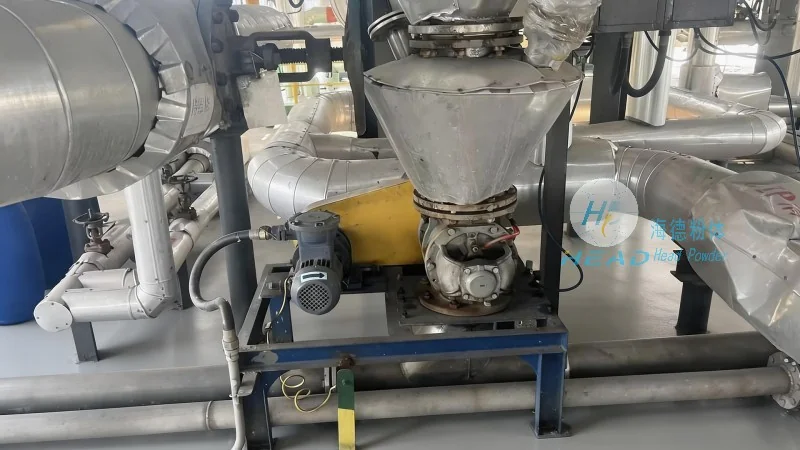
The automatic tonne bag feeding powder material conveyor consists of several essential components that work in tandem to ensure smooth material transfer. The primary parts include a tonne bag support frame, a discharge valve, a conveyor system (such as a screw or pneumatic conveyor), and a control panel. The tonne bag is securely placed on the support frame, which is typically equipped with a lifting mechanism to facilitate bag handling. The discharge valve is integrated into the bag to allow controlled release of the powder. The conveyor system, often a screw conveyor or a pneumatic system, transports the powder from the bag to the next stage of the processing line. The control panel manages the entire operation, including bag positioning, valve opening, and conveyor speed. Additionally, safety features like dust collection systems and emergency stop buttons are integrated to ensure operational safety and compliance with industrial standards.
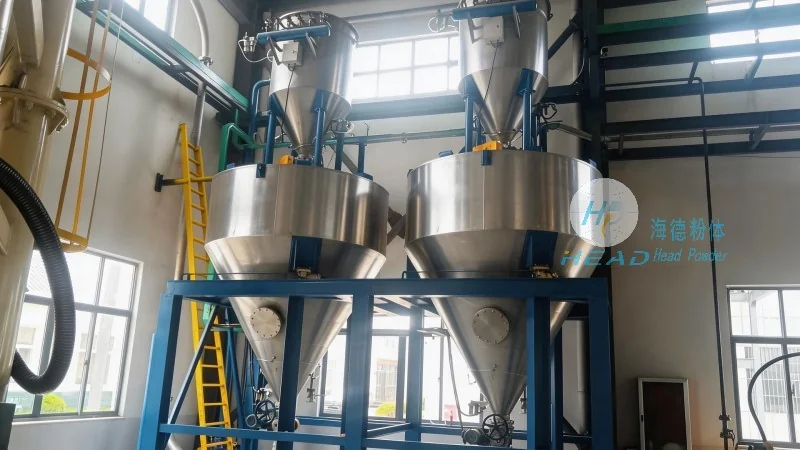
The operation of the automatic tonne bag feeding powder material conveyor follows a systematic sequence to ensure efficient and safe material transfer. The process begins with the placement of a filled tonne bag onto the support frame. The lifting mechanism may be used to adjust the bag height for proper alignment with the discharge valve, ensuring a secure and stable connection. Once the bag is positioned correctly, the control panel initiates the operation. The discharge valve opens, allowing the powder to flow out of the bag under gravity or assisted by a slight vacuum. Simultaneously, the conveyor system starts, transporting the powder from the bag to the receiving hopper or processing equipment. The control panel monitors the flow rate and adjusts the conveyor speed as needed to maintain a consistent feed rate, preventing overloading or underfeeding. The process continues until the tonne bag is empty. After the bag is emptied, the system may automatically move to the next bag or prepare for the next cycle, depending on the configuration. The entire sequence is designed to minimize downtime and maximize throughput, making it suitable for high-volume production environments.
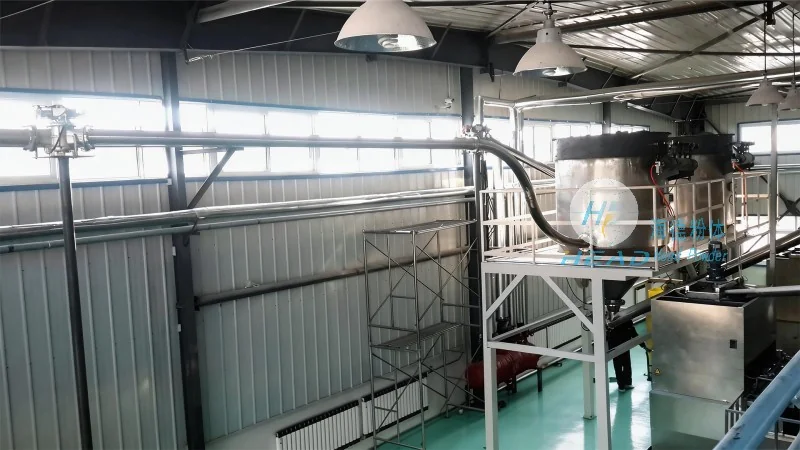
The working principle of the automatic tonne bag feeding powder material conveyor is based on mechanical and pneumatic systems that work together to control the flow of powder. The discharge valve, often a rotary valve or a pneumatic actuator, regulates the release of powder from the tonne bag. The conveyor system, such as a screw conveyor, uses rotating screws to push the powder forward, while a pneumatic conveyor uses compressed air to transport the powder. The control panel uses sensors and feedback mechanisms to monitor the system's performance, ensuring that the flow rate is consistent and the equipment operates safely. The entire system is designed to minimize dust generation and ensure that the powder is transferred without contamination, making it suitable for various industrial applications, including pharmaceuticals, food processing, and chemical manufacturing. The integration of sensors also allows for real-time monitoring of the bag's weight and the powder level, providing data for quality control and process optimization.
The automatic tonne bag feeding powder material conveyor offers several advantages, including high efficiency, reduced labor costs, and improved safety. It eliminates the need for manual handling of tonne bags, which can be hazardous and time-consuming, especially when dealing with heavy or difficult-to-handle bags. The equipment is also designed to handle a wide range of powder types, from fine powders to bulk materials, making it versatile for various industries. Applications include pharmaceutical manufacturing, where precise powder dosing is critical for product consistency and quality, food processing, where hygiene and safety are paramount to meet regulatory standards, and chemical production, where consistent material transfer is essential for maintaining product specifications and preventing contamination. The system's ability to integrate with existing processing lines also enhances operational flexibility and reduces the need for extensive modifications to current setups.
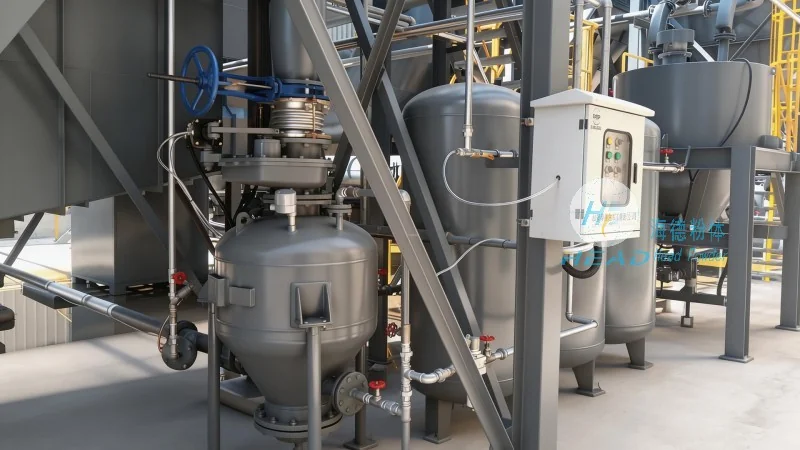
In conclusion, the automatic tonne bag feeding powder material conveyor is a sophisticated piece of equipment that plays a vital role in modern powder handling operations. By understanding its operation process and working principles, users can optimize its performance and ensure efficient, safe, and reliable material transfer. HeadPowder's expertise in designing and manufacturing such equipment ensures that clients receive high-quality solutions tailored to their specific needs, supporting their production goals and maintaining compliance with industry standards.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top