With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
The corn kernel pneumatic conveying machine is a specialized equipment designed for the efficient and dust-free transportation of corn kernels. It plays a crucial role in the agricultural and food processing industries, ensuring smooth material handling from storage to processing stages. This equipment is engineered to handle the unique characteristics of corn kernels, such as their size, density, and moisture content, while maintaining high efficiency and minimal product damage.
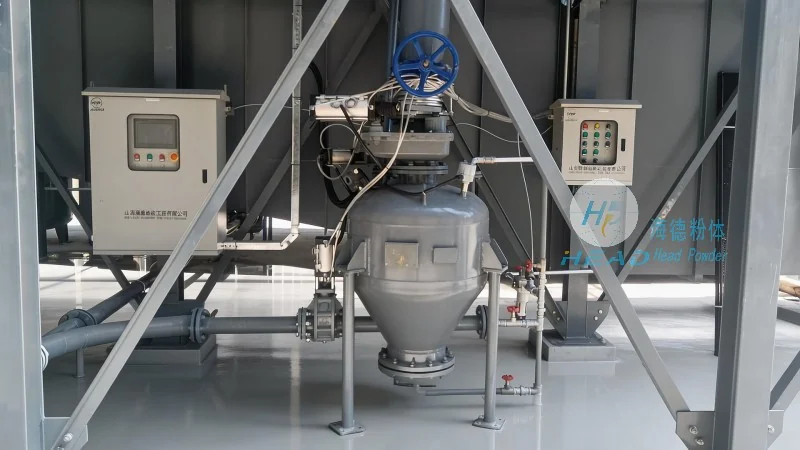
The core of the corn kernel pneumatic conveying machine is its pneumatic conveying system, which operates on the principle of air flow to move materials. The system typically consists of a hopper, a blower or air compressor, a pipeline network, and a discharge outlet. As corn kernels are fed into the hopper, the blower generates a high-pressure air stream that pulls the kernels into the pipeline. The air and material mixture travels through the pipeline to the discharge point, where the air is separated from the kernels, often using a cyclone separator or a filter system. This separation process allows the corn kernels to be collected in a clean and dry state, while the air is either recirculated or vented.
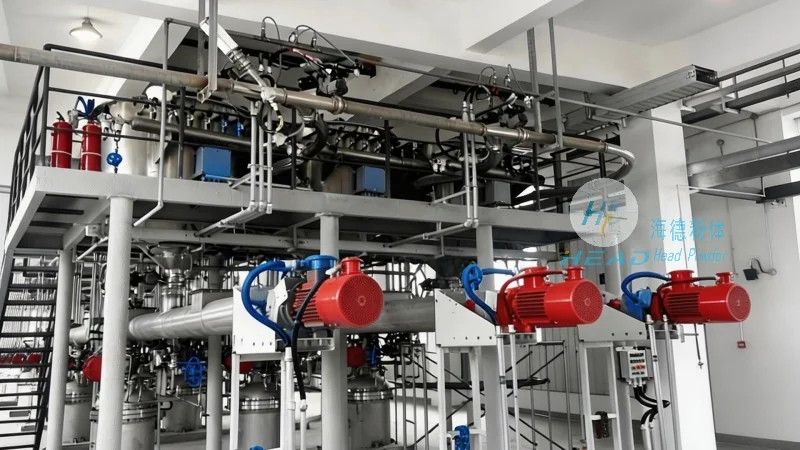
The operation of the corn kernel pneumatic conveyor involves several key steps that ensure optimal performance. First, the corn kernels are loaded into the hopper, which is equipped with a feeder to control the flow rate. The feeder ensures a consistent supply of material to the system, preventing overloading or underloading. Next, the blower is activated, creating a vacuum or pressure differential that draws the kernels into the pipeline. The air flow velocity is carefully controlled to maintain the kernels in a suspended state, preventing them from settling or damaging the equipment. As the mixture travels through the pipeline, it passes through any necessary components, such as bends or filters, which may be included to adjust the flow or remove impurities. Finally, at the discharge end, the air is separated from the kernels, and the kernels are collected in a storage bin or processing unit. The system may also include a pressure relief valve to prevent overpressure and a check valve to maintain the air flow direction.
The corn kernel pneumatic conveying machine offers several advantages over traditional mechanical conveyors. It provides a dust-free and hygienic environment, which is essential for food processing applications. The equipment is also capable of handling a wide range of material sizes and densities, making it versatile for different corn varieties. Additionally, the pneumatic system allows for long-distance transportation without the need for multiple transfer points, reducing the risk of product contamination and damage. These benefits make the corn kernel pneumatic conveyor suitable for various applications, including grain storage, milling, and animal feed production. It is particularly valuable in facilities where maintaining product quality and hygiene is paramount.
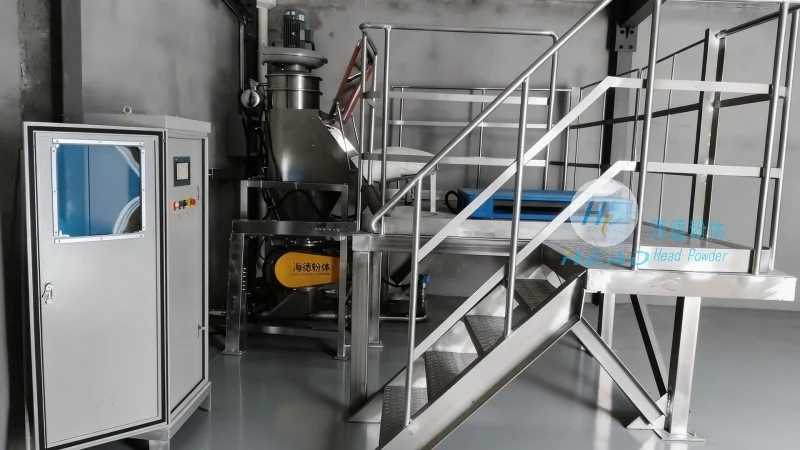
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of pneumatic conveying systems and related equipment. With a strong presence in China, particularly in Shandong, the company specializes in designing and producing high-quality corn kernel pneumatic conveyors tailored to the needs of the agricultural and food processing industries. HeadPowder's commitment to innovation and quality ensures that their products meet the highest standards of performance and reliability. By leveraging advanced engineering and manufacturing techniques, the company provides solutions that enhance efficiency and productivity in material handling processes. HeadPowder's expertise in pneumatic technology enables them to deliver customized equipment that addresses the specific challenges of corn kernel transportation, ensuring optimal results for their clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top