With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design and implementation of advanced pneumatic conveying systems tailored for flexible coke powder applications. This article explores the fundamental principles underlying such systems and highlights the key characteristics of their operational environments.
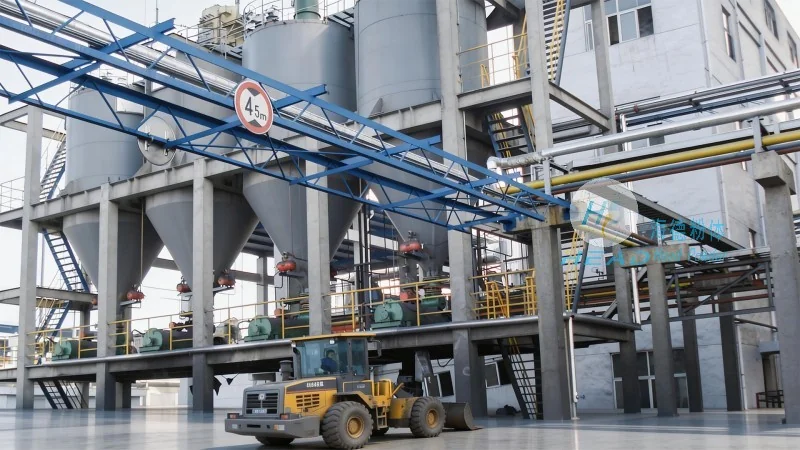
The pneumatic conveying system for flexible coke powder operates on the principle of transporting bulk materials through a pressurized or vacuumed air stream. Unlike traditional mechanical conveying methods, this system uses air as the medium to move the powder, offering advantages such as reduced equipment wear, lower maintenance costs, and the ability to handle materials in a dust-free environment. The system typically consists of a hopper for material storage, a conveyor line (often with multiple sections), and a receiver for the delivered material. The flexibility in design allows for adaptation to various production line configurations, ensuring efficient material flow from source to destination.
The operational environment of a flexible coke powder pneumatic conveying system is characterized by several critical factors that influence its performance and reliability. First, the system is designed to handle the specific properties of coke powder, including its particle size, moisture content, and flowability. These characteristics are crucial as they determine the air velocity and pressure required for effective transport. For instance, finer particles may necessitate higher air velocities to prevent clogging, while cohesive materials might require additional measures like vibration or air agitation to maintain flow.
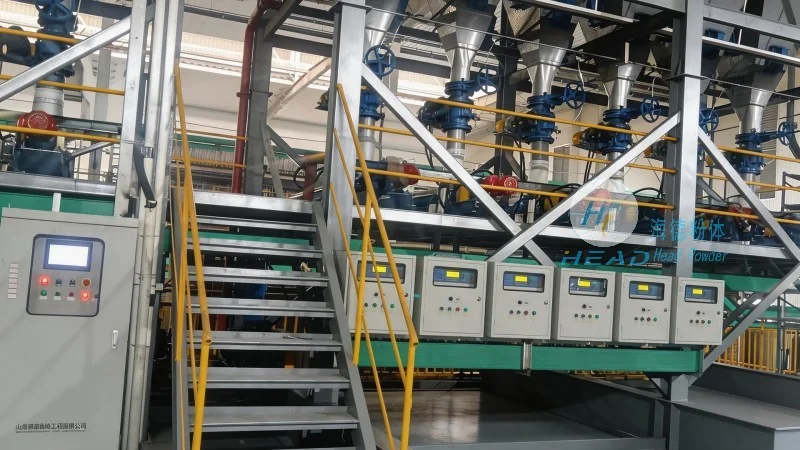
Second, the system's flexibility in layout is a significant advantage, enabling it to integrate seamlessly into existing industrial setups. This adaptability is particularly valuable in manufacturing plants where space constraints and production flow requirements vary. The modular design of the conveying system allows for easy expansion or reconfiguration, accommodating changes in production volume or material types without extensive modifications. Additionally, the system's ability to operate in both positive and negative pressure modes provides versatility in handling different material transfer scenarios, whether from a central storage to multiple processing units or from various production points to a central collection point.
Flexible coke powder pneumatic conveying systems are widely applied in various industrial sectors, including steel production, chemical processing, and power generation. In steel mills, for example, these systems are essential for transporting coke powder from storage silos to blast furnaces, ensuring a continuous and efficient supply of raw materials. The system's ability to maintain a consistent material flow rate is critical in maintaining the operational efficiency of the blast furnace, as any disruption can lead to production delays or equipment damage.
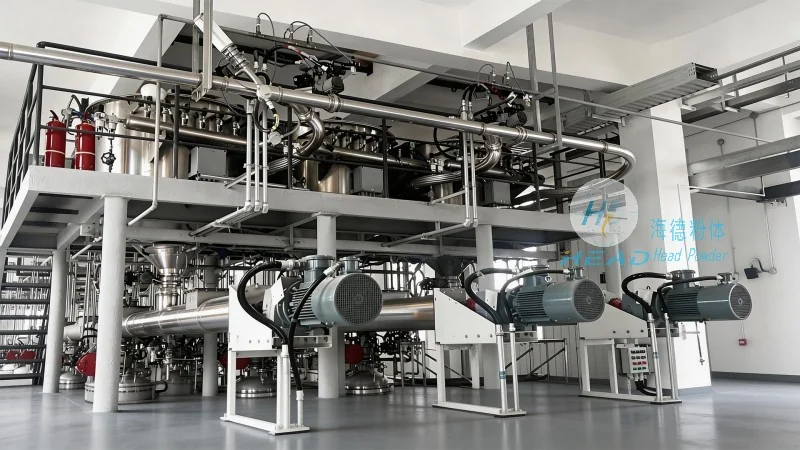
In chemical plants, the system is used to convey coke powder for use in the production of chemicals, such as carbon black or other industrial chemicals. The dust-free operation of the pneumatic system minimizes the risk of contamination and improves product quality, which is vital in chemical manufacturing where purity standards are stringent. Furthermore, the system's low maintenance requirements and energy efficiency contribute to cost savings over time, making it a preferred choice for long-term material handling solutions.
Compared to traditional mechanical conveying methods, flexible coke powder pneumatic conveying systems offer several technical advantages. The primary benefit is the reduction in equipment wear and tear, as the material is conveyed through pipes rather than being subjected to mechanical friction. This results in longer equipment lifespan and lower replacement costs. Additionally, the system's ability to handle abrasive materials like coke powder without significant wear is a significant advantage, as mechanical conveyors often require frequent maintenance or replacement of components.
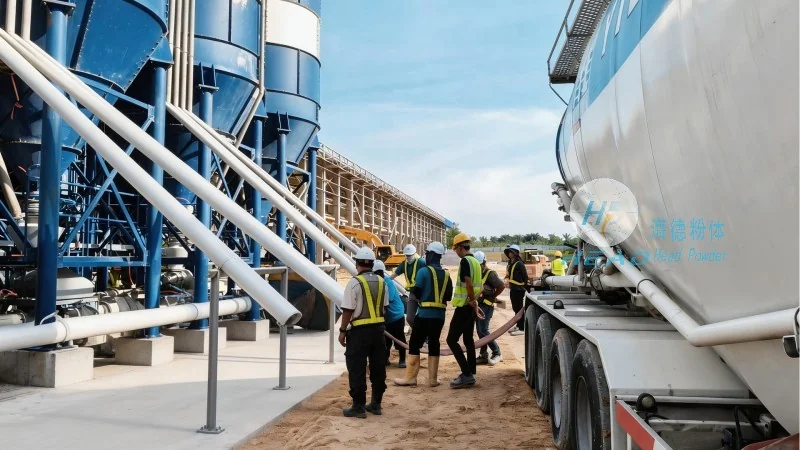
The performance of the system is typically evaluated based on several metrics, including the conveying capacity (measured in tons per hour), the pressure drop across the system, and the energy consumption per unit of material conveyed. High-efficiency systems are designed to minimize pressure drop and energy usage, ensuring optimal performance while reducing operational costs. The system's flexibility in terms of material handling also allows for the integration of sensors and control systems, enabling real-time monitoring and adjustment of operational parameters to maintain optimal performance under varying conditions.
Flexible coke powder pneumatic conveying systems represent a sophisticated solution for efficient material handling in industrial applications. By leveraging the principles of pneumatic transport, these systems offer reliable, low-maintenance, and adaptable solutions for transporting coke powder in various industrial settings. HeadPowder, with its expertise in engineering and manufacturing, provides customized solutions tailored to the specific needs of clients, ensuring optimal performance and operational efficiency. With a focus on innovation and quality, HeadPowder continues to be a trusted partner in the development of advanced material handling systems for the coke and related industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top