With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling solutions. Among their portfolio is the tonne bag breakage material pneumatic conveying system, a technology that efficiently processes bulk materials from large, breakable bags. This system combines mechanical and pneumatic principles to ensure reliable material transport, making it ideal for various industrial applications.
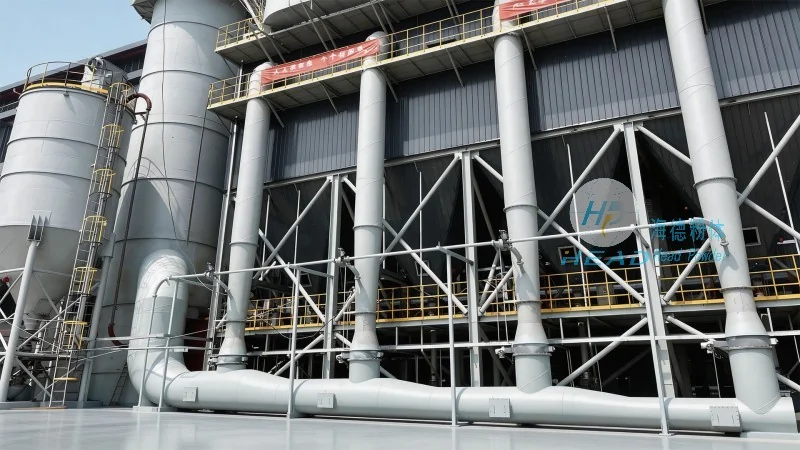
The core principle of the tonne bag breakage material pneumatic conveying system revolves around the controlled breakdown of tonne bags and subsequent transport of the liberated material through an air stream. The process begins with the placement of a large tonne bag, typically containing bulk powders or granules, onto a specialized hopper or feeder. The system then uses a combination of mechanical forces—such as a rotating breaker or impact plate—to rupture the bag, allowing the contents to fall into the hopper. Simultaneously, a high-pressure air compressor generates a powerful air flow that draws the material into the conveying pipeline. The material is then carried through the pipeline by the air current, with the system’s design ensuring minimal loss and maximum efficiency. The air stream is carefully regulated to maintain consistent velocity, preventing material segregation or blockages. This integrated approach ensures that the entire process—from bag opening to material delivery—is automated and reliable.
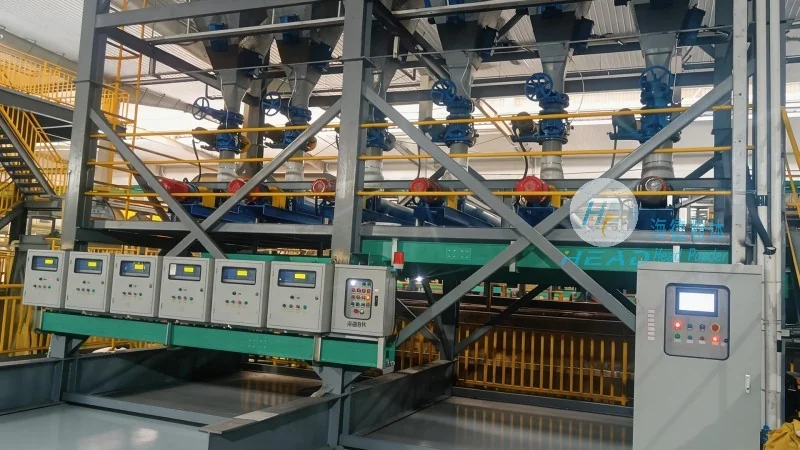
Several critical components work in tandem to ensure the system operates effectively. The bag breaker is the primary device responsible for opening the tonne bag, with options including rotating blades, impact plates, or hydraulic systems, depending on the material’s hardness and bag type. The hopper or feeder serves as the storage and feeding unit, where the broken material is collected before being introduced into the conveying line. The air compressor is a high-capacity unit that generates the necessary air pressure to drive the material through the pipeline, with adjustable settings to match the material’s flow characteristics. The conveying pipeline itself is typically made of durable materials like stainless steel or PVC, designed to withstand the abrasive nature of the material and the air pressure. Additionally, the system includes a filter and dust collection unit to manage air quality and prevent contamination, ensuring compliance with industrial safety standards. Each component is engineered to work seamlessly together, minimizing downtime and maximizing productivity.
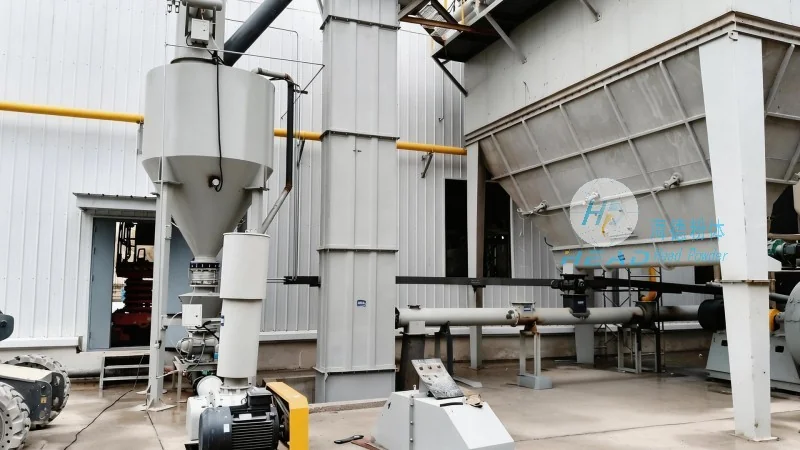
The tonne bag breakage material pneumatic conveying system is particularly suited for industrial environments where large quantities of bulk materials are handled. Its key working scene characteristics include high material throughput, which allows for efficient processing of large batches, and low maintenance requirements, as the system is designed with durable components that resist wear and tear. The system is also adaptable to various material types, including powders, granules, and even fibrous materials, making it versatile for different industries. In terms of operational flexibility, the system can be integrated with existing production lines, allowing for smooth transitions and minimal disruption. The automated nature of the process reduces the need for manual labor, enhancing safety and efficiency. Additionally, the system’s compact design makes it suitable for both new installations and retrofitting into existing facilities, providing a cost-effective solution for material handling needs.
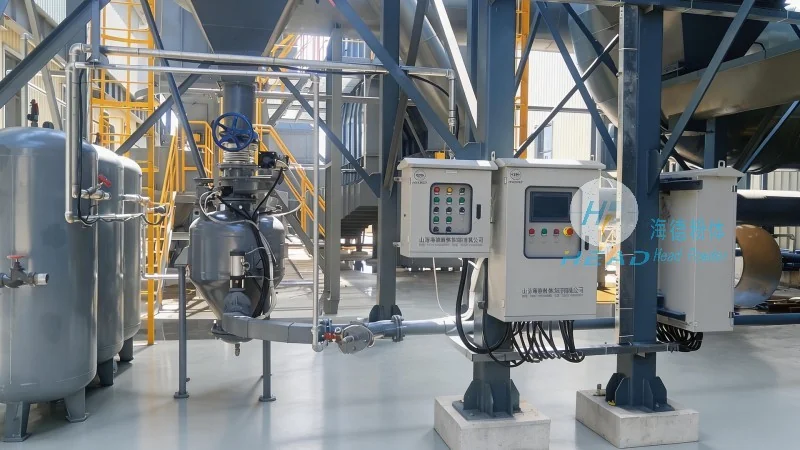
HeadPowder’s tonne bag breakage material pneumatic conveying system finds applications across multiple industries, including food processing, pharmaceuticals, chemicals, and mining. In the food industry, the system is used to handle ingredients like flour, sugar, and spices, ensuring hygienic and efficient processing. The pharmaceutical sector benefits from the system’s ability to transport sensitive materials without contamination, maintaining product quality and safety standards. In the chemical industry, the system efficiently handles bulk chemicals, reducing the risk of spills and improving operational safety. The mining industry utilizes the system to transport raw materials like ores and minerals, improving material flow and reducing handling costs. The overall benefits of this system include increased productivity, reduced labor costs, and improved material quality, making it a valuable asset for any industrial operation.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top