With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of industrial material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems. This article delves into the fundamental principles behind bulk material pneumatic conveying machines, particularly those used in silo applications, and explores the key characteristics that define their operational effectiveness across various industrial settings.
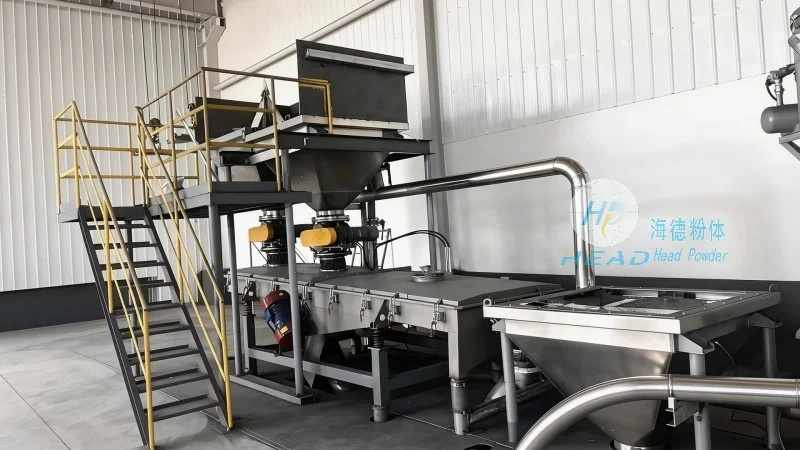
The fundamental principle of pneumatic conveying systems involves the use of pressurized air or suction to transport bulk materials from one location to another. In the context of silo-based applications, these systems are engineered to efficiently move powders, granules, and other particulate materials from storage silos to processing units, packaging lines, or other destinations within a facility. The process typically relies on either positive pressure (where air is forced through the material) or negative pressure (where air is drawn away from the material), with the choice of method depending on factors such as material properties, distance, and system layout.
At the heart of a silo pneumatic conveying machine is the hopper or feeder, which feeds material into the conveying line. The material is then entrained by the moving air stream, which carries it through the pipeline to the discharge point. Key components include the air compressor or vacuum pump, the conveying line (often made of stainless steel or other corrosion-resistant materials), and the control system that regulates pressure, flow, and material transport. The efficiency of the system is determined by factors like air velocity, material density, and the design of the hopper and discharge nozzle.
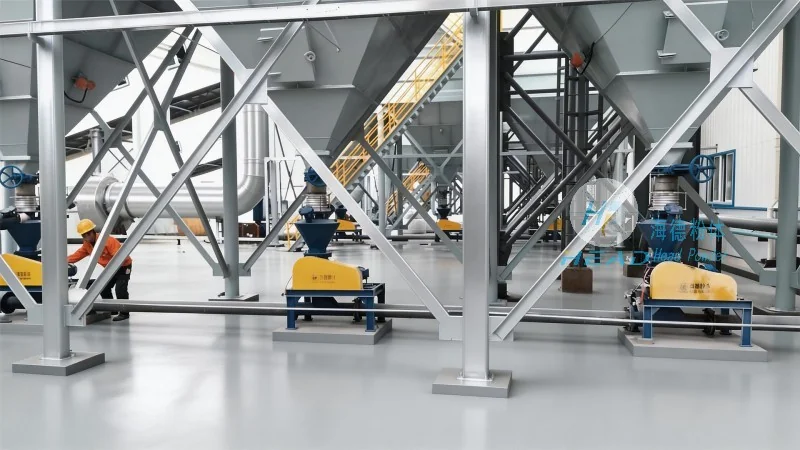
Industrial applications of silo pneumatic conveying machines span a wide range of sectors, including food processing, pharmaceuticals, chemicals, and minerals. The working scene characteristics of these systems are tailored to meet the specific demands of each industry, ensuring optimal performance and material integrity. For instance, in the food industry, systems must adhere to strict hygiene standards, often incorporating stainless steel construction and easy-to-clean components to prevent contamination. In contrast, chemical processing applications may require specialized materials to resist corrosion from aggressive substances.
One of the primary characteristics is the ability to handle a diverse range of materials, from fine powders to coarse granules, with minimal degradation or segregation. This versatility is achieved through the design of the conveying line and the control of air flow, which ensures that materials are transported without clumping or bridging. Additionally, the systems are designed to minimize material loss and dust generation, which is critical for maintaining a clean and safe working environment.
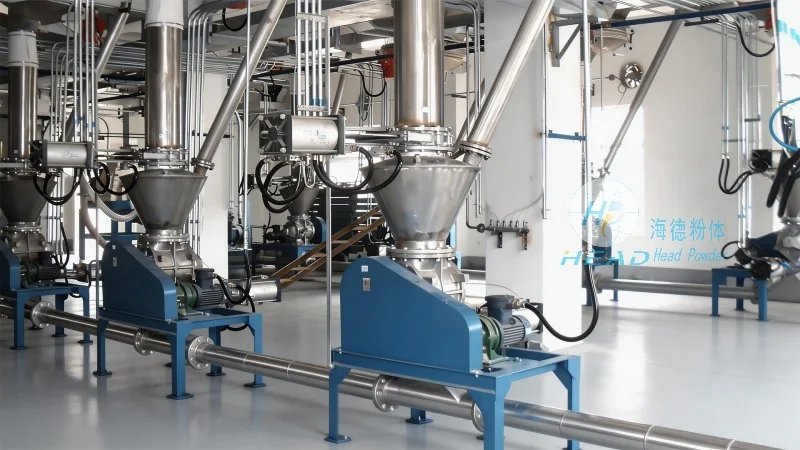
Silo pneumatic conveying machines offer several operational advantages that make them a preferred choice in many industrial settings. These include high efficiency in material transport, reduced labor costs compared to manual handling, and the ability to operate in hazardous environments where traditional mechanical conveyors may pose safety risks. The systems are also highly adaptable, allowing for easy integration with existing silo infrastructure and processing lines.
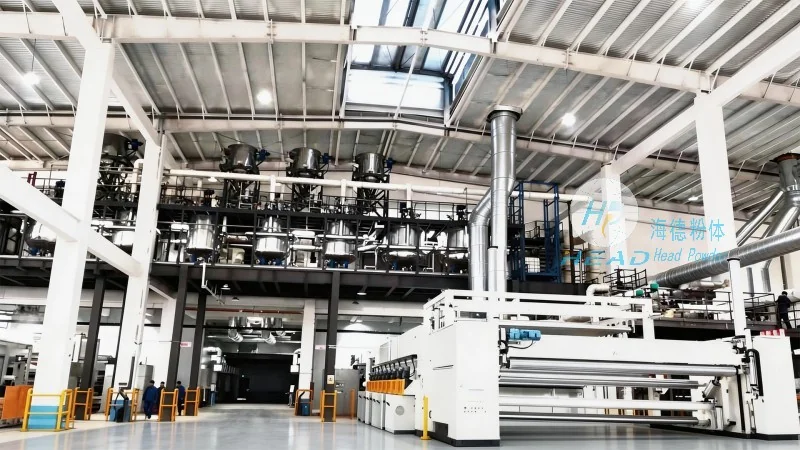
In practical applications, these machines are commonly used in scenarios such as transferring raw materials from storage silos to production lines, transporting finished products from packaging stations to storage areas, or moving waste materials for disposal. The flexibility of the system allows for changes in material flow rates and destinations without significant modifications to the equipment, making it a cost-effective solution for dynamic industrial operations.
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted partner in the design and implementation of advanced pneumatic conveying solutions for silo applications. With a focus on innovation and customer-centric design, the company provides tailored systems that meet the unique requirements of each industrial client. By leveraging decades of experience in material handling technology, HeadPowder ensures that its pneumatic conveying machines deliver reliable performance, enhanced safety, and improved operational efficiency across various working scenes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top