With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
When it comes to handling and transporting corn kernels, selecting the right conveying method is crucial for efficiency, cost-effectiveness, and product integrity. The choice of system can significantly impact production lines in agricultural processing facilities, feed mills, and food manufacturing operations. This article explores common corn kernel conveying methods and highlights the advantages of HeadPowder's specialized pneumatic conveying solutions for corn kernels.
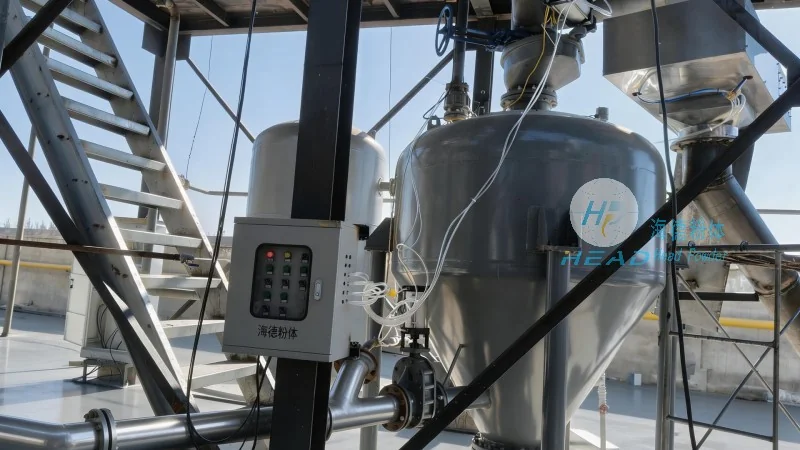
Traditional corn kernel conveying often relies on mechanical systems such as belt conveyors, screw conveyors, and bucket elevators. These methods are widely used due to their simplicity and reliability. Belt conveyors use a continuous belt to move kernels horizontally or at a slight incline, making them suitable for long-distance horizontal transport. Screw conveyors, or augers, are effective for vertical or inclined transport, utilizing a rotating helical screw to push kernels forward. Bucket elevators, on the other hand, lift kernels vertically using buckets attached to a chain or belt, ideal for vertical movement in processing plants.
While mechanical systems are common, they come with several limitations that can affect operational efficiency and product quality. One major drawback is the risk of kernel breakage or damage during transport, which can reduce product value and increase waste. Additionally, mechanical systems often require more maintenance and have higher energy consumption compared to pneumatic alternatives. Dust generation is another concern, as loose kernels can create airborne particles that pose health and safety risks in processing environments. These challenges highlight the need for more advanced and efficient conveying solutions.
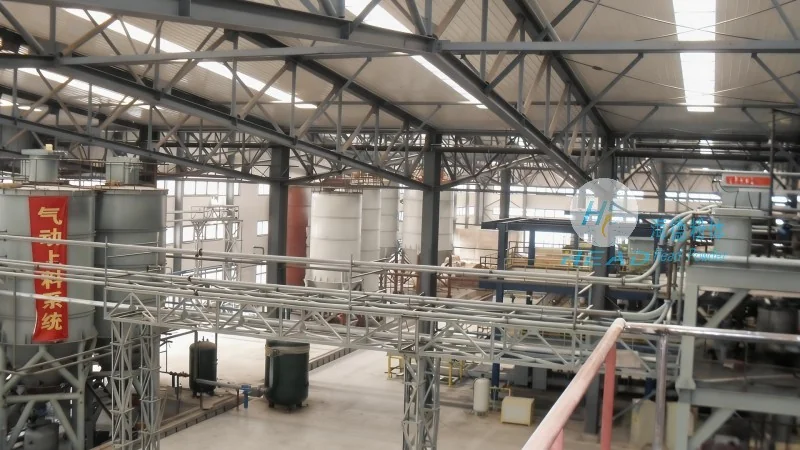
HeadPowder, a leading provider of engineering solutions in China, offers a state-of-the-art pneumatic conveying system specifically designed for corn kernel transport. The system leverages air pressure to move kernels through a network of pipes, eliminating the need for mechanical components that can cause damage or require frequent maintenance. The HeadPowder corn kernel pneumatic conveying system is engineered to handle the unique characteristics of corn kernels, ensuring minimal breakage and preserving product quality throughout the conveying process. With its headquarters in Shandong, China, HeadPowder combines advanced technology with local expertise to deliver tailored solutions for agricultural processing industries.
One of the primary advantages of HeadPowder's corn kernel pneumatic conveying system is its ability to reduce product damage. Unlike mechanical systems that rely on friction and physical contact, pneumatic transport uses air to gently move kernels, minimizing the risk of breakage or abrasion. This is particularly important for corn kernels, which are sensitive to handling and can lose nutritional value or market value if damaged. The system also offers improved hygiene and dust control, as the enclosed piping system prevents airborne particles from contaminating the product or the environment. This is a significant benefit for food processing facilities, where maintaining high standards of cleanliness is essential.
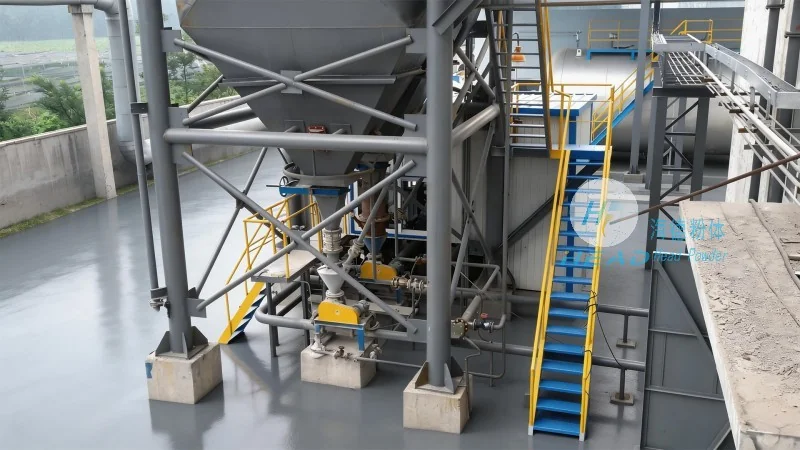
HeadPowder's pneumatic conveying system is designed for high efficiency and cost-effectiveness. The system uses less energy compared to traditional mechanical conveyors, as it relies on air pressure rather than motor-driven components. This reduces operational costs and contributes to lower energy consumption over time. Additionally, the system's compact design allows for easier integration into existing production lines, minimizing downtime and installation costs. The ability to transport kernels over long distances without intermediate handling points further enhances operational efficiency, reducing labor costs and improving overall productivity.
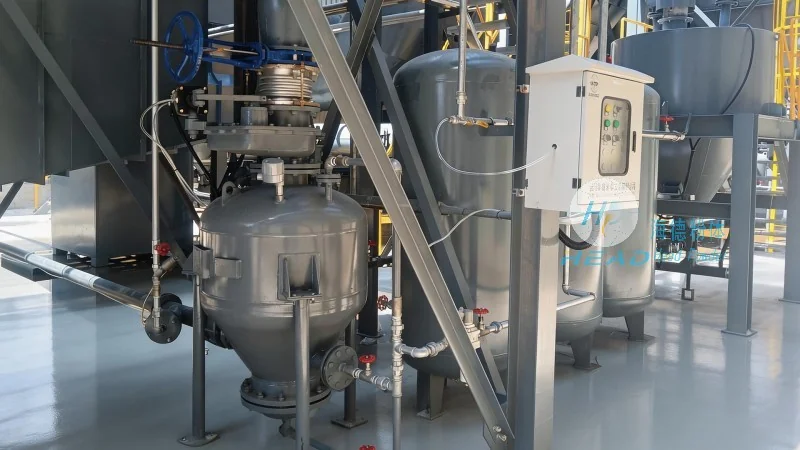
HeadPowder understands that different processing facilities have unique requirements. The corn kernel pneumatic conveying system is highly customizable to meet specific operational needs. The system can be configured for various distances, flow rates, and kernel types, ensuring optimal performance for each application. Whether a facility needs to transport kernels from a storage silo to a processing line or between different processing stages, the system can be tailored to fit the exact requirements. This versatility makes it suitable for a wide range of applications, from small-scale feed mills to large-scale food processing plants.
Reliability is a top priority for HeadPowder's pneumatic conveying system. The system is built with high-quality components that are designed to withstand the demands of continuous operation in industrial environments. The enclosed piping system reduces the risk of leaks and contamination, while the air filtration and cleaning systems maintain optimal performance. Regular maintenance is minimal compared to mechanical systems, as there are fewer moving parts that require attention. HeadPowder provides comprehensive support, including maintenance services and spare parts, ensuring that the system operates at peak efficiency throughout its lifespan.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top