With more than 10‑year industry experience, Shandong Headpowder delivers full‑service pneumatic‑conveying systems and blowers, undertaking nationwide turn‑key powder‑handling projects.
HeadPowder, a leading provider of material handling solutions, specializes in advanced vacuum conveying systems designed to meet diverse industrial needs. This article explores the fundamental principles of negative pressure vacuum material conveying and highlights key application scenarios where this technology excels in transporting powders and granules efficiently and safely.
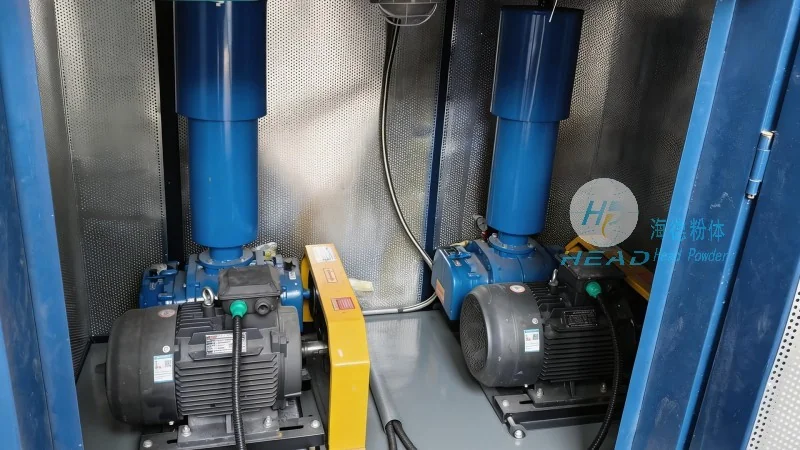
Negative pressure vacuum conveying operates on the principle of creating a pressure differential between the material source and the receiving container. By generating a vacuum in the conveying line, the system draws material from the source into the vacuum chamber. The vacuum is typically created using a vacuum pump, which reduces the pressure inside the line below atmospheric pressure. As a result, the material is drawn into the system due to the pressure difference. This method is particularly effective for handling fine powders and granules that are prone to dust and clogging in traditional positive pressure systems.
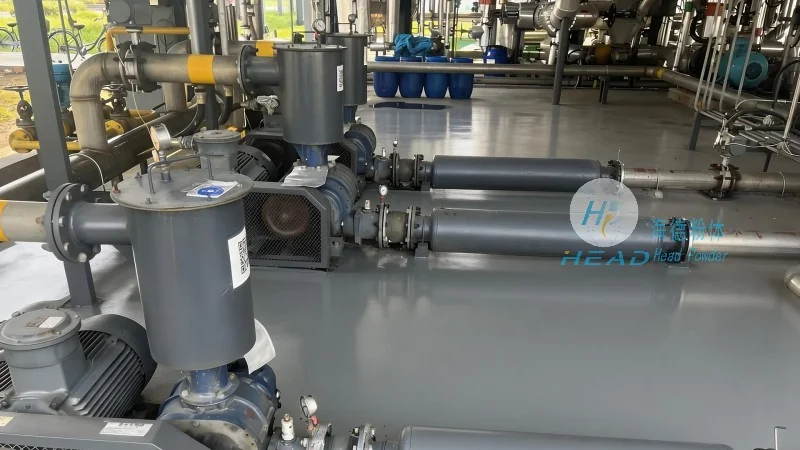
One of the primary benefits of negative pressure vacuum conveying is its ability to minimize dust generation and exposure. The sealed system prevents particles from escaping into the environment, enhancing workplace safety and compliance with environmental regulations. Additionally, this method reduces product contamination by keeping the material contained within the system, which is crucial for sensitive or high-value products. The low operating noise and energy efficiency of vacuum pumps also contribute to a more sustainable and cost-effective operation.
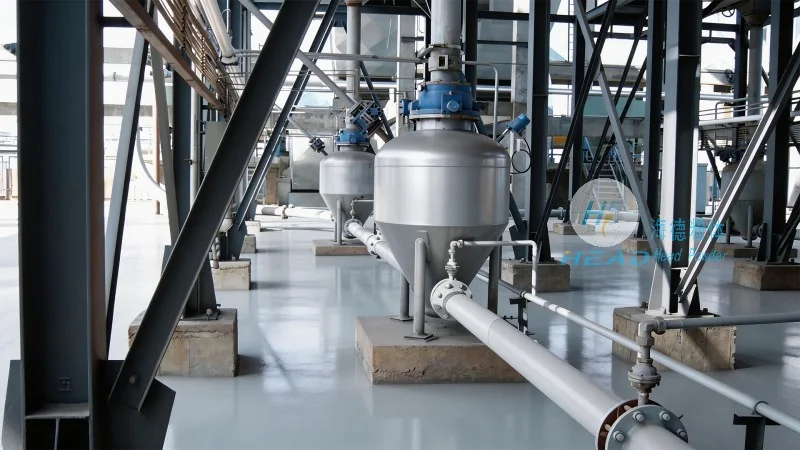
HeadPowder's negative pressure vacuum conveying systems are widely used in various industrial sectors. In the pharmaceutical industry, these systems are essential for transporting sterile powders and granules, ensuring that the materials remain uncontaminated during handling. The food processing sector also benefits from this technology, as it allows for the safe and hygienic transfer of powders like flour, sugar, and spices. In the chemical industry, negative pressure vacuum conveying is used to handle hazardous powders, providing a safe method to transport materials without exposing workers to dangerous substances. Furthermore, in the agricultural sector, these systems are employed to convey bulk materials such as seeds, fertilizers, and grains, improving efficiency in storage and processing operations.
HeadPowder understands that each industrial application has unique requirements. Therefore, their negative pressure vacuum conveying solutions are highly customizable to fit specific operational needs. The systems can be integrated with existing production lines, allowing for seamless material transfer without disrupting current workflows. This flexibility ensures that businesses can adapt to changing production demands while maintaining optimal performance. Additionally, the company offers comprehensive support, including installation, maintenance, and technical assistance, to ensure that clients achieve the best results from their vacuum conveying systems.
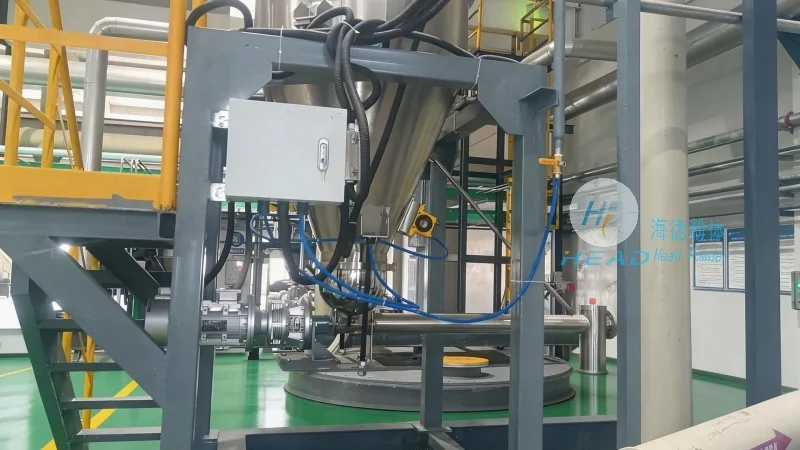
Negative pressure vacuum material conveying is a reliable and efficient method for transporting powders and granules in various industrial applications. By leveraging the principles of vacuum technology, these systems provide a safe, clean, and cost-effective solution for material handling. HeadPowder, with its expertise and commitment to quality, continues to provide advanced vacuum conveying solutions that meet the evolving needs of industries worldwide. Whether in pharmaceuticals, food processing, chemicals, or agriculture, HeadPowder's negative pressure vacuum conveying systems offer a robust and adaptable approach to material transport.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Zhangqiu District, Jinan City, Shandong Province, China

telephone
WeChatconsult
top