

Principle and Application Characteristics of Vacuum Suction Type Powder Conveying Systems
HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder conveying solutions. This article delves into the fundamental principles of vacuum suction type powder conveying systems and highlights their unique application characteristics across various industries.
Understanding the Vacuum Suction Principle
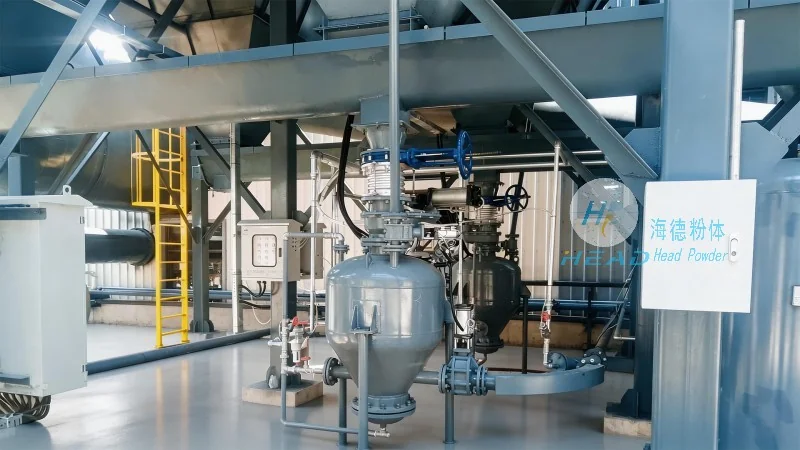
Vacuum suction type powder conveying systems operate on the principle of creating a negative pressure environment within the conveying line. By generating a vacuum, these systems draw powder materials from the source to the destination without the need for mechanical pressure or direct contact with the material. The process involves a series of components, including a vacuum pump, conveying pipes, and a control unit, which work in tandem to ensure efficient and reliable powder transport.
Key Components and Operational Mechanism
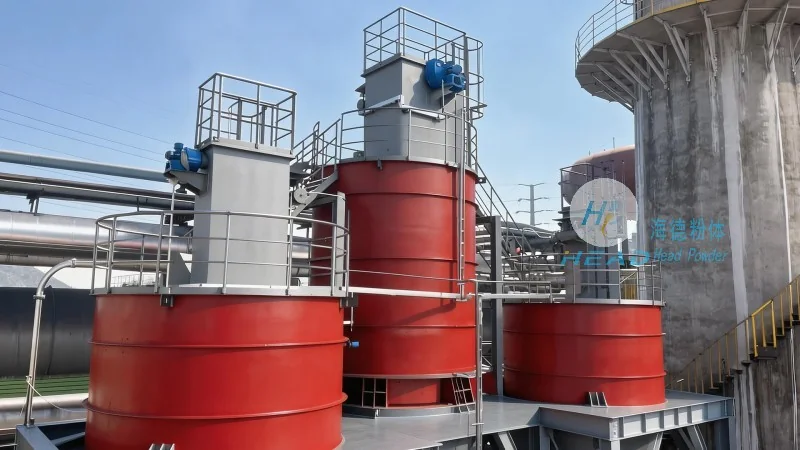
The core components of a vacuum suction system include a vacuum pump, which provides the necessary suction force; conveying hoses or pipes that transport the powder; a filter system to prevent dust and particles from escaping; and a control panel for monitoring and adjusting the system's performance. The operational mechanism begins with the vacuum pump creating a low-pressure zone in the system. As the pump operates, it draws air and powder particles from the source container into the conveying line. The powder is then carried through the pipes by the induced airflow, while the air is filtered and released back into the environment. This method ensures that the powder is transported without the need for manual handling or mechanical agitation, reducing the risk of contamination and material degradation.
Application Characteristics in Different Industries
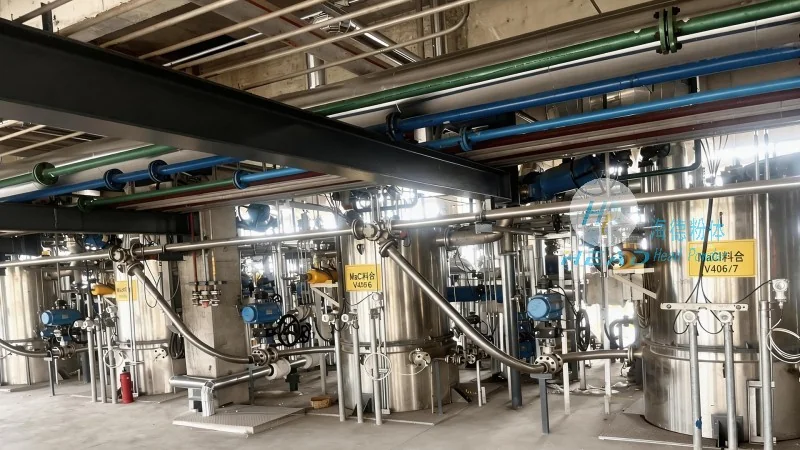
Vacuum suction type powder conveying systems are widely used across multiple sectors due to their versatility and efficiency. In the chemical industry, these systems are ideal for handling fine powders such as pigments, catalysts, and reagents, where maintaining product purity is critical. The negative pressure environment minimizes dust exposure and prevents cross-contamination, making it suitable for sensitive chemical processes. In the food and pharmaceutical industries, the system's ability to handle hygienic materials is paramount. The enclosed design and filtration capabilities ensure that powders like flour, sugar, or active pharmaceutical ingredients (APIs) are transported in compliance with stringent hygiene standards. Additionally, the system's gentle handling reduces product agglomeration and maintains the integrity of the material, which is essential for maintaining product quality and shelf life.
Advantages and Benefits of Vacuum Suction Systems
Compared to traditional positive pressure or mechanical conveying methods, vacuum suction systems offer several distinct advantages. One of the primary benefits is the reduced risk of dust and particle dispersion, which enhances workplace safety and environmental compliance. The enclosed system design prevents dust from escaping into the air, making it suitable for applications where air quality is a concern. Another advantage is the energy efficiency of vacuum suction systems, as they typically require less power to operate compared to high-pressure positive pressure systems. This results in lower operational costs and reduced environmental impact. Furthermore, the system's flexibility allows for easy integration with existing production lines, with minimal modifications required. The ability to transport powders over longer distances without the need for intermediate storage or handling points also streamlines the overall production process, improving operational efficiency.
Conclusion and Company Overview
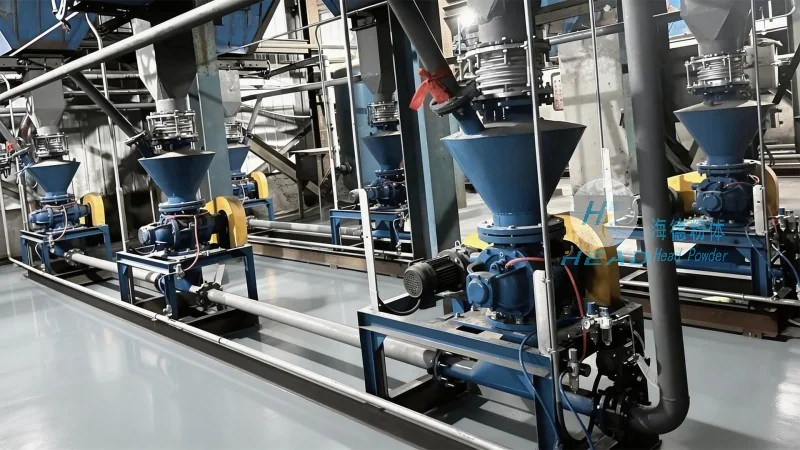
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a trusted provider of vacuum suction type powder conveying systems. With years of experience in the industry, the company has developed advanced solutions tailored to meet the specific needs of various industries. By leveraging the principles of vacuum suction, HeadPowder's systems offer a reliable, efficient, and safe method for powder transport. The company's commitment to quality and innovation ensures that its products meet the highest standards, providing customers with a cost-effective and sustainable solution for their powder handling needs. Whether in chemical, food, or pharmaceutical applications, HeadPowder's vacuum suction systems are designed to enhance productivity while maintaining product integrity and environmental compliance.